

Operation Process and Working Principle of Dilute Phase Powder Conveyors
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of dilute phase powder conveyors. These systems are engineered to efficiently transport bulk materials in a dispersed state, ensuring optimal performance and reliability in various industrial applications.
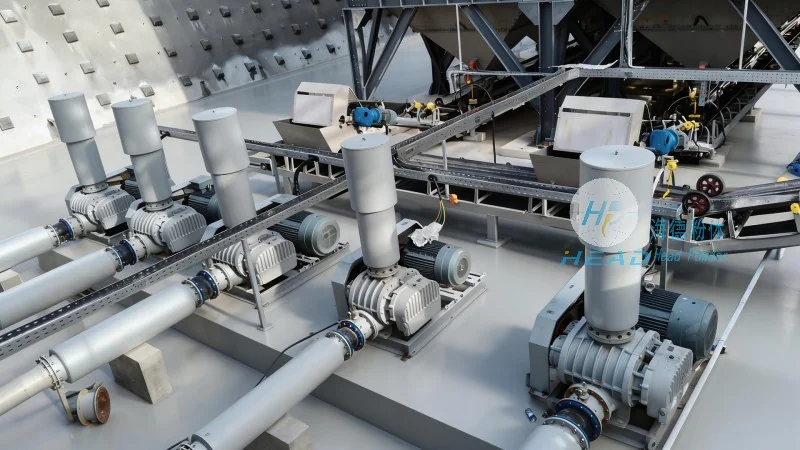
Working Principle of Dilute Phase Conveying Systems
Dilute phase powder conveyors operate by creating a low concentration of material particles suspended in a carrier gas. The process begins with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. A high-velocity air stream, typically generated by a positive displacement blower or a centrifugal fan, propels the material particles through the pipeline. The air velocity is maintained above the material's terminal velocity, ensuring that the particles remain suspended and are transported efficiently. This method allows for the transportation of powders over long distances with minimal pressure drop and reduced risk of material degradation.
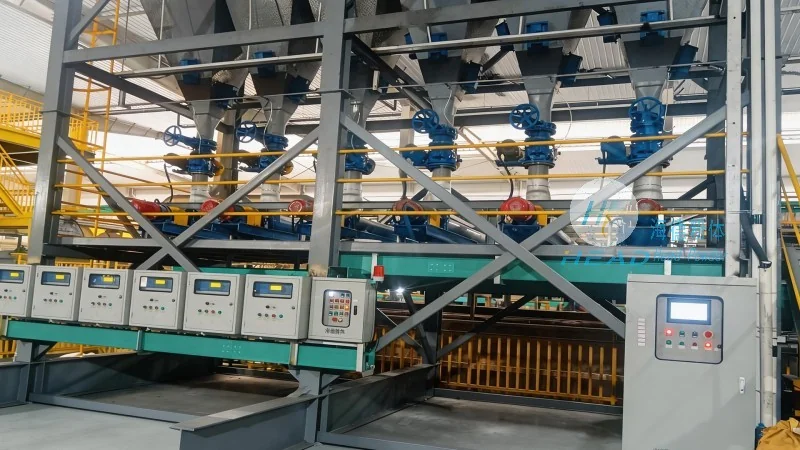
Operation Process of Dilute Phase Powder Conveyors
The operation of a dilute phase powder conveyor involves several key steps. First, the bulk material is loaded into the hopper or storage silo. The feeder then regulates the material flow into the conveying line. The air compressor or fan supplies the necessary air pressure and volume to create the conveying air stream. As the material enters the pipeline, it is mixed with the air and carried forward. The system includes control valves and sensors to monitor pressure, flow rate, and material level, ensuring stable operation. At the discharge end, the material is separated from the air, often using a cyclone separator or a bag filter, and collected in a receiving hopper or container.
Key Components and Their Functions
Several critical components contribute to the effective operation of dilute phase powder conveyors. The hopper or feeder is responsible for storing and feeding the bulk material into the system. The air compressor or fan provides the motive force, generating the high-velocity air stream. The pipeline system, typically made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. The control system, including pressure regulators, flow meters, and sensors, monitors and adjusts the operation to maintain optimal conditions. The separation equipment, such as cyclones or filters, removes the material from the air at the discharge end, preventing dust emissions and ensuring material purity.
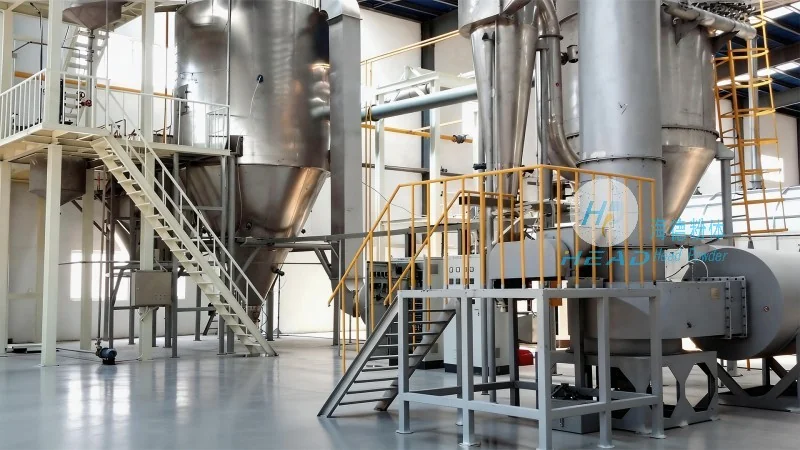
Application Scenarios and Benefits
Dilute phase powder conveyors are widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining. They are particularly suitable for transporting fine powders, granules, and other bulk materials that are prone to caking or agglomeration. The benefits of these systems include high conveying capacity, low energy consumption, minimal material degradation, and the ability to transport materials over long distances. Additionally, the system's design allows for easy integration with existing production lines and facilitates clean and efficient material handling.