

Principle and Working Scene Characteristics of Desulfurization Fly Ash Powder Pneumatic Conveying Eq
Desulfurization fly ash, a byproduct of flue gas desulfurization processes in thermal power plants and industrial facilities, poses significant handling challenges due to its fine particle size and potential environmental hazards. The pneumatic conveying system offers an efficient and reliable solution for transporting this powder, ensuring safe and effective material transfer from source to destination. This article explores the fundamental principles behind such equipment and highlights key working scene characteristics that define its application in industrial settings.
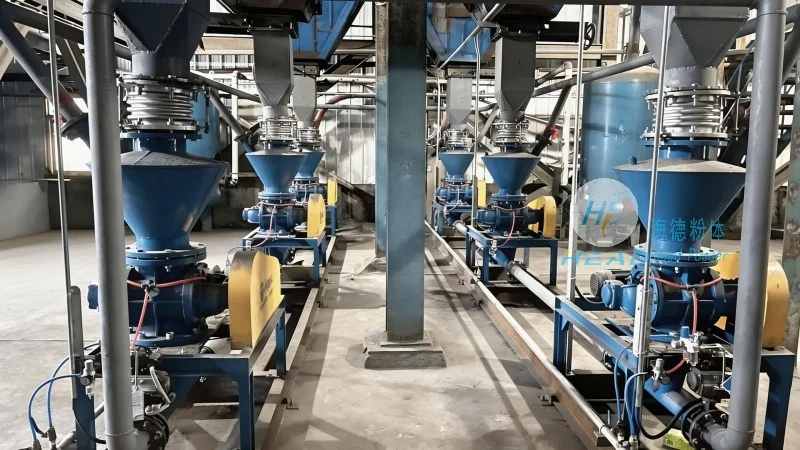
Principle of Pneumatic Conveying for Desulfurization Fly Ash
The core principle of pneumatic conveying involves the use of compressed air or gas to transport particulate materials through a pipeline. In the context of desulfurization fly ash, the system typically operates under positive pressure, where air is forced through a hopper or feeder, lifting the ash particles into the conveying line. The air velocity is carefully controlled to maintain a stable flow, preventing particle segregation and ensuring consistent delivery. Key components include the feed hopper, rotary valve, air compressor, and pipeline system, each playing a critical role in the overall conveying process. The design of the system must account for the ash's properties—such as moisture content, particle size distribution, and density—to optimize performance and minimize operational issues like blockages or material degradation.
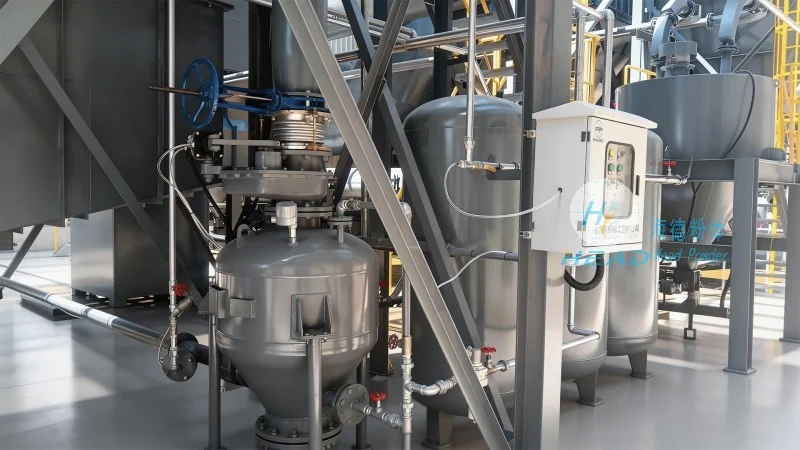
Working Scene Characteristics and Application Environments
The working scene characteristics of desulfurization fly ash pneumatic conveying equipment are tailored to meet the demands of diverse industrial applications. These systems are commonly employed in power plants, cement factories, and waste management facilities where large volumes of fly ash need to be transported over short to medium distances. The equipment is designed to handle high throughput rates, often ranging from several tons per hour to tens of tons per hour, depending on the system configuration. One of the primary advantages is the ability to transport ash in a closed system, reducing dust emissions and improving workplace safety. Additionally, the flexibility of pneumatic conveying allows for integration with existing infrastructure, such as existing pipelines or storage silos, minimizing installation costs and time. The working environment may involve harsh conditions, including high temperatures and corrosive gases, which requires robust materials of construction for the conveying components to ensure long-term reliability.
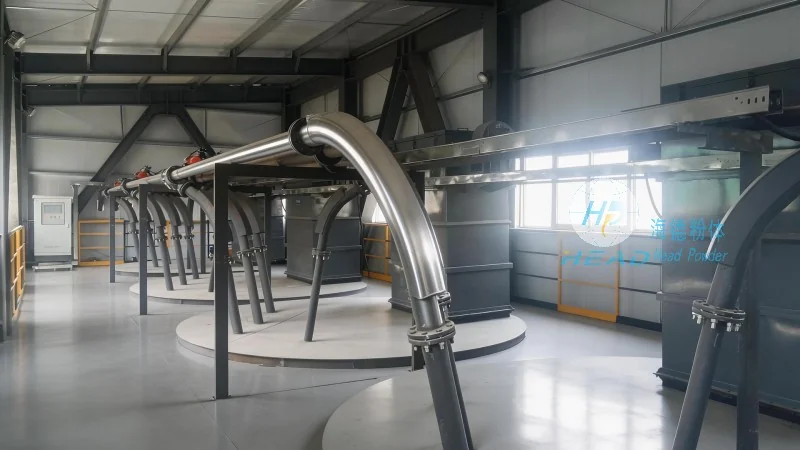
Technical Advantages and Operational Efficiency
HeadPowder, as a leading manufacturer of industrial conveying solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique requirements of desulfurization fly ash. The company's expertise lies in optimizing system performance through precise control of air pressure, flow rates, and particle velocity, ensuring efficient and low-cost material transport. The use of positive pressure systems reduces the risk of material degradation compared to negative pressure systems, which are more prone to clogging and air leakage. Furthermore, the closed-loop design of the equipment minimizes environmental impact by containing dust and preventing contamination of the surrounding air. Operational efficiency is enhanced through features like automatic control systems that adjust air flow based on feed rate, reducing energy consumption and extending equipment lifespan. The modular design of the systems allows for easy maintenance and component replacement, ensuring minimal downtime during routine servicing.
Company Profile and Service Commitment
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable enterprise based in Shandong, China, dedicated to providing high-quality industrial conveying equipment. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the power and cement industries. With a focus on research and development, HeadPowder continuously improves its product line to meet evolving industry standards and client needs. The company's facilities in Shandong are equipped with advanced manufacturing capabilities, enabling the production of customized pneumatic conveying systems that adhere to international quality and safety regulations. HeadPowder's team of experienced engineers and technicians provides comprehensive support, from system design and installation to ongoing maintenance and technical assistance. This dedication to service ensures that clients receive not only reliable equipment but also long-term solutions that enhance operational efficiency and reduce costs.