

Principles and Working Scenarios of Intelligent Bulk Bag Unloading Pneumatic Powder Conveying Equipm
Intelligent bulk bag unloading pneumatic powder conveying equipment represents a significant advancement in material handling technology, particularly for industries dealing with bulk powders. This equipment is designed to efficiently and safely transfer powders from bulk bags into processing systems, storage tanks, or other containers. The integration of intelligent features enhances operational efficiency, reduces labor costs, and improves overall process reliability. In this article, we will explore the fundamental principles behind this equipment, its key working scenarios, and the specific advantages it offers to various industrial applications.
Core Principles of Pneumatic Powder Conveying
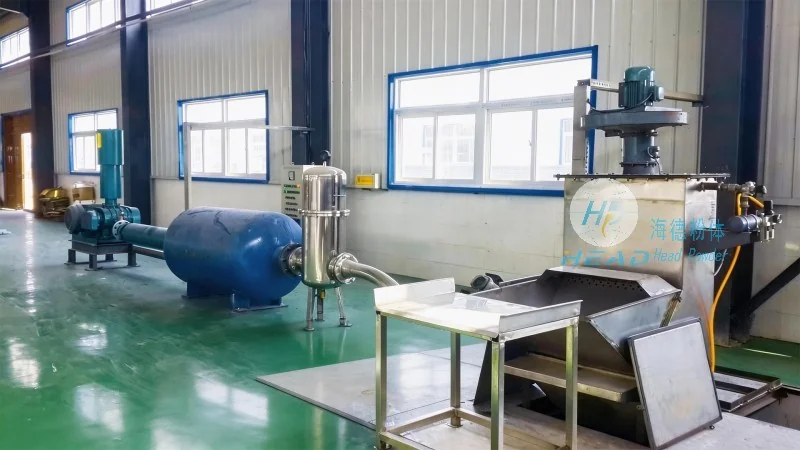
The operation of intelligent bulk bag unloading pneumatic powder conveying equipment is based on the principles of pneumatic conveying, which utilizes air to transport bulk materials. The system typically consists of a bulk bag unloader, a pneumatic conveying line, and a receiving hopper or tank. The process begins with the bulk bag being placed on the unloader frame. The bag is then opened, and the powder is discharged into a hopper equipped with a rotary valve or other feeding mechanism. Compressed air is introduced into the conveying line, creating a flow that draws the powder from the hopper and transports it to the destination. The intelligent features may include automated bag opening, level sensing, and real-time monitoring of the conveying process, ensuring precise control and minimal material loss.
Key Working Scenarios and Applications
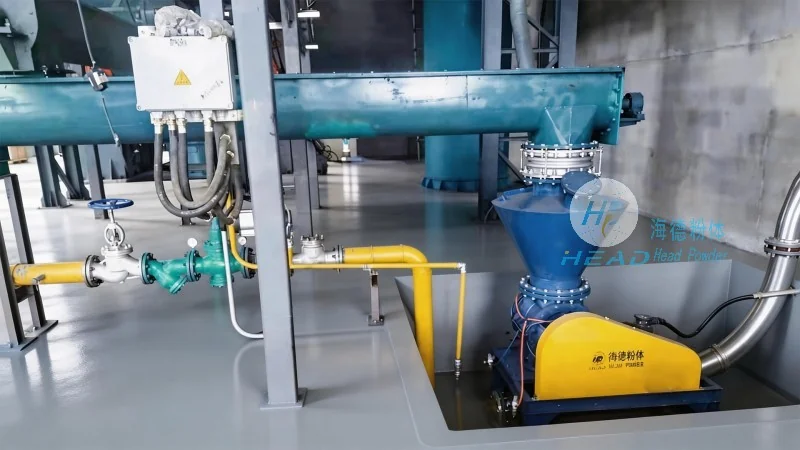
Intelligent bulk bag unloading pneumatic powder conveying equipment is widely used across various industries due to its versatility and efficiency. Some of the primary working scenarios include:
- Pharmaceutical Industry: In pharmaceutical manufacturing, the equipment is used to handle raw materials such as active pharmaceutical ingredients (APIs), excipients, and other fine powders. The intelligent system ensures that the powders are transferred under sterile and controlled conditions, minimizing contamination risks. The equipment's ability to handle small batches and precise dosing is crucial for pharmaceutical production lines.
- Food and Beverage Industry: For food processing, the equipment is employed to convey ingredients like flour, sugar, spices, and other food-grade powders. The intelligent features help maintain hygiene standards, as the system can be designed with stainless steel components and easy-to-clean features. The equipment's efficiency in handling large bulk bags reduces downtime and improves production throughput.
- Chemical Industry: In chemical processing, the equipment is used to transport various chemical powders, including catalysts, pigments, and other industrial chemicals. The intelligent system provides precise control over the conveying rate, ensuring that the chemical process parameters are maintained. The equipment's robust design allows it to handle abrasive and corrosive materials, making it suitable for demanding chemical applications.
- Mineral and Mining Industry: For mineral processing, the equipment is used to transfer raw ores, minerals, and other bulk materials from bulk bags to processing equipment. The intelligent features help optimize the conveying process, reducing energy consumption and improving material recovery rates. The equipment's ability to handle large volumes and different particle sizes makes it ideal for mining operations.
Advantages of Intelligent Bulk Bag Unloading Pneumatic Powder Conveying Equipment
Implementing intelligent bulk bag unloading pneumatic powder conveying equipment offers several key advantages over traditional methods. These include:
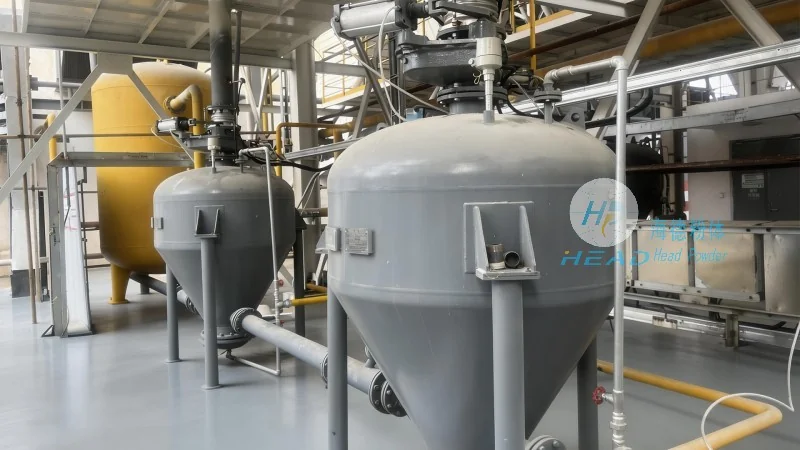
- Enhanced Efficiency and Productivity: The automated operation reduces labor requirements and minimizes downtime, leading to increased production efficiency. The intelligent control systems allow for precise control of the conveying rate, ensuring optimal material flow and reducing waste.
- Improved Safety and Hygiene: The equipment is designed with safety features such as automatic bag opening and closing, preventing accidental exposure to powders. The stainless steel construction and easy-to-clean design maintain high hygiene standards, which is critical in industries like pharmaceuticals and food processing.
- Reduced Material Loss and Contamination: The intelligent system minimizes material loss during transfer, as it can detect and adjust for variations in bag density and material flow. The enclosed design prevents dust and contamination, ensuring that the transferred powders remain clean and free from foreign particles.
- Cost Savings: By reducing labor costs and minimizing material waste, the equipment provides significant cost savings over time. The energy-efficient design also contributes to lower operational costs, making it a cost-effective solution for bulk powder handling.
Conclusion
Intelligent bulk bag unloading pneumatic powder conveying equipment is a vital component in modern industrial operations, offering a reliable and efficient solution for handling bulk powders. The integration of intelligent features enhances the overall performance of the system, making it suitable for a wide range of applications across various industries. As industries continue to demand higher efficiency and safety standards, this equipment will play an increasingly important role in material handling processes. For companies looking to optimize their bulk powder handling operations, investing in such intelligent equipment can lead to significant improvements in productivity, safety, and cost-effectiveness.