

Principle and Working Scene Characteristics of White Gray Material Handling Equipment
White gray material handling equipment serves as a critical component in industrial production for transporting bulk powders like white and gray materials. This equipment is designed to ensure efficient material flow, enhance operational efficiency, and maintain safety standards in various industrial settings. The following article explores the working principles, key components, and working scene characteristics of such equipment, providing valuable insights for professionals in the material handling industry.
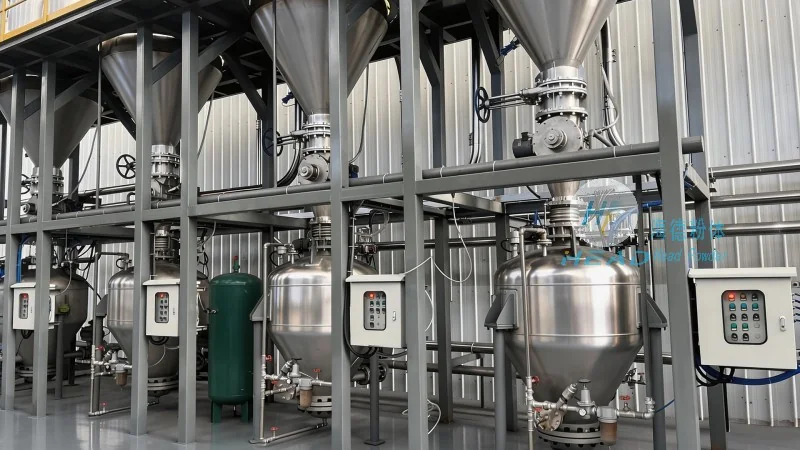
Working Principle of White Gray Material Handling Equipment
The fundamental working principle of white gray material handling equipment centers on the effective transport of powders. These systems may employ different mechanisms based on the material properties and operational requirements. For instance, pneumatic conveying systems utilize air pressure to move materials through pipelines, while screw conveyors rely on rotating screws to push materials forward. Bucket elevators, another common type, use buckets attached to a chain or belt to lift materials vertically. The choice of mechanism is influenced by factors like material particle size, moisture content, and the required transport distance. The equipment is engineered to handle materials with varying flow characteristics, ensuring stable and reliable operation under diverse industrial conditions.
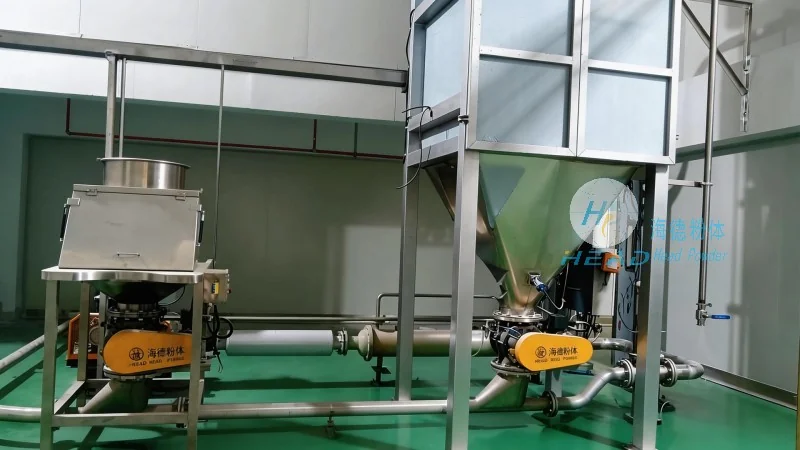
Key Components and Their Functions
White gray material handling equipment comprises several essential components that work together to achieve efficient material transport. The primary components include the material inlet, conveyor mechanism, control system, and discharge outlet. The material inlet is designed to safely introduce the white or gray powder into the system, often equipped with sealing mechanisms to prevent dust leakage and maintain environmental compliance. The conveyor mechanism, whether pneumatic or mechanical, is responsible for moving the material from the inlet to the discharge point. The control system monitors and regulates the operation, ensuring optimal performance and preventing issues like blockages or overloading. The discharge outlet allows the material to be released at the desired location, with adjustable discharge angles to accommodate different application needs. Each component is constructed with durability in mind, using materials resistant to abrasion and corrosion from the white and gray powders, thereby extending the equipment's service life.
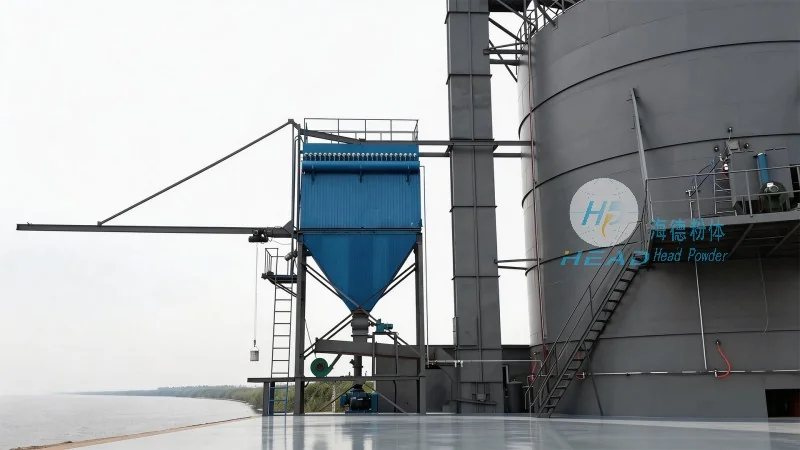
Working Scene Characteristics and Application Scenarios
The working scene characteristics of white gray material handling equipment are closely tied to the industrial environments where they are deployed. These systems are commonly found in sectors such as cement production, chemical processing, and mining, where large volumes of white or gray powders need to be transported between different stages of production. For example, in cement plants, the equipment is used to move raw materials like limestone and clay from storage silos to the grinding mills. In chemical factories, it handles powders like calcium carbonate or gypsum for various production processes. The working scene characteristics include high material throughput, continuous operation, and the need for dust control measures to comply with environmental regulations. The equipment is also adapted to different spatial configurations, including horizontal and vertical transport, to suit the layout of industrial facilities. Its ability to handle materials with varying flow properties makes it versatile for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
Advantages in Industrial Production
White gray material handling equipment offers several advantages that contribute to improved industrial productivity and operational efficiency. One key advantage is its ability to transport materials in a closed system, which reduces dust pollution and enhances workplace safety. This is particularly important in industries where airborne dust can pose health risks or affect product quality. Additionally, the equipment is designed for high efficiency, with minimal energy consumption and low maintenance requirements, leading to cost savings over time. The reliability of the system ensures consistent material flow, reducing downtime and improving overall production output. Furthermore, the equipment's adaptability allows it to handle a variety of materials, making it a versatile solution for different industrial needs. Its robust construction and durability enable it to operate in harsh conditions, such as high temperatures or corrosive environments, without compromising performance.
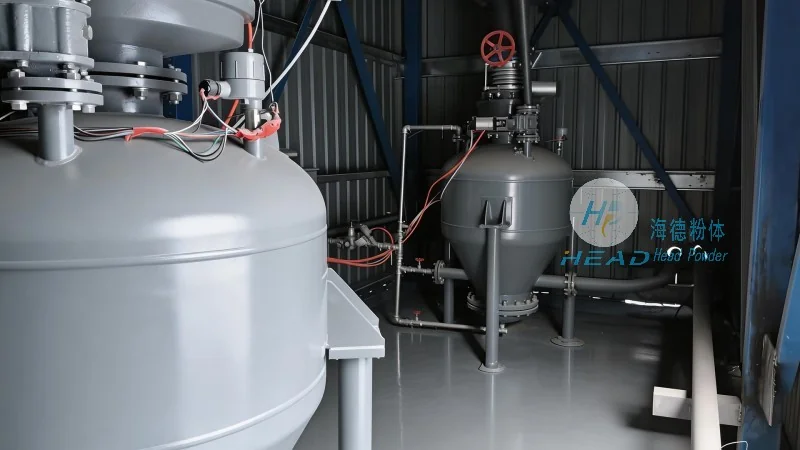
Company Information
HeadPowder, a leading manufacturer of white gray material handling equipment, is dedicated to providing high-quality solutions for industrial material transport. With years of experience in the field, the company has developed advanced equipment that meets the demands of modern industrial production. Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and manufacturing customized material handling systems tailored to specific customer requirements. The company's commitment to innovation and quality ensures that its products are reliable, efficient, and durable, helping clients achieve optimal performance in their operations. HeadPowder's expertise in material handling technology positions it as a trusted partner for industries seeking efficient and safe material transport solutions.