

Principle and Working Scene Characteristics of Fly Ash Silo Material Conveying Equipment
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling solutions. This article focuses on the fly ash silo material conveying equipment, exploring its operational principles and typical working scenarios to provide a comprehensive understanding of this critical component in industrial applications.
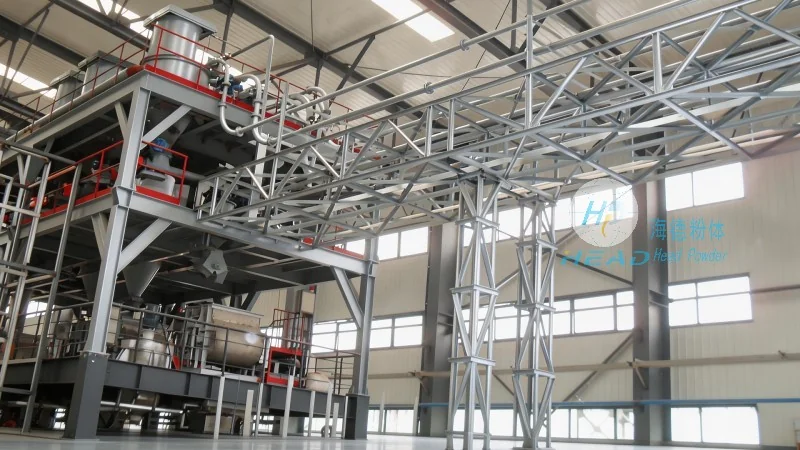
Principle of Operation
The fly ash silo material conveying equipment is engineered to efficiently transport fly ash from storage silos to processing or disposal units. It typically operates on the principle of mechanical conveying, utilizing components such as screw conveyors, belt conveyors, or pneumatic systems to move the material. The system is designed to handle the bulk density and flow characteristics of fly ash, ensuring consistent and reliable material transfer. Key components include the hopper, conveyor mechanism, control system, and safety features. The equipment is built to withstand the abrasive nature of fly ash, with materials like stainless steel or corrosion-resistant alloys used in critical parts to extend service life and maintain performance.
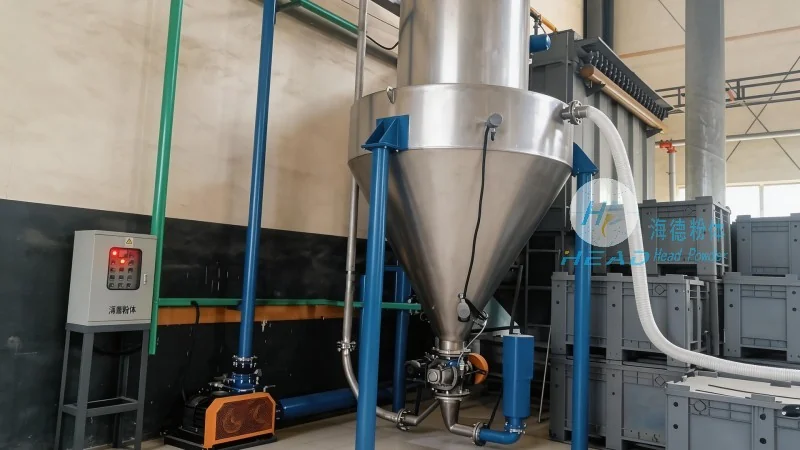
Working Scene Characteristics
The fly ash silo material conveying equipment is commonly employed in power plants, cement factories, and waste management facilities where large volumes of fly ash need to be handled. In power plants, it facilitates the transfer of fly ash from the boiler's bottom ash hopper to the silo for storage or further treatment. The equipment is designed to operate in environments with varying temperatures and humidity levels, ensuring stable performance under different operational conditions. The working scene often involves high-throughput requirements, as power plants generate significant amounts of fly ash daily. The equipment's design allows for integration with existing infrastructure, minimizing installation time and costs. Additionally, the system is equipped with monitoring and control features to optimize material flow and prevent blockages, enhancing overall operational efficiency.
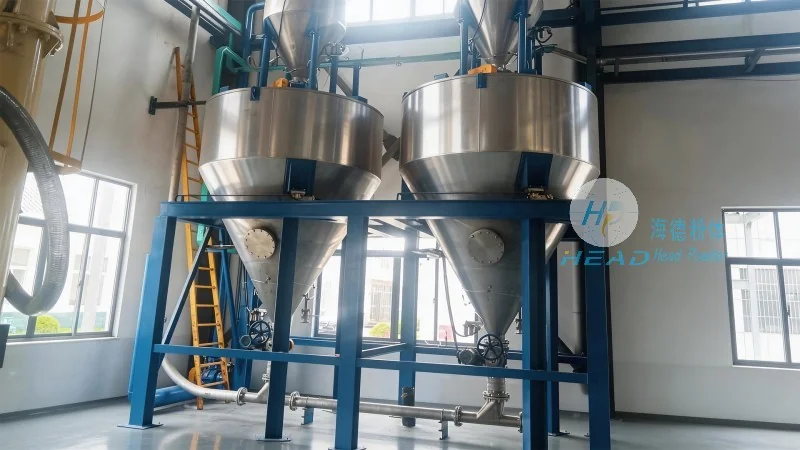
Key Features and Advantages
HeadPowder's fly ash silo material conveying equipment offers several advantages that make it suitable for demanding industrial applications. The equipment is designed for high reliability, with robust construction and minimal maintenance requirements. The use of advanced control systems enables precise regulation of material flow, reducing waste and improving process efficiency. The equipment is also scalable, allowing it to be customized to meet the specific needs of different facilities, whether for small-scale or large-scale operations. Safety features, such as overload protection and emergency stop mechanisms, are integrated to ensure operator safety and prevent equipment damage. The equipment's low energy consumption and environmental friendliness make it an attractive solution for facilities aiming to reduce operational costs and environmental impact.