

Principle and Working Scene Characteristics of Powder Bin Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. This article explores the fundamental principles and practical working scene characteristics of powder bin pneumatic conveying systems, which are widely used in various industrial sectors for efficient material transport.
The Core Principle of Powder Bin Pneumatic Conveying
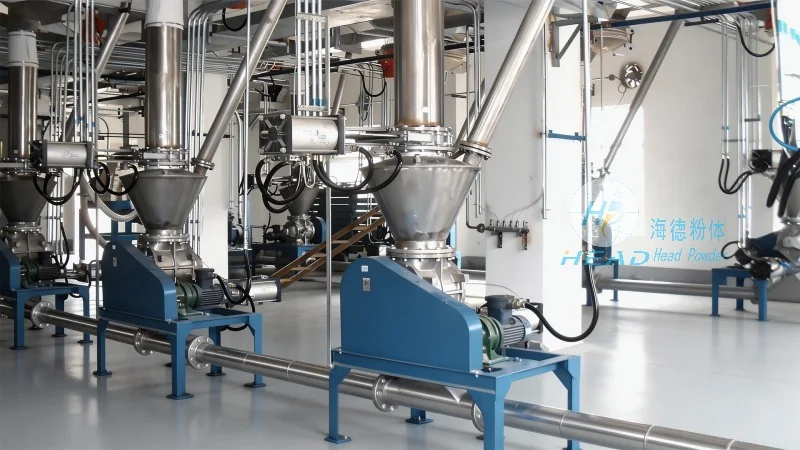
Powder bin pneumatic conveying systems operate on the principle of air-assisted material transport. The system typically consists of a storage bin, a conveying line, and a control system. When the system is activated, compressed air is introduced into the bin, creating a pressure differential that propels the powder particles through the pipeline. This method is known as positive pressure conveying, where air and powder move together in the same direction. The process involves several key steps: first, the powder is drawn from the bin into the conveying line by the air flow; second, the mixture travels through the pipeline to the destination point; third, the powder is separated from the air at the receiving end, often using a cyclone separator or a bag filter. This principle allows for the safe and efficient transfer of bulk powders over relatively long distances without the need for mechanical components like belts or screws, which can be prone to wear and contamination.
Key Components and Their Functions
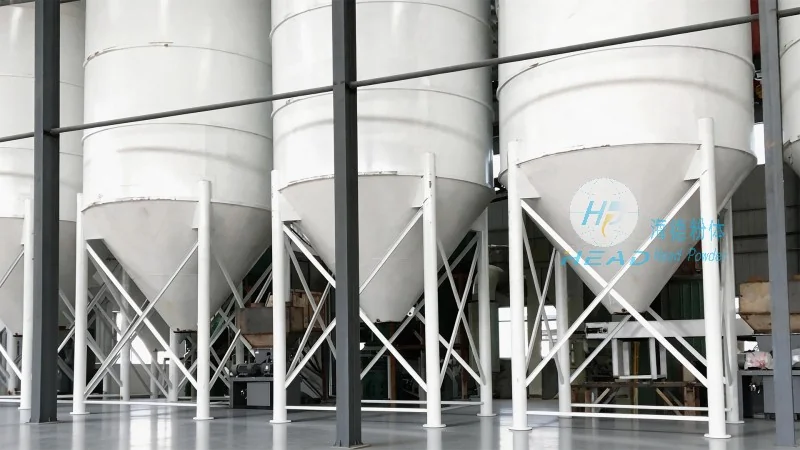
The effectiveness of a powder bin pneumatic conveying system depends on the proper functioning of its main components. The storage bin, or powder hopper, is designed to hold the bulk material and maintain a consistent feed rate. It often includes a discharge valve at the bottom to control the flow of powder into the conveying line. The conveying line is usually made of stainless steel or other corrosion-resistant materials to handle different types of powders, such as chemicals, food ingredients, or pharmaceuticals. The line diameter and length are critical factors that affect the system's performance, as they determine the pressure drop and the required air volume. The control system, which may include pressure regulators, flow meters, and solenoid valves, ensures that the air pressure and flow rate are maintained at optimal levels. Additionally, a dust collection system, such as a cyclone separator or a baghouse filter, is essential to capture any powder particles that may escape during the conveying process, ensuring environmental compliance and product purity.
Working Scene Characteristics and Application Scenarios
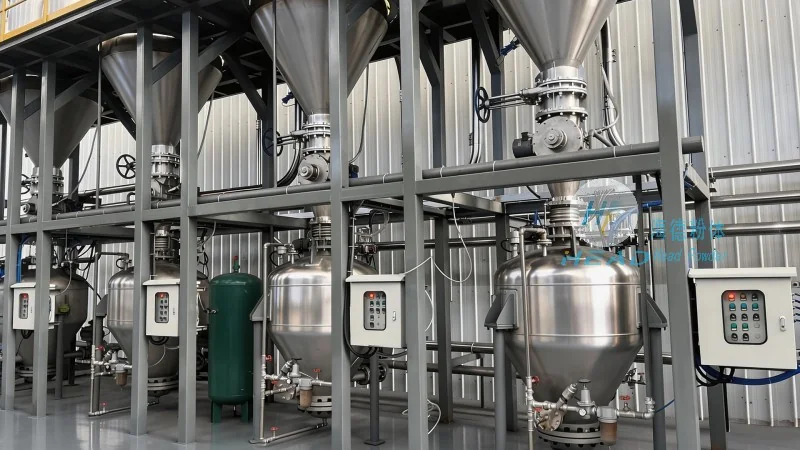
Powder bin pneumatic conveying systems are particularly well-suited for applications where bulk powders need to be transported from a central storage location to multiple processing points. In industrial settings, these systems are commonly used in chemical manufacturing, where powders like pigments, polymers, and additives are moved between reactors and storage tanks. In the food and beverage industry, they are employed to transfer ingredients such as flour, sugar, and spices from silos to production lines, ensuring hygienic and efficient handling. The pharmaceutical industry also relies on these systems for the transport of active pharmaceutical ingredients (APIs) and excipients, as the enclosed design prevents contamination and cross-contamination. Another key application is in the mining and mineral processing sector, where bulk minerals are conveyed from storage bins to processing equipment. The working scene characteristics of these systems include high throughput, low maintenance requirements, and the ability to handle a wide range of powder properties, including varying particle sizes, densities, and moisture contents. The systems are also adaptable to different operating conditions, such as temperature and humidity variations, making them suitable for both indoor and outdoor installations.
Technical Advantages in Practical Applications
Compared to traditional mechanical conveying methods, powder bin pneumatic conveying systems offer several technical advantages that enhance operational efficiency and product quality. One of the primary benefits is the reduction in material handling time and labor costs. The enclosed design of the system minimizes dust exposure, which not only improves workplace safety but also maintains the integrity of the powder by preventing agglomeration or degradation. The system's ability to handle fine powders without clogging is another significant advantage, as the air flow helps to keep the particles in suspension, reducing the risk of blockages in the pipeline. Additionally, the system's flexibility allows for easy integration with existing production lines, enabling seamless material transfer without disrupting the overall workflow. The low maintenance requirements of the components, such as the absence of moving parts in the conveying line, contribute to long-term cost savings and increased system reliability. Furthermore, the system's scalability allows manufacturers to adjust the capacity based on production needs, making it suitable for both small-scale and large-scale operations.
Company Profile and Professional Support
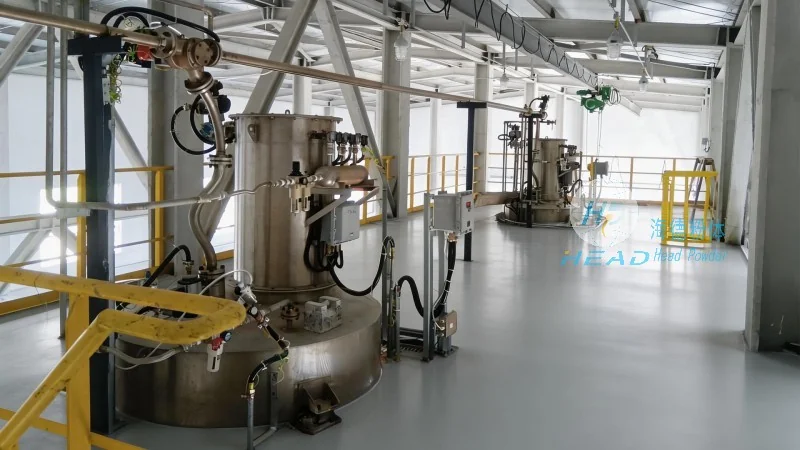
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company dedicated to providing high-quality powder handling solutions. With years of experience in the industry, HeadPowder has developed a comprehensive range of powder bin pneumatic conveying systems tailored to meet the diverse needs of various industries. The company's team of engineers and technicians is committed to delivering innovative and reliable equipment that meets international standards for safety and performance. HeadPowder offers comprehensive technical support, including system design, installation, and maintenance services, ensuring that clients receive the best possible solution for their specific requirements. The company's commitment to quality and customer satisfaction has earned it a strong reputation in the market, making it a trusted partner for businesses seeking efficient and effective powder handling solutions.