

Principle and Working Scene Features of Electrode Carbon Black Purification Ash Powder Conveying Equ
Electrode carbon black purification ash powder conveying equipment is a specialized system designed for the efficient handling and transportation of ash powders generated during the purification process of electrode carbon black. This equipment plays a crucial role in industrial settings where the management of fine particulate materials is essential for maintaining operational efficiency and environmental compliance. The system integrates advanced engineering principles to ensure reliable performance under various operational conditions.
Working Principle of the Conveying Equipment
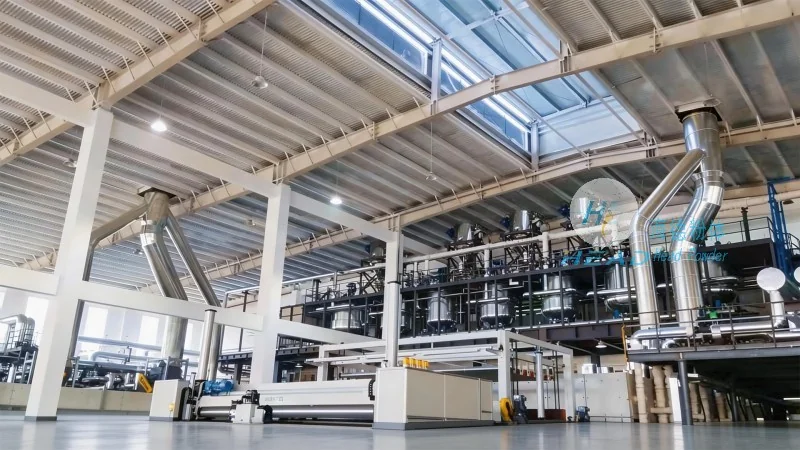
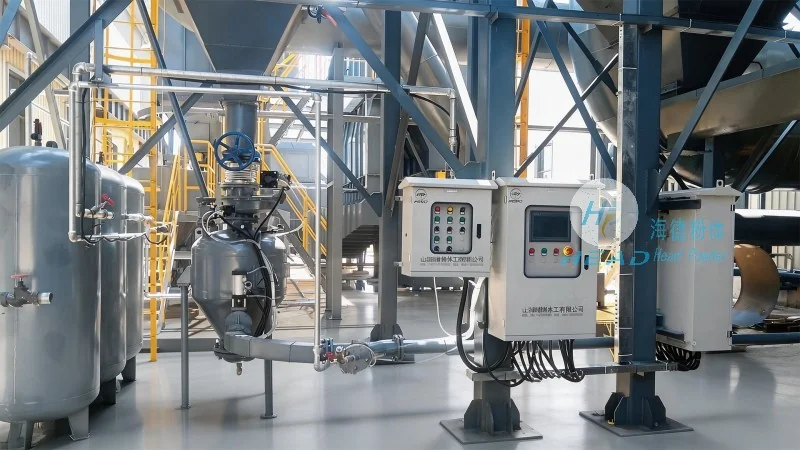
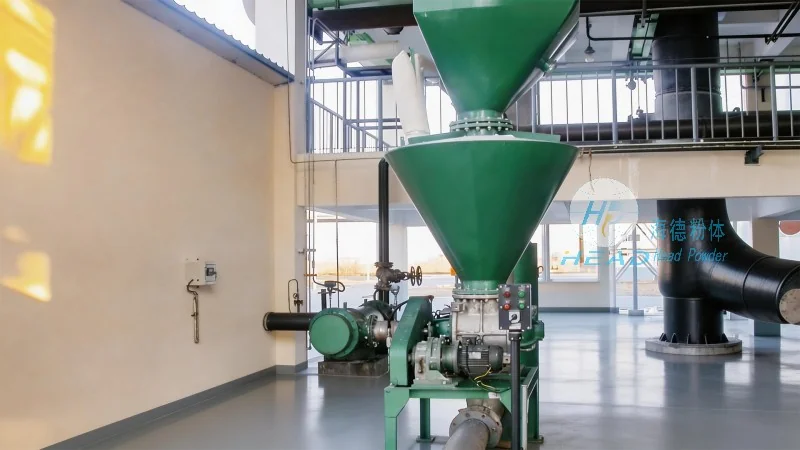
The core of the conveying equipment lies in its ability to transport fine ash powders from the source to the designated disposal or processing location. Typically, such systems employ a combination of mechanical and pneumatic components to achieve seamless material transfer. The process begins with the collection of ash powders, which are then fed into a hopper or storage tank. From there, the material is transferred through a series of pipes or conveyor belts, depending on the specific design. For pneumatic conveying systems, compressed air is used to create a flow that propels the powder through the pipeline. Mechanical conveyors, on the other hand, utilize rotating blades or screws to move the material. The selection of the conveying method depends on factors such as the particle size, moisture content, and the distance to be covered. The equipment is engineered to handle the unique characteristics of electrode carbon black ash, which often includes high temperature sensitivity and potential reactivity during transport. Advanced control systems are integrated to regulate the flow rate, pressure, and speed, ensuring consistent and safe operation. This ensures that the ash powders are conveyed without clogging or degradation, maintaining the integrity of the material throughout the process.
Key Features and Technical Advantages
Headpowder's conveying equipment for electrode carbon black purification ash powders is designed with several key features that enhance its performance and reliability. One of the primary advantages is its high efficiency in material handling, which minimizes downtime and maximizes production output. The system is built with durable materials that can withstand the abrasive nature of ash powders, reducing maintenance requirements and extending the equipment's service life. Additionally, the equipment incorporates advanced filtration and cleaning mechanisms to prevent dust emissions and maintain air quality in the working environment. This not only improves safety for operators but also complies with environmental regulations. The modular design of the equipment allows for easy installation and integration into existing industrial setups, making it a flexible solution for various applications. Furthermore, the control system is user-friendly, enabling operators to monitor and adjust the conveying parameters in real-time, ensuring optimal performance under different load conditions.
Working Scene Characteristics and Application Scenarios
The working scene characteristics of electrode carbon black purification ash powder conveying equipment are tailored to meet the demands of specific industrial environments. These systems are commonly used in the production facilities of electrode carbon black manufacturers, where the ash generated during the purification process needs to be transported to storage or disposal sites. The equipment is designed to operate in environments with varying temperatures and humidity levels, making it suitable for both indoor and outdoor applications. The compact design of the conveying system allows for installation in confined spaces, which is often required in industrial plants with limited floor space. The equipment's ability to handle high volumes of ash powders makes it ideal for large-scale production lines, where consistent material flow is critical for maintaining production rates. Additionally, the system's low maintenance requirements and energy efficiency contribute to cost savings for industrial operators. The working scene also includes scenarios where the ash powders need to be transferred to other processing units for further treatment or recycling. In such cases, the conveying equipment ensures that the material is transported without contamination or loss, supporting the overall sustainability goals of the industrial operation.
Conclusion and Company Information
Electrode carbon black purification ash powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a reliable and efficient solution for managing fine particulate materials in industrial settings. The equipment's advanced design and robust construction ensure consistent performance, while its modular and user-friendly features make it adaptable to various operational needs. By integrating state-of-the-art technology, Headpowder's conveying systems help industrial clients maintain operational efficiency, reduce costs, and comply with environmental standards. With a strong presence in China, particularly in Shandong, HeadPowder Engineering Co., Ltd. continues to provide high-quality equipment tailored to the specific requirements of the electrode carbon black industry. The company's commitment to innovation and customer satisfaction ensures that its conveying equipment remains a leading solution for ash powder transportation in the market.