

Principle and Working Scene Characteristics of Rice Husk Ash Powder Conveying Equipment
Rice husk ash, a byproduct of biomass combustion processes, is often handled as a fine powder that requires efficient and reliable transportation systems. The rice husk ash powder conveying equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these challenges through advanced engineering solutions tailored to the unique properties of this material. This equipment is designed to ensure safe, clean, and efficient movement of rice husk ash powder from production sites to processing or storage facilities, playing a crucial role in the overall workflow of biomass energy and environmental management operations.
Principle of Operation for Rice Husk Ash Powder Conveying Equipment
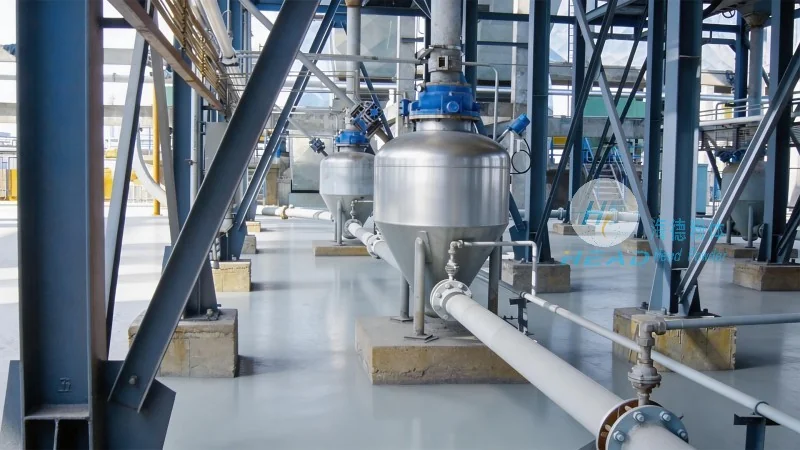
The core principle of rice husk ash powder conveying equipment revolves around the utilization of pneumatic or mechanical conveying technologies. For pneumatic systems, the equipment typically operates by creating a pressure differential within a closed pipeline system. A fan or blower generates airflow that draws the rice husk ash powder into the inlet, where it is mixed with air to form a slurry-like mixture. This mixture is then propelled through the pipeline to the destination point, where a separator or cyclone separates the powder from the air, allowing the powder to be deposited in a collection bin or processing unit. The air is then filtered and returned to the system, ensuring minimal dust emissions and environmental compliance. Mechanical conveying systems, such as screw conveyors or belt conveyors, may also be employed for shorter distances or when the material is less abrasive, though pneumatic systems are more common for fine powders like rice husk ash due to their ability to handle high volumes and long distances with minimal maintenance.
Key Components and Their Functions in the Conveying System
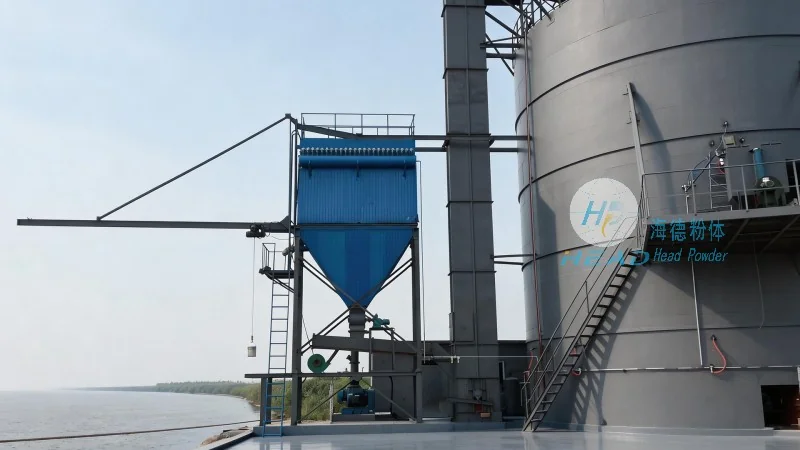
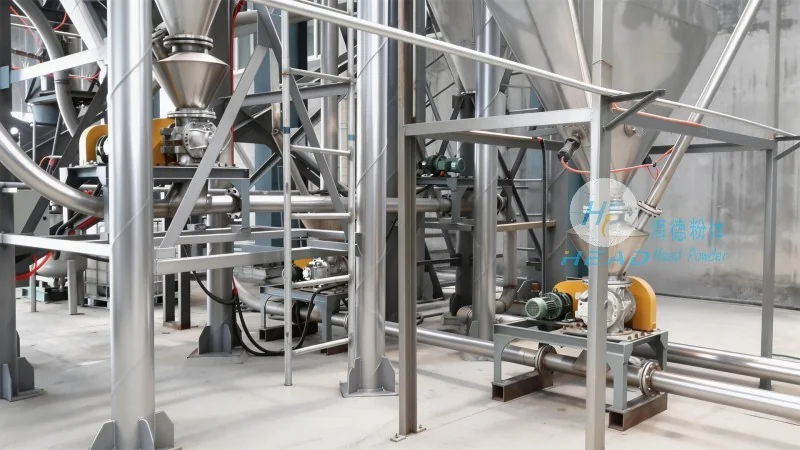
The rice husk ash powder conveying equipment consists of several critical components, each playing a vital role in the overall operation. The primary components include the feed hopper, which serves as the entry point for the rice husk ash powder, ensuring a consistent and controlled feed rate. The feed hopper is equipped with a valve or gate mechanism to regulate the flow of material into the conveying system. The blower or fan unit provides the necessary airflow to move the powder through the pipeline, with adjustable speed settings to accommodate varying material volumes and pipeline lengths. The conveying pipeline itself is typically made of corrosion-resistant materials, such as stainless steel or PVC, to withstand the abrasive nature of the rice husk ash powder and prevent material buildup or clogging. The separator or cyclone is a critical component that separates the powder from the air, ensuring that the powder is deposited accurately and that the air is cleaned before being recirculated. Additionally, the system may include a dust collection system, such as a baghouse or electrostatic precipitator, to capture any fine particles that escape the separator and prevent air pollution. The control panel, equipped with sensors and monitoring devices, allows operators to adjust the system parameters in real-time, ensuring optimal performance and preventing equipment damage.
Working Scene Characteristics and Application Scenarios
The rice husk ash powder conveying equipment is designed to operate in diverse industrial and environmental settings, each with unique requirements and challenges. In biomass power plants, the equipment is used to transport rice husk ash from the combustion chamber to the ash handling and disposal facilities, ensuring that the ash is collected efficiently and without contamination. The long-distance conveying capabilities of the system make it ideal for power plants with multiple ash storage areas or for transporting ash to off-site disposal sites. In environmental remediation projects, the equipment is used to move rice husk ash from treatment facilities to landfills or recycling centers, where it can be used as a soil amendment or for other industrial applications. The equipment's ability to handle fine powders without clogging or degradation makes it suitable for these applications, where the material's properties are critical to the success of the project. In industrial manufacturing facilities, the equipment may be used to transport rice husk ash from processing units to packaging or storage areas, ensuring that the material is handled safely and in compliance with environmental regulations. The equipment's compact design and low maintenance requirements make it suitable for use in tight spaces or in facilities with limited operational space. Additionally, the system's ability to operate continuously for extended periods without significant downtime makes it ideal for high-volume production environments, such as biomass processing plants or large-scale agricultural operations.
Advantages of Using Rice Husk Ash Powder Conveying Equipment from Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. offers a range of rice husk ash powder conveying equipment that is designed to meet the specific needs of its clients. The company's equipment is known for its high efficiency, reliability, and durability, making it a preferred choice for industries that require consistent and safe handling of fine powders. The equipment is manufactured using high-quality materials and advanced engineering techniques, ensuring that it can withstand the harsh conditions of the rice husk ash processing environment. The company provides customized solutions, allowing clients to select the appropriate conveying system based on their specific application requirements, such as pipeline length, material volume, and environmental constraints. The equipment is also designed with safety features, such as dust suppression systems and emergency stop mechanisms, to protect operators and the environment from potential hazards. Additionally, the company offers comprehensive after-sales support, including maintenance services, spare parts availability, and technical assistance, ensuring that clients can rely on their equipment for long-term operation. The use of rice husk ash powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. not only improves the efficiency of the rice husk ash handling process but also contributes to environmental sustainability by reducing the amount of waste material that is disposed of in landfills and by promoting the use of biomass as a renewable energy source.
Conclusion: The Importance of Efficient Rice Husk Ash Powder Conveying Equipment
In conclusion, the rice husk ash powder conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. is a critical component in the processing and management of rice husk ash, a valuable byproduct of biomass energy production. The equipment's advanced design and reliable operation ensure that rice husk ash is handled safely and efficiently, reducing the risk of dust emissions and environmental contamination. The system's ability to handle fine powders over long distances makes it suitable for a wide range of applications, from biomass power plants to environmental remediation projects. The equipment's durability and low maintenance requirements make it a cost-effective solution for industries that require continuous operation. By investing in high-quality rice husk ash powder conveying equipment, companies can improve their operational efficiency, reduce costs, and contribute to a more sustainable future. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and reliable equipment solutions that meet the evolving needs of the biomass and environmental industries.