

Working Principle and Features of Tonne Bag Material Conveying System Equipment
HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, production, and supply of tonne bag material conveying systems. The company is located in Shandong, China, and has been committed to providing high-quality industrial solutions for material handling and transportation in various industries. This article will introduce the working principle and key features of the tonne bag material conveying system equipment produced by HeadPowder.
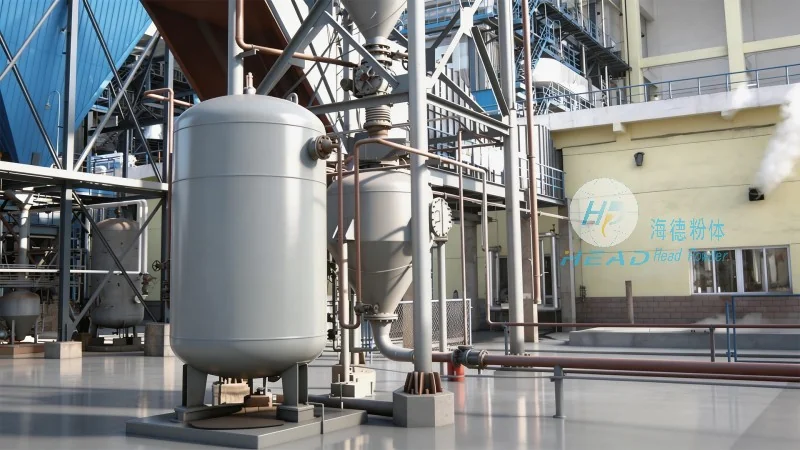
Overview of Tonne Bag Material Conveying System
The tonne bag material conveying system is an essential equipment used in bulk material handling processes. It is designed to efficiently transport materials from the storage area to the processing or packaging area. The system typically consists of components such as feeding mechanisms, conveying belts, lifting devices, and control systems. These components work together to ensure smooth and continuous material flow, reducing manual labor and improving operational efficiency.
Working Principle of Tonne Bag Material Conveying System
The working principle of the tonne bag material conveying system is based on the mechanical transmission of force and motion. The process starts with the material being loaded into the feeding hopper. The feeding mechanism then evenly distributes the material onto the conveyor belt. The conveyor belt, driven by a motor, moves the material forward through the system. The lifting device, such as a vertical conveyor or elevator, may be used to elevate the material to a higher level for further processing. The control system monitors the entire operation, ensuring that the conveying speed, material flow rate, and safety parameters are maintained within optimal ranges. This integrated approach allows for a seamless and automated material handling process from the initial loading to the final discharge point.
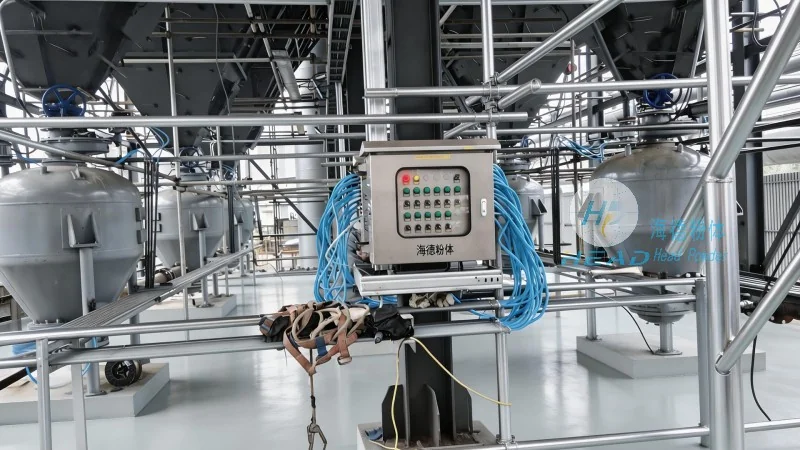
Key Features of Tonne Bag Material Conveying System
The tonne bag material conveying system from HeadPowder Engineering Co., Ltd. offers several notable features that enhance its performance and usability. Firstly, the system is designed for high capacity and durability, capable of handling large volumes of bulk materials with minimal maintenance. The robust construction ensures long-term reliability in demanding industrial environments. Secondly, the system features adjustable conveying speeds and flow rates, allowing for flexible operation to meet different production requirements. This adaptability is crucial for industries with varying material throughput needs. Thirdly, the equipment incorporates advanced safety features, including overload protection, emergency stop buttons, and automatic shut-off mechanisms. These safety measures ensure the protection of operators and the prevention of equipment damage during operation. Additionally, the system is equipped with easy-to-clean components and modular design, facilitating maintenance and cleaning processes. The modular design also enables customization to fit specific plant layouts and material handling needs. Finally, the control system is user-friendly, with intuitive interfaces that allow operators to monitor and control the system efficiently. This ease of operation reduces training time and enhances overall productivity.
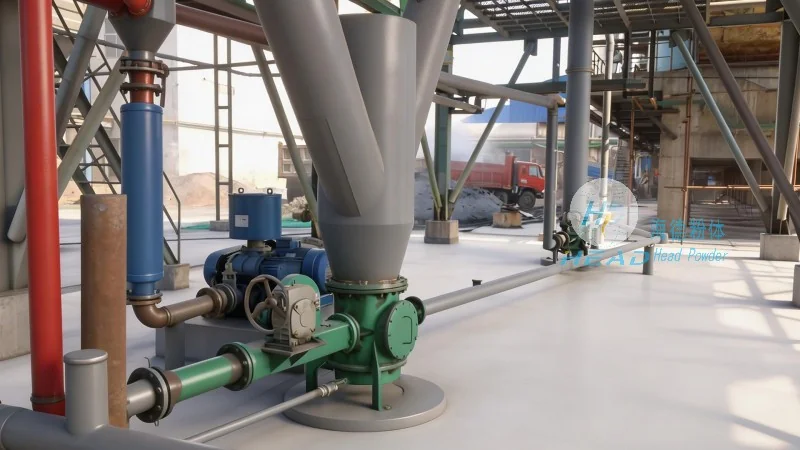
Applications and Benefits
The tonne bag material conveying system is widely used in various industries, including mining, construction, agriculture, and chemical processing. It is particularly suitable for transporting materials such as sand, gravel, cement, coal, and other bulk solids. The primary benefits of using this system include increased operational efficiency, reduced labor costs, improved safety, and enhanced material handling capacity. By automating the material conveying process, the system minimizes the risk of human error and accidents, leading to a safer working environment. Additionally, the consistent material flow provided by the system ensures stable production processes and reduces downtime caused by material shortages or blockages. The durability and low maintenance requirements of the equipment also contribute to long-term cost savings for businesses.
Conclusion
In conclusion, the tonne bag material conveying system equipment from HeadPowder Engineering Co., Ltd. is a reliable and efficient solution for bulk material handling. Its working principle, based on mechanical transmission and automation, ensures smooth and continuous material flow. The key features, including high capacity, adjustable speed, safety measures, and user-friendly control systems, make it an ideal choice for various industrial applications. By investing in this equipment, businesses can enhance their operational efficiency, improve safety standards, and achieve long-term cost savings. HeadPowder Engineering Co., Ltd. remains committed to providing high-quality and customized solutions to meet the diverse needs of its clients in Shandong, China, and beyond.