

Working Principle and Features of Brown Sugar Material Handling System Equipment
For those in the sugar processing industry, particularly those dealing with brown sugar, the efficiency and reliability of material handling systems are critical to operational success. The brown sugar material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a prime example of advanced engineering tailored to meet the specific demands of this sector. This article will delve into the working principle and key features of this equipment, providing insights into how it enhances productivity and ensures consistent quality in brown sugar processing operations.
Company Background and Expertise
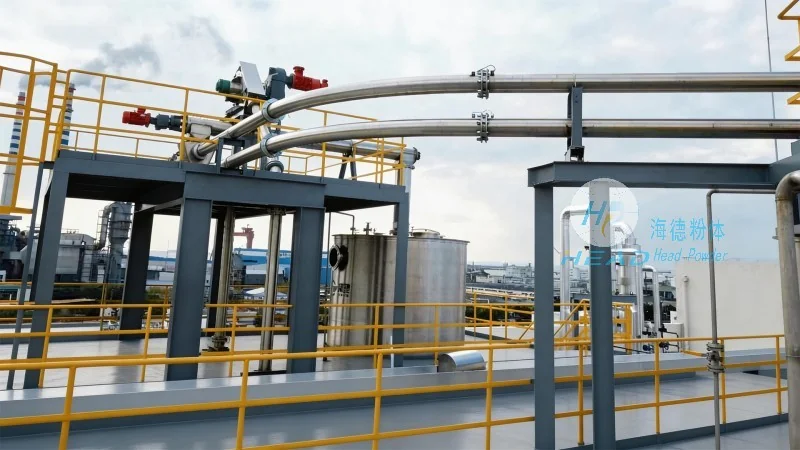
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer in the field of powder and bulk material handling solutions. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality equipment that meets international standards. Their expertise in designing and manufacturing material handling systems for various industries, including the sugar sector, positions them as a trusted partner for businesses seeking reliable and efficient solutions.
Understanding the Brown Sugar Material Handling System
The brown sugar material handling system is designed to facilitate the seamless movement of brown sugar from storage to processing units, and subsequently to packaging or storage areas. This system integrates various components such as conveyors, elevators, and storage silos, all working in tandem to ensure a continuous and controlled flow of material. The equipment is engineered to handle the unique characteristics of brown sugar, including its moisture content, density, and potential stickiness, which can pose challenges in traditional handling methods.
Working Principle of the Equipment
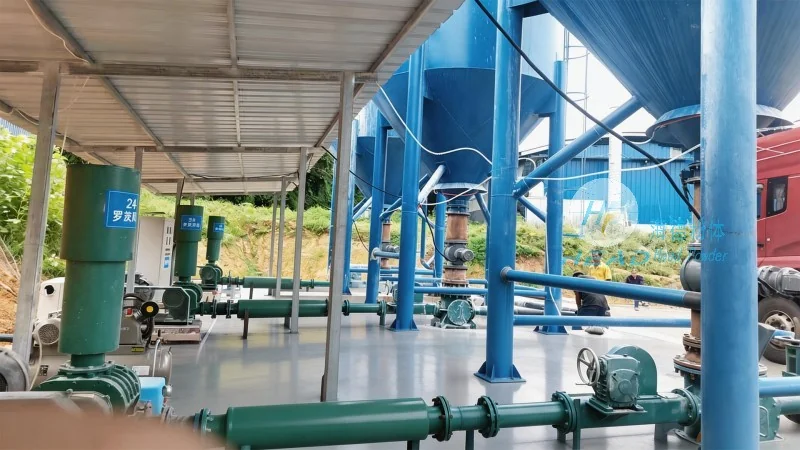
The core of the brown sugar material handling system lies in its automated and integrated workflow. The process typically begins with the loading of brown sugar into a storage silo or hopper. From there, the material is transferred to a conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the specific application and layout of the facility. The conveyors are equipped with advanced control systems that regulate the speed and direction of material movement, ensuring precise and efficient transport. Additionally, the system may incorporate feeding mechanisms and distribution units that direct the brown sugar to different processing lines or storage locations as required.
Key Features and Advantages
The brown sugar material handling system by HeadPowder is characterized by several notable features that enhance its performance and usability. One of the primary features is its modular design, which allows for easy customization and expansion to accommodate changing production needs. This flexibility is particularly valuable in industries where production volumes fluctuate or where new processing technologies are introduced. Another key feature is the integration of advanced monitoring and control systems. These systems provide real-time data on material flow, equipment performance, and operational efficiency, enabling operators to make informed decisions and quickly address any issues that may arise.
Furthermore, the equipment is designed with durability and low maintenance in mind. High-quality materials and robust construction ensure that the system can withstand the rigors of continuous operation, reducing downtime and maintenance costs over the long term. The system also incorporates safety features, such as emergency stop buttons and overload protection, to safeguard both personnel and equipment. These features align with industry standards and contribute to a safer working environment.
Enhancing Operational Efficiency and Product Quality
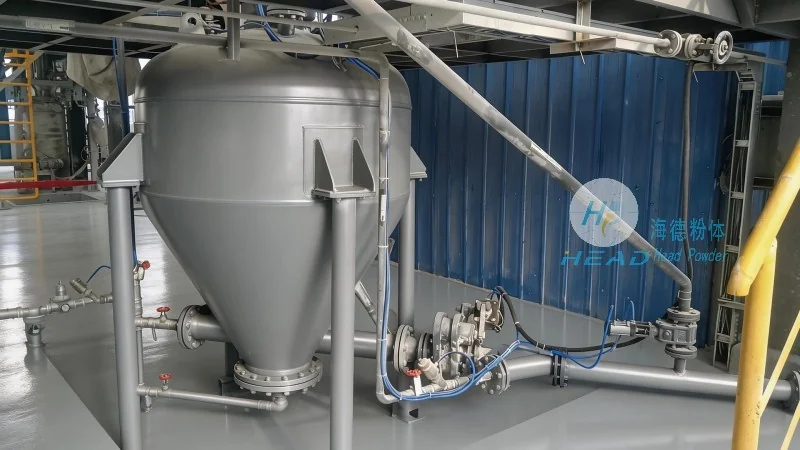
By implementing the brown sugar material handling system, sugar processing facilities can achieve significant improvements in operational efficiency. The automated nature of the system reduces the need for manual labor, minimizing human error and increasing the speed of material transfer. This leads to higher throughput and reduced processing times, which are crucial for meeting market demands and maintaining competitiveness. Moreover, the precise control over material movement ensures consistent quality in the final product. By preventing contamination and maintaining uniform moisture levels, the system helps to preserve the natural characteristics of brown sugar, resulting in a product that meets or exceeds customer expectations.
Conclusion
In summary, the brown sugar material handling system equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient handling of brown sugar. Its working principle, based on integrated automation and precise control, combined with its key features such as modularity, advanced monitoring, and durability, makes it an ideal choice for sugar processing operations. By leveraging this equipment, businesses can enhance their operational efficiency, improve product quality, and maintain a competitive edge in the market. As a trusted manufacturer with a strong presence in China, HeadPowder continues to provide innovative solutions that meet the evolving needs of the industry.