

Working Principle and Features of Tonne Bag Unpacking and Powder Conveying Equipment
Efficient handling of bulk powders is a critical challenge in many industrial sectors, from pharmaceuticals and food processing to chemical manufacturing. The tonne bag unpacking and powder conveying equipment offered by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges with a robust, automated solution designed to streamline material transfer and enhance operational efficiency.
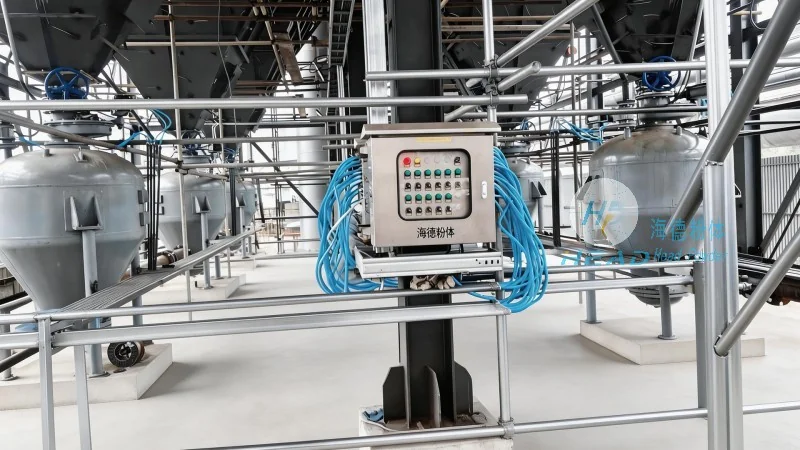
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced powder handling systems that integrate seamlessly into existing production lines. The company's commitment to quality and innovation has positioned it as a trusted partner for businesses seeking reliable equipment to manage bulk materials. This article explores the working principles and key features of their tonne bag unpacking and powder conveying equipment, highlighting how it can optimize workflow and reduce operational costs.
Working Principle of Tonne Bag Unpacking and Powder Conveying Equipment
The equipment operates through a series of coordinated steps that ensure safe and efficient material transfer from the tonne bag to the processing line. The process begins with the placement of the tonne bag on a dedicated loading platform. A mechanical system, often incorporating a hydraulic or pneumatic actuator, then opens the bag's top, allowing the powder to flow into a hopper or direct into the conveying system. This step eliminates the need for manual bag opening, reducing labor costs and minimizing the risk of dust exposure.
Once the bag is opened, the powder is transferred to a screw conveyor or pneumatic conveyor, depending on the specific application. The screw conveyor provides a continuous, low-speed transport of the material, while the pneumatic system is ideal for handling fine powders that require minimal contact and reduced risk of contamination. The conveying component is equipped with variable speed drives, allowing operators to adjust the flow rate according to the material's characteristics and processing requirements. This flexibility ensures optimal performance across a wide range of powder types, from free-flowing to cohesive materials.
The system also includes a dust collection and filtration unit to maintain a clean working environment. As the powder is transferred, any airborne particles are captured by a high-efficiency particulate air (HEPA) filter, preventing contamination of the product and protecting the health of operators. The integrated control panel allows for real-time monitoring of the process, with alarms set to alert staff in case of blockages or other issues. This proactive approach to maintenance ensures minimal downtime and consistent performance.
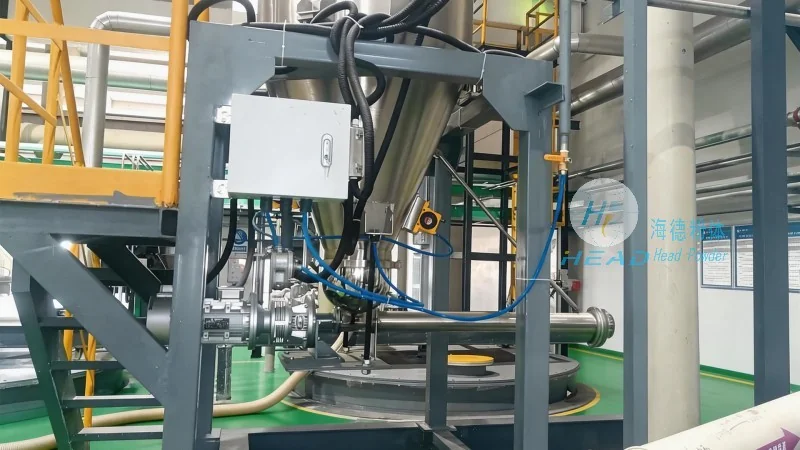
Key Features of the Tonne Bag Unpacking and Powder Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. has incorporated several advanced features into their equipment to enhance functionality and user experience. One of the standout features is the automated bag opening mechanism, which reduces manual intervention and improves safety. The system is designed to handle bags of various sizes and materials, including woven polypropylene and kraft paper, ensuring versatility across different industries.
The equipment is also equipped with a material flow monitoring system that provides real-time data on the quantity and speed of powder transfer. This feature allows for precise inventory management and helps prevent overfilling or underfilling of processing vessels. Additionally, the conveying components are constructed from food-grade or chemical-resistant materials, depending on the application, ensuring compliance with industry standards and preventing cross-contamination.
Another key feature is the energy-efficient design, which incorporates variable frequency drives (VFDs) to adjust motor speed based on the load. This not only reduces energy consumption but also extends the lifespan of the equipment by minimizing wear and tear. The system is also designed for easy maintenance, with quick-release components and accessible parts that allow for rapid servicing without extensive downtime.
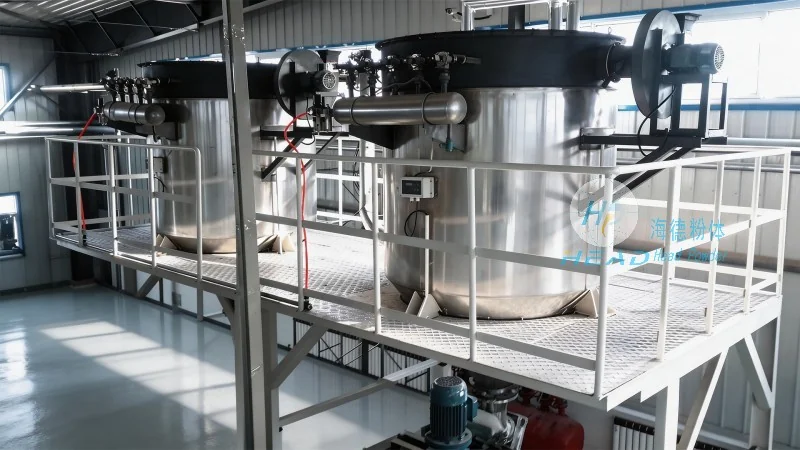
The control system is user-friendly, featuring a touchscreen interface that simplifies operation and reduces the learning curve for new staff. The interface displays all critical parameters, including flow rate, pressure, and temperature, providing operators with a clear overview of the process. The system also includes a data logging function, allowing for historical analysis of performance and identification of trends that may indicate maintenance needs.
Benefits and Applications
The tonne bag unpacking and powder conveying equipment from HeadPowder offers numerous benefits to businesses in various sectors. For pharmaceutical manufacturers, the system ensures a clean, sterile environment, critical for maintaining product quality and regulatory compliance. In the food industry, the equipment's hygienic design and material selection meet stringent safety standards, reducing the risk of contamination and ensuring product safety. Chemical manufacturers benefit from the system's ability to handle a wide range of materials, including hazardous powders, with minimal risk of exposure.
One of the primary advantages is the reduction in labor costs. By automating the bag opening and conveying process, businesses can reduce the number of operators required for material handling, freeing up staff for more value-added tasks. Additionally, the system's efficiency reduces material waste by minimizing spillage and ensuring accurate transfer of the powder. This leads to cost savings and improved profitability over time.
The equipment is also highly adaptable, making it suitable for a variety of applications, from small-scale production lines to large-scale industrial facilities. Whether used in a laboratory setting or a full-scale manufacturing plant, the system can be customized to meet specific requirements, ensuring optimal performance and integration with existing infrastructure.