

Working Principle and Features of Cement Aggregate Powder Conveying Systems
Understanding the working principle and features of cement aggregate powder conveying systems is crucial for industries that rely on efficient material handling in construction and manufacturing. These systems are designed to transport bulk materials such as cement, aggregates, and other powders with precision and reliability, ensuring smooth operations in production lines.
Overview of Cement Aggregate Powder Conveying Systems
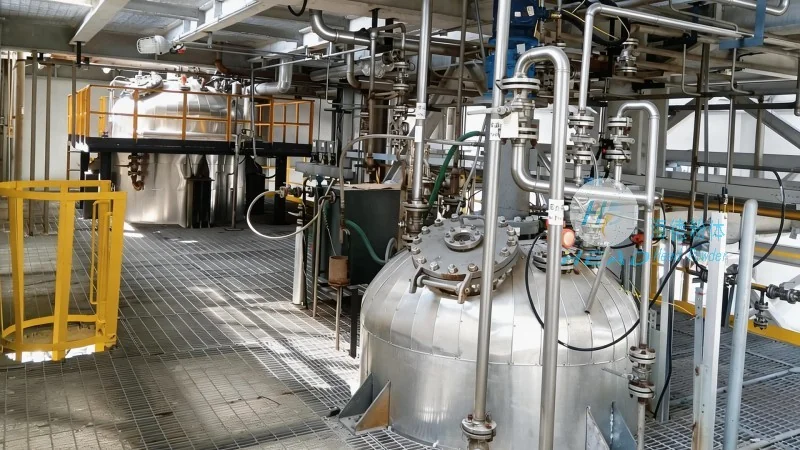
Cement aggregate powder conveying systems are sophisticated equipment used to move large volumes of dry bulk materials from one location to another within industrial facilities. The core components typically include feed hoppers, conveyor belts or screw conveyors, control panels, and dust collection systems. Each component plays a vital role in ensuring the system operates efficiently and safely. The feed hopper is responsible for storing and feeding the material into the conveyor, while the conveyor itself transports the material to the desired destination. Control panels allow operators to monitor and adjust the system's parameters, such as speed and pressure, to maintain optimal performance. Dust collection systems are essential for maintaining air quality and preventing dust accumulation, which can affect both safety and product quality.
Working Principle of the System
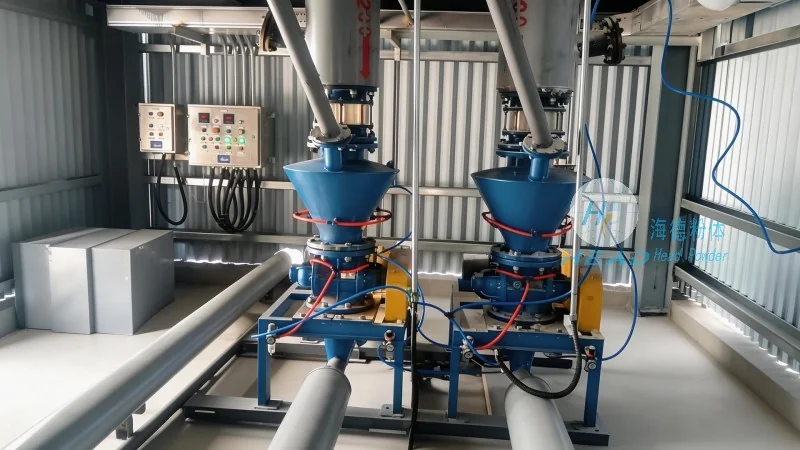
The working principle of a cement aggregate powder conveying system involves several key steps. First, the bulk material is loaded into the feed hopper. The hopper then releases the material into the conveyor mechanism, which can be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the system design. The conveyor transports the material through a series of pipes or channels to the discharge point. During this process, the system may incorporate features like vibration or agitation to prevent material bridging and ensure consistent flow. The control panel monitors the system's performance, adjusting the conveyor speed or pressure as needed to maintain a steady flow rate. Finally, the material is discharged into a storage silo or directly into a processing unit, completing the conveying process.
Key Features and Advantages
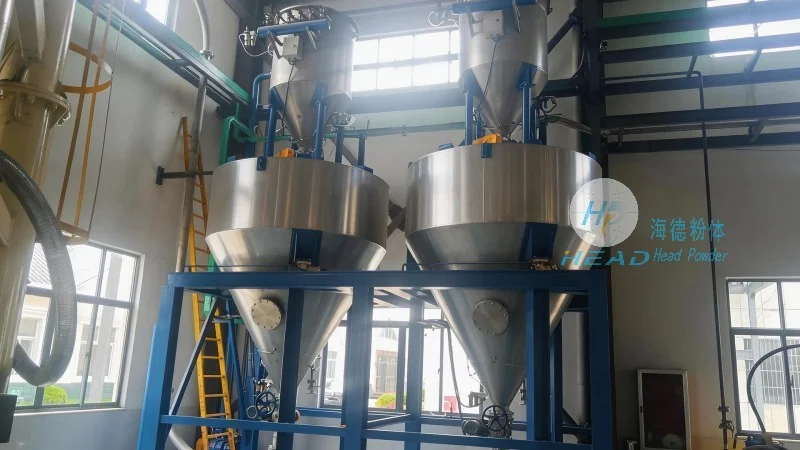
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in developing advanced cement aggregate powder conveying systems. These systems are characterized by several key features that enhance their performance and reliability. One of the primary features is the use of high-quality materials and robust construction, ensuring durability and long service life. The systems are designed to handle a wide range of materials, including cement, sand, gravel, and other powders, with consistent performance. Another important feature is the integration of advanced control technology, which allows for precise monitoring and adjustment of the conveying process. This technology helps maintain optimal flow rates and prevents system failures, reducing downtime and maintenance costs. Additionally, the systems are equipped with efficient dust collection and filtration systems, ensuring compliance with environmental regulations and maintaining a clean working environment. The modular design of these systems allows for easy installation and maintenance, making them suitable for various industrial applications.
Application in Industrial Settings
Cement aggregate powder conveying systems are widely used in the construction industry, where they are essential for transporting raw materials to concrete mixing plants and other production facilities. In manufacturing, these systems are used in industries such as cement production, mining, and chemical processing, where bulk material handling is critical. The systems are also used in agricultural and food processing applications, where they help transport grains, powders, and other bulk materials. The efficiency and reliability of these systems contribute to increased productivity and reduced operational costs in various industrial settings.
Conclusion
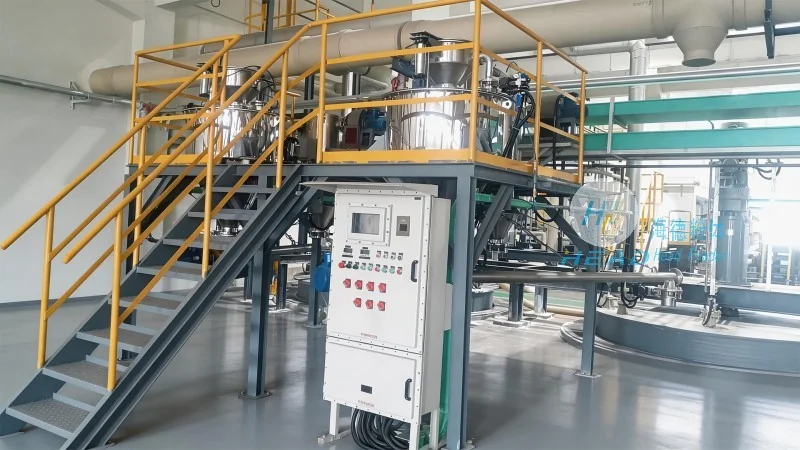
In summary, cement aggregate powder conveying systems are essential equipment for industries that require efficient and reliable bulk material handling. The working principle and features of these systems, as developed by companies like Shandong HeadPowder Engineering Co., Ltd., ensure optimal performance and durability. By understanding the key components and advantages of these systems, industries can make informed decisions when selecting the right equipment for their material handling needs. The integration of advanced technology and robust construction in modern conveying systems has significantly improved their efficiency and reliability, making them indispensable in today's industrial operations.