

Working Principle and Features of Sulfur Powder Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems for various bulk materials, including sulfur powder. This article explores the working principle and key features of sulfur powder pneumatic conveying lines, highlighting how these systems enhance operational efficiency and safety in industrial applications.
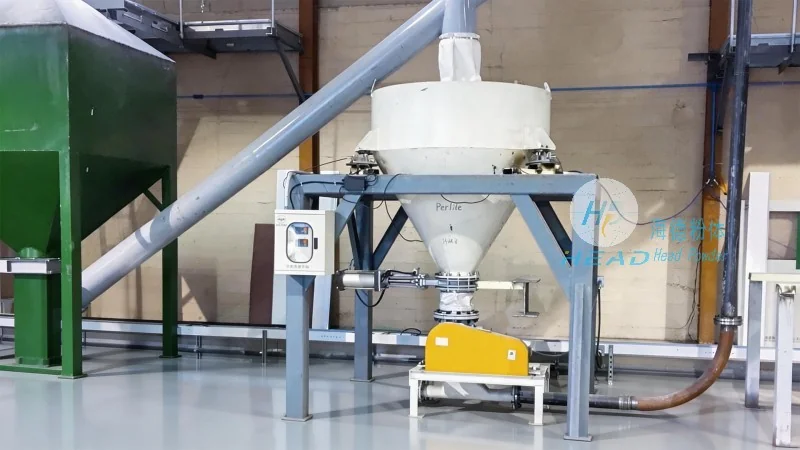
Overview of Sulfur Powder Pneumatic Conveying Systems
Sulfur powder pneumatic conveying systems are engineered to transport sulfur powder from storage silos or processing units to processing equipment or storage locations using a combination of air and pressure. The system typically consists of several core components, including a hopper, a rotary valve, a conveying pipe, a filter, and a dust collector. These components work in tandem to ensure efficient, reliable, and safe material transport.
The Working Principle of Sulfur Powder Pneumatic Conveying Lines
The operation of a sulfur powder pneumatic conveying line begins with the material being fed into the hopper from a storage silo. The rotary valve then controls the flow of sulfur powder into the conveying pipe, where it is mixed with high-velocity air. The air, often supplied by a blower or compressor, creates a flow that propels the sulfur powder through the pipeline. The conveying process relies on the principle of pneumatic transport, where the material is suspended and transported by the air stream. The system may use either positive pressure (pressure conveying) or negative pressure (vacuum conveying), depending on the specific application and system design. Positive pressure systems are commonly used for long-distance or high-capacity transport, as they can maintain consistent pressure and flow rates. Negative pressure systems are often employed for shorter distances or when the material needs to be transported from multiple sources to a single destination, as they can effectively capture and transport dust-laden air.
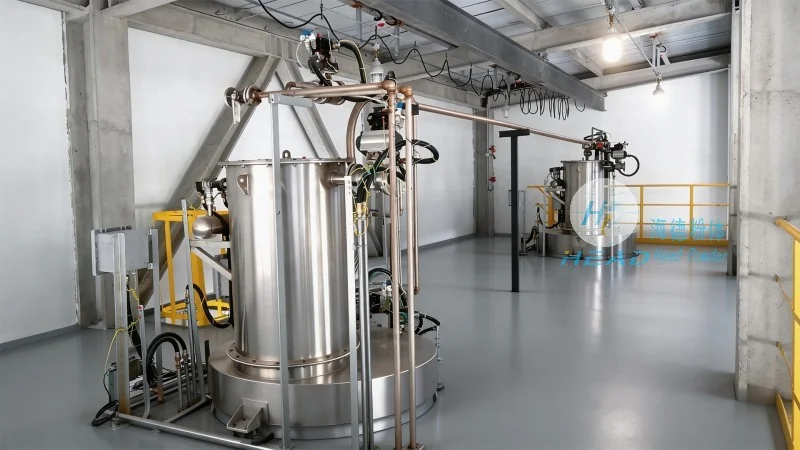
Key Features of Sulfur Powder Pneumatic Conveying Systems
HeadPowder's sulfur powder pneumatic conveying systems are characterized by several distinct features that enhance performance and reliability. One of the primary advantages is the ability to handle sulfur powder in a dust-free environment, which is critical for maintaining product quality and preventing contamination. The systems are designed to minimize material degradation and agglomeration, ensuring that the sulfur powder remains in a free-flowing state throughout the conveying process. Additionally, the use of advanced filtration and dust collection systems helps to maintain air quality and comply with environmental regulations, making these systems suitable for a wide range of industrial applications.
Efficiency and Safety in Industrial Applications
The efficiency of sulfur powder pneumatic conveying systems is evident in their ability to transport large volumes of material with minimal downtime and maintenance. The systems are equipped with automated controls that monitor flow rates, pressure, and air quality, ensuring optimal performance. Safety features, such as explosion-proof components and emergency shut-off valves, are integrated into the design to protect personnel and equipment from potential hazards associated with sulfur powder handling. These features make the systems suitable for use in environments where safety is a top priority, such as chemical processing plants and fertilizer production facilities.
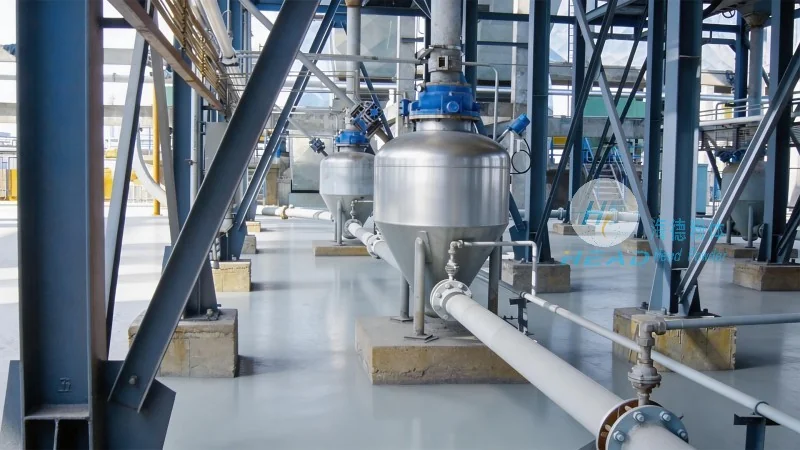
Customization and Reliability
HeadPowder understands that each industrial application has unique requirements, and therefore, offers customized pneumatic conveying solutions tailored to specific needs. The company's engineers work closely with clients to design systems that meet their operational demands, including material characteristics, transport distances, and environmental considerations. The use of high-quality materials and components ensures the long-term reliability of the systems, reducing the need for frequent repairs and replacements. This focus on customization and reliability has made HeadPowder a trusted partner for businesses seeking efficient and safe sulfur powder handling solutions.
Conclusion
Sulfur powder pneumatic conveying systems, as exemplified by those offered by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated and effective solution for transporting sulfur powder in industrial settings. By leveraging the principles of pneumatic transport and incorporating advanced design features, these systems enhance operational efficiency, ensure product quality, and maintain safety standards. The combination of technical expertise, customization capabilities, and commitment to quality makes HeadPowder a leading provider of sulfur powder pneumatic conveying solutions in China and beyond.