

Working Principle and Features of Ammonium Nitrate Pneumatic Conveying Systems
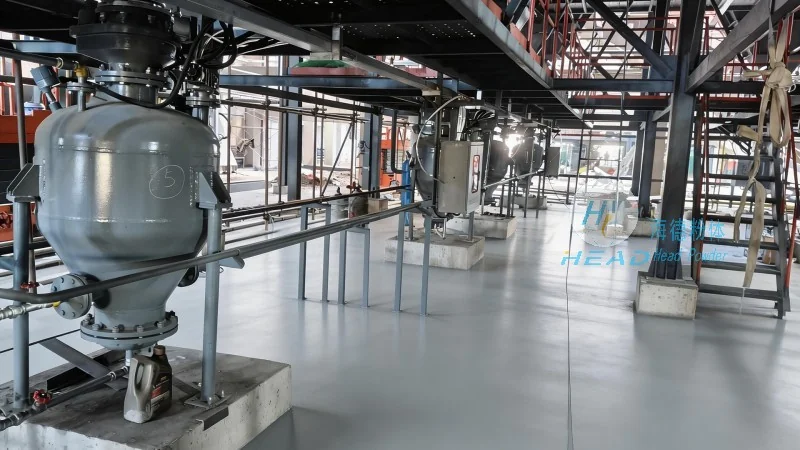
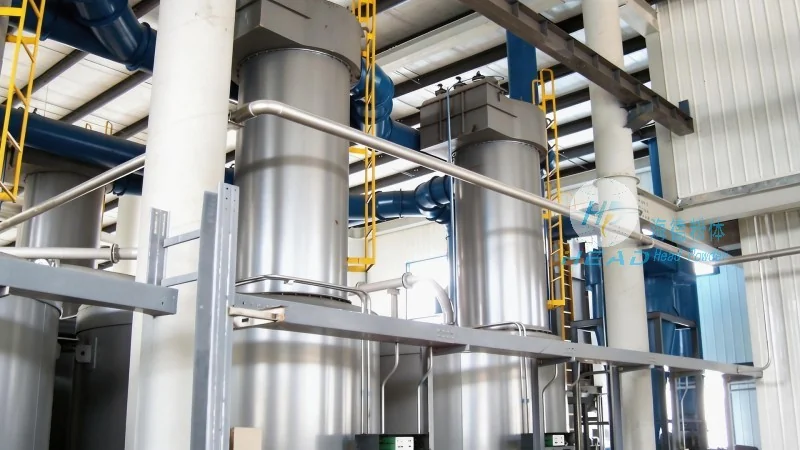
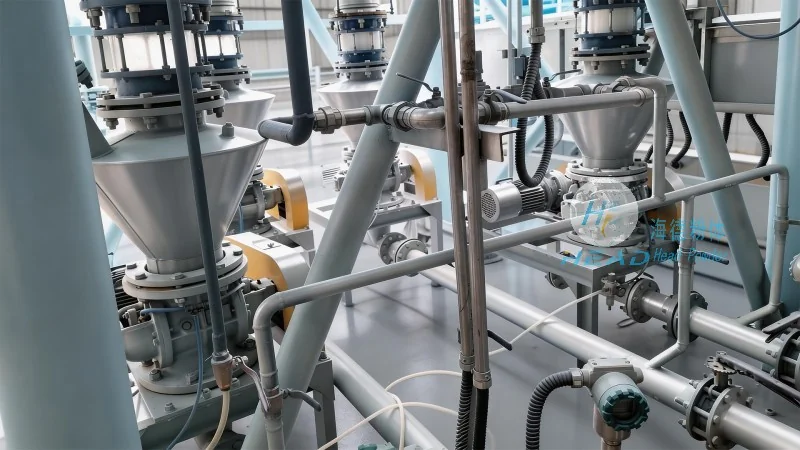
Ammonium nitrate, a widely used industrial chemical, often requires efficient and reliable transport solutions. The pneumatic conveying system, particularly designed for handling ammonium nitrate, operates on the principle of using air or gas to move bulk materials through a pipeline. This method eliminates the need for mechanical components like belts or buckets, offering a more hygienic and low-maintenance approach. The system typically consists of a hopper, a conveyor line, and a receiver. The material is fed into the hopper, where it is then drawn into the pipeline by a vacuum or pressure created by a fan or blower. As the air flows through the system, it carries the ammonium nitrate particles along the pipeline to the desired destination. The design of the system, including the type of air flow (e.g., positive or negative pressure), is crucial in ensuring the efficient and safe transport of ammonium nitrate, which is sensitive to moisture and temperature changes.
Key Features of Ammonium Nitrate Pneumatic Conveying Systems
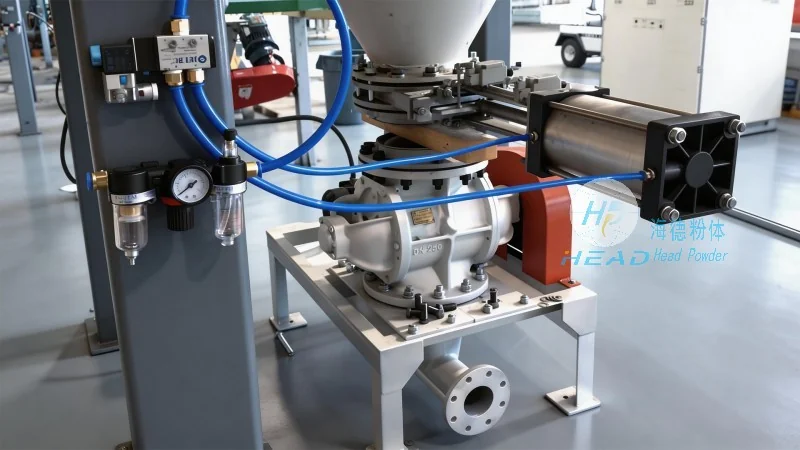
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, offers advanced pneumatic conveying systems tailored for ammonium nitrate applications. These systems are engineered with several key features that enhance performance and safety. Firstly, the system is designed to maintain a controlled environment, minimizing exposure to moisture and preventing caking or clumping of the ammonium nitrate. This is achieved through the use of sealed pipelines and proper air filtration. Secondly, the equipment is constructed from materials resistant to corrosion and chemical reactions, ensuring durability and longevity. The conveying speed can be adjusted to optimize material flow, reducing the risk of blockages or damage to the product. Additionally, the system incorporates safety features such as pressure relief valves and emergency shut-off mechanisms, adhering to industry standards for handling hazardous materials. The modular design of the system allows for easy installation and maintenance, reducing downtime and operational costs. By integrating these features, the pneumatic conveying system provides a reliable and efficient solution for transporting ammonium nitrate, meeting the demands of various industrial applications.
Application and Benefits in Industrial Settings
The application of ammonium nitrate pneumatic conveying systems is prevalent in industries such as fertilizer production, chemical manufacturing, and mining. In fertilizer plants, the system efficiently moves ammonium nitrate from storage silos to processing units, ensuring a continuous supply of raw material. The benefits of using this system include reduced labor costs, improved safety due to enclosed transport, and increased productivity. The system's ability to handle large volumes of material in a short time makes it ideal for high-throughput operations. Furthermore, the low maintenance requirements and the ability to operate in a controlled environment contribute to overall cost savings. The system's design also allows for easy integration with existing production lines, minimizing the need for major infrastructure changes. By leveraging the advanced technology from Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, industries can enhance their operational efficiency and ensure the safe handling of ammonium nitrate, a critical component in many industrial processes.