

Working Principle and Features of Ammonium Sulfate Pneumatic Conveying Systems
Ammonium sulfate, a widely used chemical fertilizer, requires efficient and reliable handling systems to ensure smooth production and transportation processes. The pneumatic conveying system, particularly designed for ammonium sulfate, plays a crucial role in modern industrial applications. This article delves into the working principle and key features of such systems, highlighting their importance in optimizing material handling in chemical and agricultural sectors.
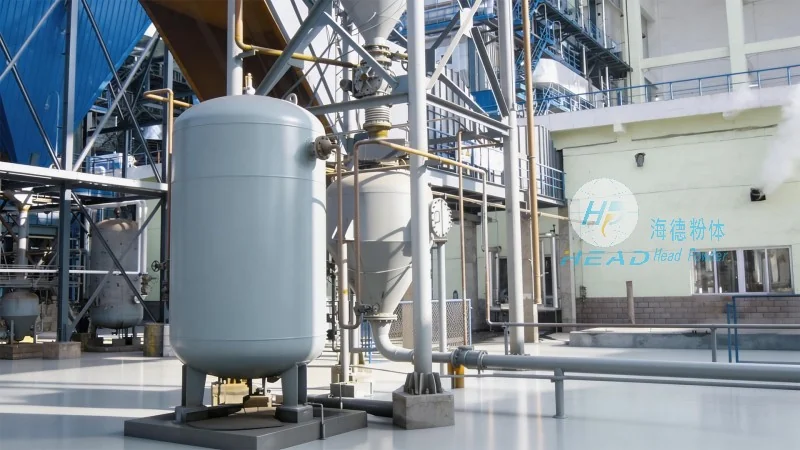
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and fabrication of advanced pneumatic conveying solutions tailored for various bulk materials, including ammonium sulfate. With a strong focus on precision engineering and customer-specific requirements, the company has established itself as a trusted partner in the industry, providing high-quality equipment that meets stringent operational standards.
The working principle of an ammonium sulfate pneumatic conveying system typically involves the use of compressed air to transport the material from a source point to a destination point. The system comprises several key components, including a hopper, a rotary airlock, a conveying line, and a receiver. The process begins with the material being fed into the hopper, where it is then drawn into the conveying line by the pressure difference created by the compressed air. The rotary airlock ensures a controlled and continuous flow of material, preventing backflow and maintaining system efficiency.
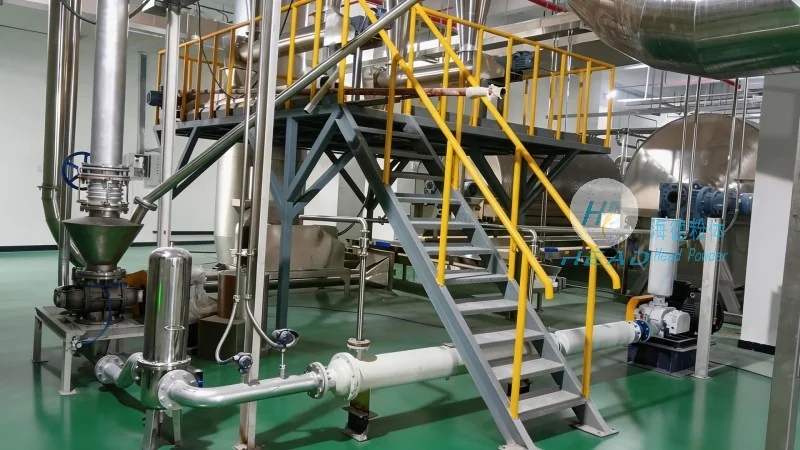
One of the primary advantages of pneumatic conveying systems for ammonium sulfate is their ability to handle fine and abrasive materials without causing excessive wear on equipment components. The design of the conveying line, often equipped with smooth or coated surfaces, minimizes friction and ensures the material is transported safely and efficiently. Additionally, the system can be configured to operate in both positive and negative pressure modes, providing flexibility in different industrial settings.
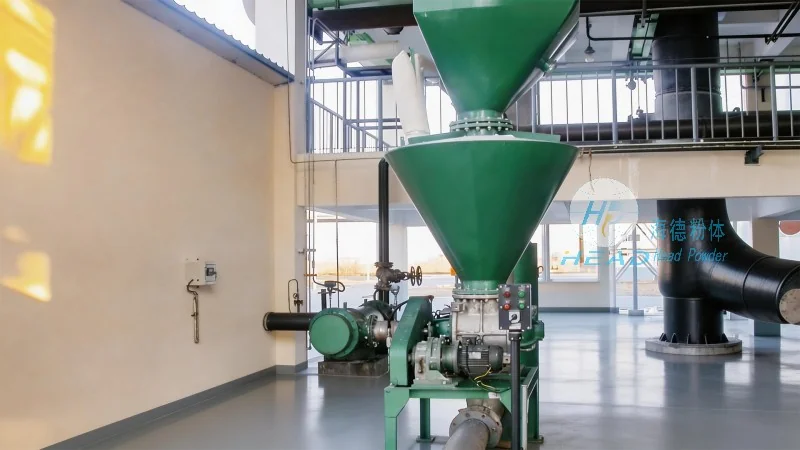
Another notable feature is the system's adaptability to varying production volumes and operational conditions. Shandong HeadPowder Engineering Co., Ltd. offers customized solutions that can be scaled to meet the specific needs of clients, whether for small-scale laboratory applications or large-scale industrial production. The company's expertise in material flow dynamics and system integration ensures that the conveying system operates at optimal performance levels, minimizing downtime and maintenance costs.
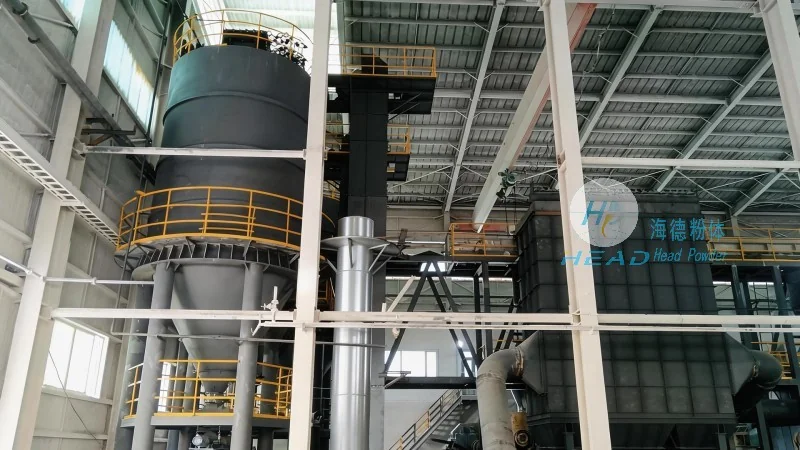
Efficiency and reliability are paramount in the operation of ammonium sulfate pneumatic conveying systems. The use of high-quality materials and robust construction ensures that the equipment can withstand the corrosive nature of ammonium sulfate and other chemical substances. Regular maintenance and monitoring of system parameters, such as air pressure and flow rates, are essential to maintain consistent performance and extend the service life of the components.
In conclusion, the pneumatic conveying system for ammonium sulfate, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient method for material handling. By understanding the working principle and leveraging the key features of such systems, industries can enhance their operational productivity while ensuring compliance with safety and environmental standards. The combination of advanced engineering and tailored solutions makes these systems indispensable in the modern chemical and agricultural sectors.