

What is a Monosodium Glutamate Material Handling System Equipment? What are its Design Principles?
Monosodium glutamate (MSG), a widely recognized flavor enhancer in the food industry, requires specialized equipment for efficient handling during production. The design and operation of a monosodium glutamate material handling system are critical to maintaining product quality, ensuring safety, and optimizing production efficiency. This article delves into the components, design principles, and practical applications of such systems, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
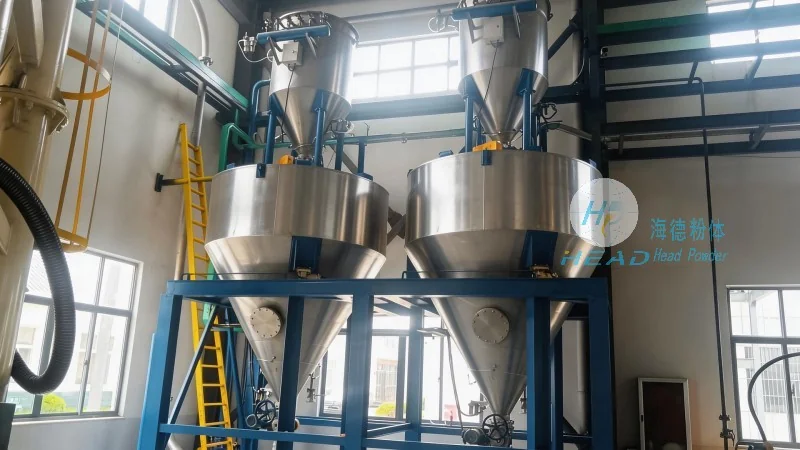
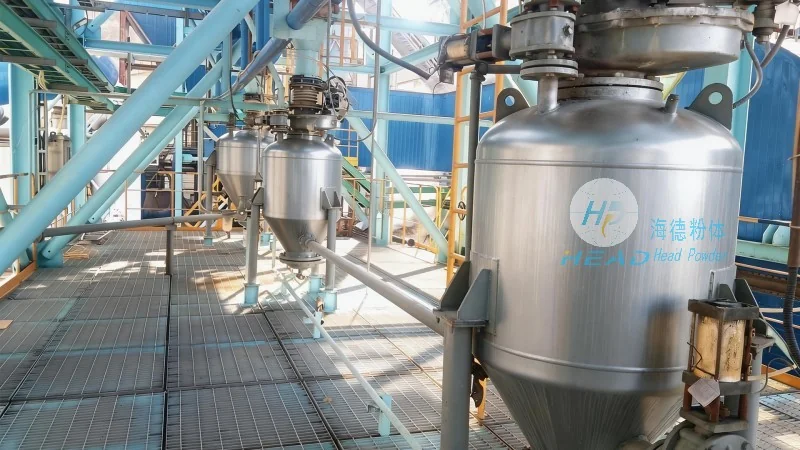
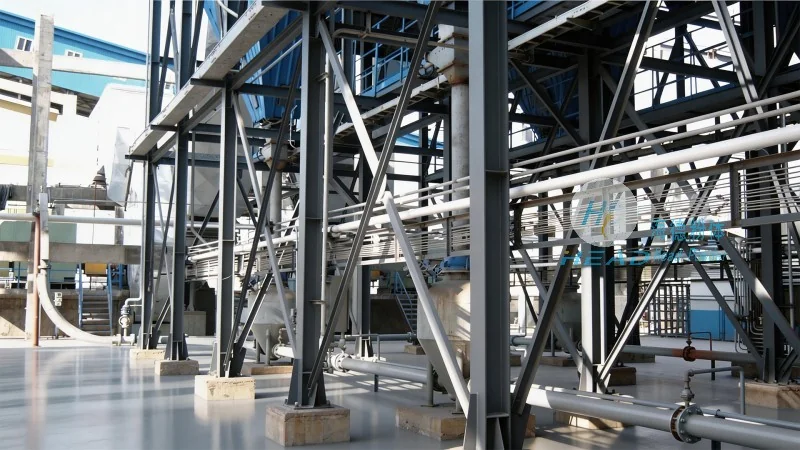
Introduction to Monosodium Glutamate Material Handling Systems
A monosodium glutamate material handling system is a comprehensive infrastructure designed to manage the entire lifecycle of MSG from raw material storage to finished product packaging. These systems are tailored to the unique properties of MSG, which includes its hygroscopic nature (ability to absorb moisture from the air) and the need for strict hygiene standards to prevent contamination. The system integrates various equipment, including bulk handling devices, storage silos, and control mechanisms, to ensure seamless material flow and operational reliability. For MSG manufacturers, a well-designed material handling system is not just a logistical tool but a key factor in maintaining competitive advantage and meeting regulatory requirements.
Key Components of the System
The core components of an MSG material handling system include bulk material transport equipment, storage facilities, and advanced control systems. Bulk material handling equipment, such as screw conveyors, belt conveyors, and bucket elevators, is used to move MSG from storage silos to processing units. Screw conveyors are particularly effective for handling dry MSG due to their ability to transport materials in a closed, sanitary environment, preventing dust and cross-contamination. Belt conveyors are often used for larger volumes and longer distances, providing high throughput and flexibility. Storage silos are typically made of stainless steel or reinforced concrete, with internal linings to prevent corrosion and ensure product integrity. These silos are equipped with temperature and humidity control systems to maintain optimal conditions for MSG storage. Control systems, often based on programmable logic controllers (PLCs), integrate sensors and actuators to monitor and regulate the flow of materials, ensuring precise control over the entire process.