

What is a Quartz Stone Material Handling System? What is its Design Principle?
Quartz stone material handling systems are specialized equipment designed to efficiently transport and manage quartz stone materials in industrial settings. These systems are crucial for optimizing production processes in industries such as stone fabrication, construction, and manufacturing. The primary goal of these systems is to enhance productivity, reduce labor costs, and ensure safe handling of heavy and abrasive quartz stone materials.
Key Components of Quartz Stone Material Handling Systems
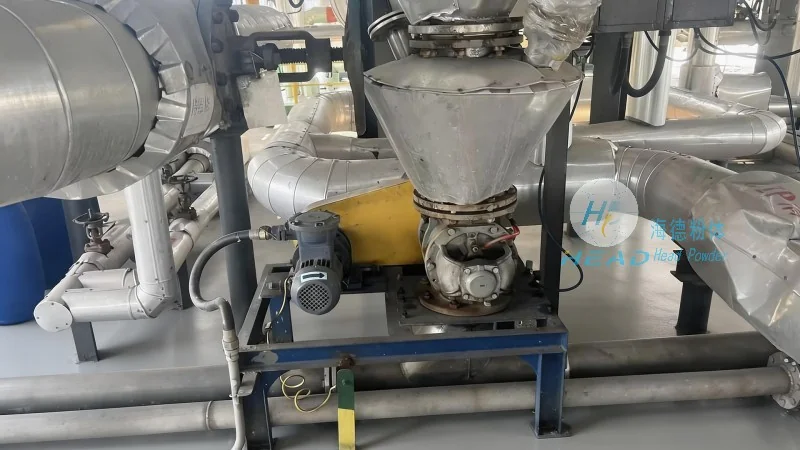
At the core of a quartz stone material handling system are several key components that work in tandem to facilitate smooth material movement. These components include conveyors, hoists, cranes, and specialized handling tools. Each component is engineered to handle the unique properties of quartz stone, which is known for its hardness, durability, and resistance to abrasion. For instance, conveyors are often equipped with heavy-duty belts or chains to withstand the weight and friction of quartz stone slabs or blocks. Hoists and cranes are designed with robust lifting mechanisms to safely lift and position large quartz stone pieces, while specialized tools like vacuum lifters or mechanical grippers ensure precise handling without damaging the stone surface.
Design Principles of Quartz Stone Material Handling Systems
The design of quartz stone material handling systems follows several fundamental principles aimed at maximizing efficiency and safety. First, the system must be capable of handling the high weight and abrasive nature of quartz stone. This involves using materials that can withstand wear and tear, such as stainless steel or high-grade alloys for conveyor components and lifting equipment. Second, the system must ensure minimal material damage during transport. This is achieved through smooth surfaces, gentle acceleration and deceleration, and specialized handling tools that avoid scratches or cracks on the quartz stone surface. Third, the system must prioritize operator safety. This includes features like emergency stop buttons, safety guards, and ergonomic controls to reduce the risk of accidents and fatigue. Additionally, the design considers space optimization, ensuring that the system fits within the existing industrial layout while maximizing material throughput.
Applications of Quartz Stone Material Handling Systems
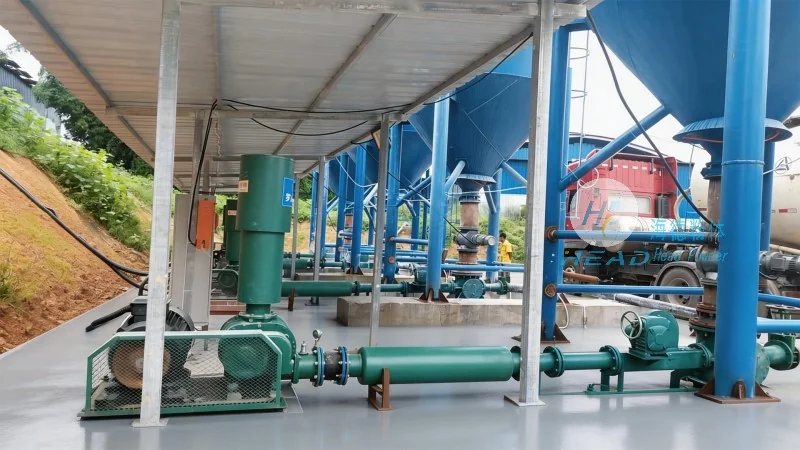
Quartz stone material handling systems are widely used in various applications across different industries. In stone fabrication plants, these systems are used to transport raw quartz stone blocks from storage to cutting and polishing stations. They also help move finished quartz stone slabs and countertops to packaging and shipping areas. In construction sites, the systems assist in moving large quartz stone panels for building facades or flooring installations. Furthermore, in manufacturing facilities that use quartz stone as a raw material, the systems ensure a continuous flow of materials from storage to processing equipment, reducing downtime and improving overall production efficiency.
HeadPowder's Expertise in Quartz Stone Material Handling Systems
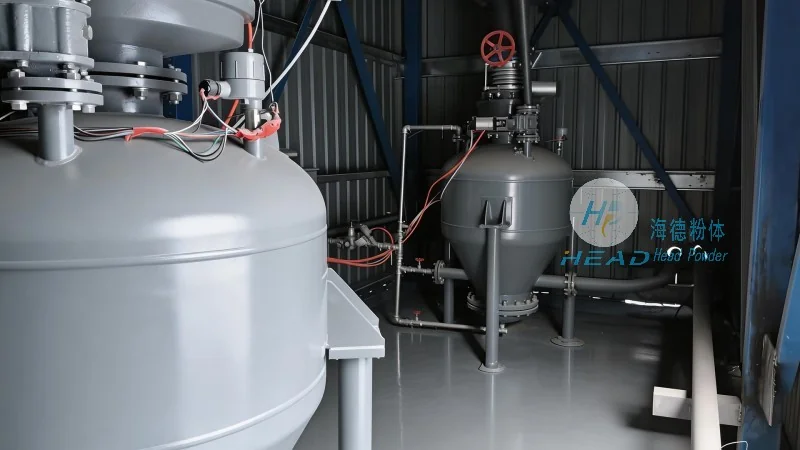
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in designing and manufacturing high-quality quartz stone material handling systems. With years of experience in the industry, HeadPowder has developed systems tailored to meet the specific needs of clients in the stone and construction sectors. The company's engineers leverage advanced technology and materials science to create systems that are not only efficient but also durable and cost-effective. For example, HeadPowder's conveyors are equipped with wear-resistant belts that can handle the abrasive nature of quartz stone, while their hoists and cranes are designed with safety features that comply with international standards. The company also provides customized solutions, adapting the systems to fit the unique requirements of each client's facility, whether it's a small-scale stone workshop or a large industrial plant.
Benefits of Using Quartz Stone Material Handling Systems
Implementing a quartz stone material handling system offers numerous benefits for businesses. Firstly, it significantly improves productivity by automating the material transport process, reducing the time and labor required for manual handling. This leads to faster production cycles and increased output. Secondly, the systems enhance safety by minimizing the risk of accidents caused by manual lifting and moving of heavy quartz stone pieces. This not only protects workers but also reduces the risk of workplace injuries and associated costs. Thirdly, the system reduces material damage, which is crucial for maintaining the quality of quartz stone products. By preventing scratches and cracks during transport, the systems help preserve the value of the stone and ensure consistent product quality. Additionally, the systems improve space utilization by optimizing the layout of the production area, allowing for more efficient use of available space and better workflow management.