

Efficient and Clean Solution for Coke Particle Transport: A Detailed Explanation of Pneumatic Convey
Efficient and clean transport of coke particles is a critical requirement in modern industrial processes, particularly in the steel and metallurgical sectors. Traditional methods such as belt conveyors or bucket elevators often face challenges related to material spillage, dust generation, and operational inefficiencies. In response to these challenges, pneumatic conveying technology has emerged as a superior alternative, offering enhanced efficiency, reduced environmental impact, and improved safety. This article delves into the principles, benefits, and practical applications of pneumatic conveying systems specifically designed for coke particle transport, with a focus on the solutions provided by Shandong HeadPowder Engineering Co., Ltd.
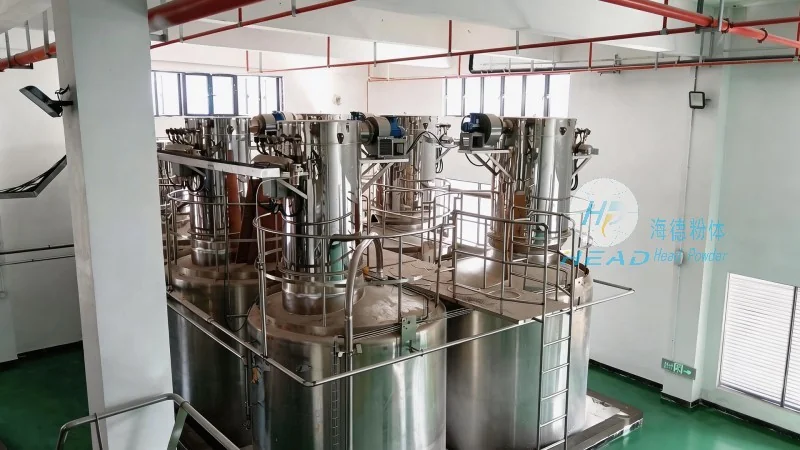
Introduction to Pneumatic Conveying for Coke Particle Transport
Pneumatic conveying, also known as air conveying, involves the transport of solid materials like coke particles through a pipeline using compressed air or other gas streams. Unlike mechanical systems that rely on physical contact and movement, pneumatic systems utilize the force of air to move materials, minimizing wear and tear on equipment while ensuring a more hygienic and dust-free operation. The core components of a pneumatic conveying system include a hopper for material storage, a conveyor line (typically made of stainless steel or other corrosion-resistant materials), a blower or compressor to generate the air flow, and a receiver or discharge point where the material is collected. For coke particles, which are often abrasive and heavy, the design of the system must consider factors such as particle size, density, and moisture content to ensure optimal performance.
HeadPowder's Expertise in Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of coke particle transport. With years of experience in the industry, HeadPowder has developed a deep understanding of the challenges associated with handling coke particles, including their high abrasiveness and potential for dust generation. The company's team of engineers and technicians work closely with clients to assess their specific requirements, from the volume of material to be transported and the distance over which it needs to be moved, to the environmental and safety standards that must be met. By leveraging advanced engineering principles and cutting-edge technology, HeadPowder ensures that its pneumatic conveying systems deliver consistent performance and reliability, even in the most demanding industrial environments.
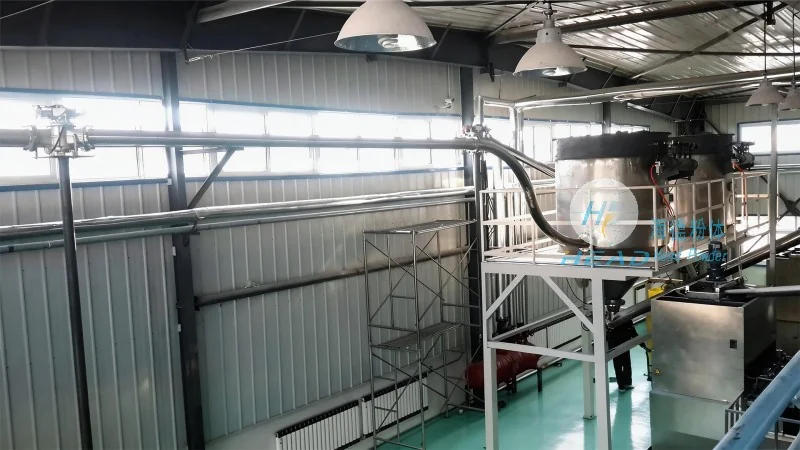
Key Features of Pneumatic Conveying Systems for Coke Particles
HeadPowder's pneumatic conveying systems for coke particles are equipped with several key features that enhance their efficiency and effectiveness. One of the primary features is the use of high-quality, corrosion-resistant materials for the conveyor line and components, which ensures durability and resistance to the abrasive nature of coke particles. The system also incorporates advanced control systems that allow for precise regulation of air pressure and flow, enabling optimal material transport without excessive energy consumption. Additionally, the design includes features such as in-line filters and dust collection systems to minimize environmental impact and maintain compliance with regulatory standards. The flexibility of the system allows for easy integration with existing industrial setups, reducing installation time and costs. Furthermore, the system's modular design enables scalability, allowing clients to expand their conveying capacity as their operations grow.
Benefits of Choosing Pneumatic Conveying for Coke Transport
Adopting pneumatic conveying technology for coke particle transport offers numerous benefits that contribute to improved operational efficiency and reduced costs. First and foremost, the system provides a significant reduction in material spillage and dust generation compared to traditional mechanical systems. This not only improves workplace safety by minimizing the risk of respiratory issues and other health hazards but also reduces the need for frequent cleaning and maintenance of equipment and surrounding areas. The efficiency of pneumatic conveying is another key advantage, as it can transport materials over longer distances with less energy consumption compared to other methods. This leads to lower operational costs and a more sustainable operation. Additionally, the system's ability to handle a wide range of particle sizes and densities makes it versatile for various industrial applications. The reduced maintenance requirements and longer service life of the equipment further contribute to cost savings over the long term. For industries that prioritize environmental responsibility and operational efficiency, pneumatic conveying is an ideal solution.
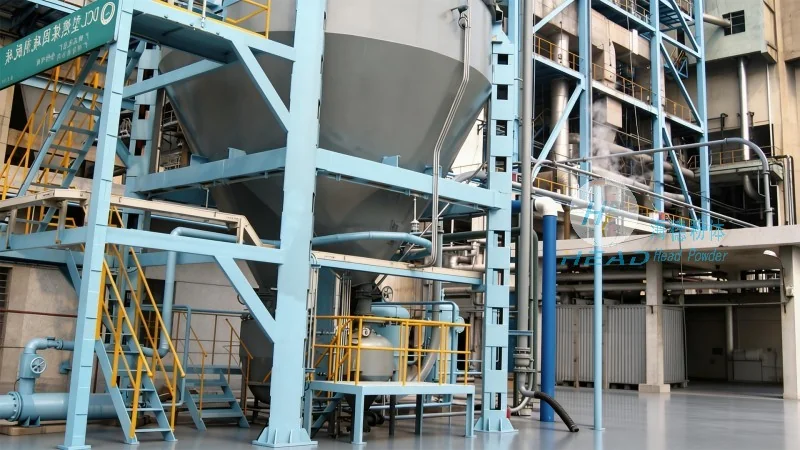
Application Scenarios and Performance in Industrial Settings
The effectiveness of pneumatic conveying systems for coke particles is demonstrated in various industrial settings. In steel plants, for example, coke is used as a fuel in blast furnaces, and efficient transport of coke particles from storage to the furnace is crucial for maintaining production rates. HeadPowder's systems have been successfully implemented in such plants, achieving high transport rates with minimal downtime. In metallurgical facilities, where coke is used as a reducing agent in the production of metals, the system ensures consistent material supply to the processing units. The performance of the system is measured by factors such as the conveying capacity, which refers to the volume of material transported per unit time, and the pressure drop across the system, which indicates the energy efficiency. HeadPowder's systems typically achieve high conveying capacities while maintaining low pressure drops, ensuring optimal performance. The reliability of the system is also a key factor, with minimal breakdowns and quick recovery times, which minimizes production disruptions. Case studies from clients in the industry have shown that implementing pneumatic conveying systems has led to significant improvements in operational efficiency and cost savings.
How HeadPowder Ensures Efficiency and Cleanliness in Transport Solutions
Shandong HeadPowder Engineering Co., Ltd. places a strong emphasis on ensuring that its pneumatic conveying systems for coke particles are both efficient and clean. The company follows a rigorous design and manufacturing process to ensure that all components meet the highest standards of quality and performance. The use of advanced materials and engineering techniques ensures that the system can withstand the harsh conditions associated with coke particle transport. HeadPowder also provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that the system operates at peak performance throughout its service life. The company's commitment to sustainability is reflected in its design choices, such as the inclusion of energy-efficient components and the use of recyclable materials. By focusing on both efficiency and cleanliness, HeadPowder provides clients with a reliable and environmentally friendly solution for coke particle transport. The company's reputation in the industry is built on its ability to deliver solutions that meet the specific needs of clients while adhering to the highest standards of quality and performance.