

[BEGIN HTML CONTENT]
Efficient and clean transport of camellia seeds is a critical factor in optimizing the overall processing workflow for oil extraction. Traditional methods often involve manual handling or mechanical conveyors that can introduce contamination, increase operational costs, and reduce product quality. In response to these challenges, air-powered conveying technology has emerged as a superior solution, offering a hygienic and efficient means to move camellia seeds through various stages of processing. This article provides a detailed overview of air-powered conveying systems, their benefits for camellia seed handling, and how HeadPowder Engineering Co., Ltd. leverages this technology to deliver tailored solutions for clients in Shandong, China.
Introduction to Air-Powered Conveying for Camellia Seed Handling
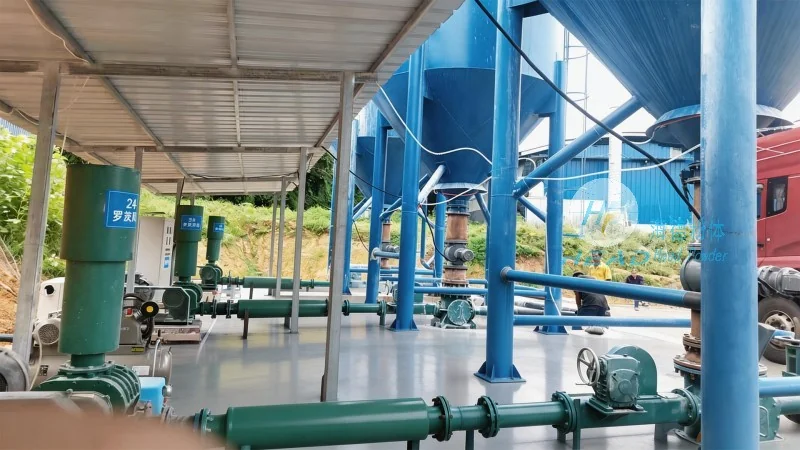
Camellia seeds, a key raw material for high-quality cooking oil and other value-added products, require careful handling to preserve their integrity and quality. The traditional methods of transporting these seeds, such as bucket elevators or belt conveyors, can lead to dust generation, product contamination, and increased labor costs. Air-powered conveying, also known as pneumatic conveying, addresses these issues by using compressed air to move seeds in a closed system. This technology ensures that the seeds remain clean, dry, and free from external contaminants, which is essential for maintaining the high standards of oil extraction processes.
How Air-Powered Conveying Works
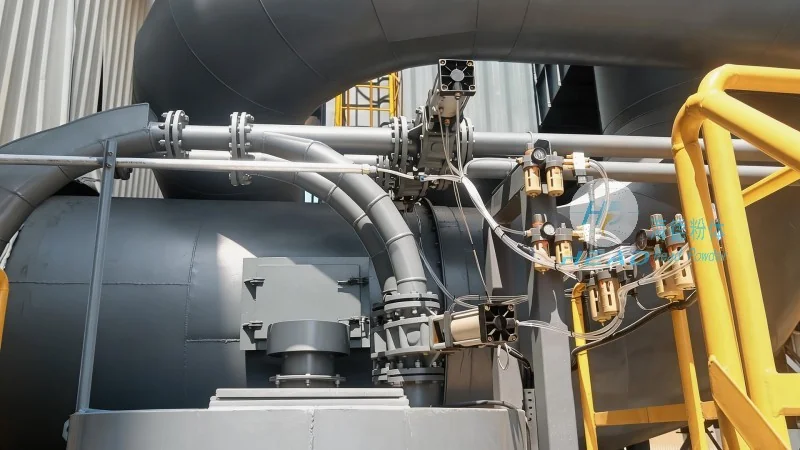
At its core, air-powered conveying systems operate by creating a pressure differential to move materials. There are two primary types: positive pressure and negative pressure systems. Positive pressure systems use a blower to force air and material through a pipeline, while negative pressure systems use a vacuum to draw material into the system. For camellia seeds, positive pressure systems are often preferred due to their ability to handle a wide range of particle sizes and their efficiency in moving materials over long distances. The system typically consists of a hopper, a conveyor line, and a discharge point, all connected by a network of pipes. The compressed air is introduced at the hopper, lifting the seeds and propelling them through the pipeline to the processing unit. This method ensures a continuous and controlled flow of seeds, minimizing downtime and maximizing throughput.
Key Advantages of Air-Powered Conveying for Camellia Seeds
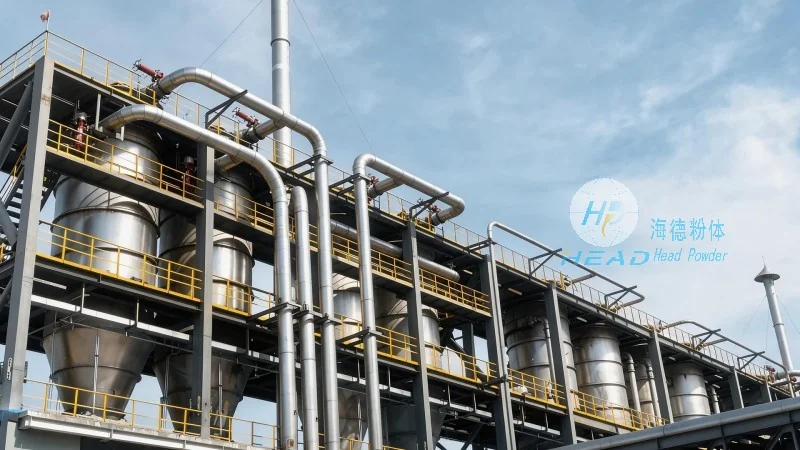
Implementing air-powered conveying for camellia seed transport offers several distinct advantages that directly impact operational efficiency and product quality. First, the hygienic nature of the system reduces the risk of contamination from external sources, which is crucial for maintaining the purity of the seeds before oil extraction. Unlike mechanical conveyors that may trap dust or debris, pneumatic systems keep the material enclosed, preventing cross-contamination and ensuring compliance with food safety regulations. Second, air-powered conveying significantly improves efficiency by enabling high-speed, continuous movement of seeds. This reduces the time required for material transfer, allowing processing lines to operate at optimal speeds and increasing overall production capacity. Third, the technology minimizes product damage and loss during transport. The gentle handling of seeds by air currents reduces breakage and bruising, which can affect oil yield and quality. Additionally, the closed system design reduces dust emissions, creating a cleaner working environment and lowering the risk of respiratory issues for workers. These benefits collectively contribute to lower operational costs and higher profitability for businesses involved in camellia seed processing.
HeadPowder's Expertise in Camellia Seed Conveying Solutions
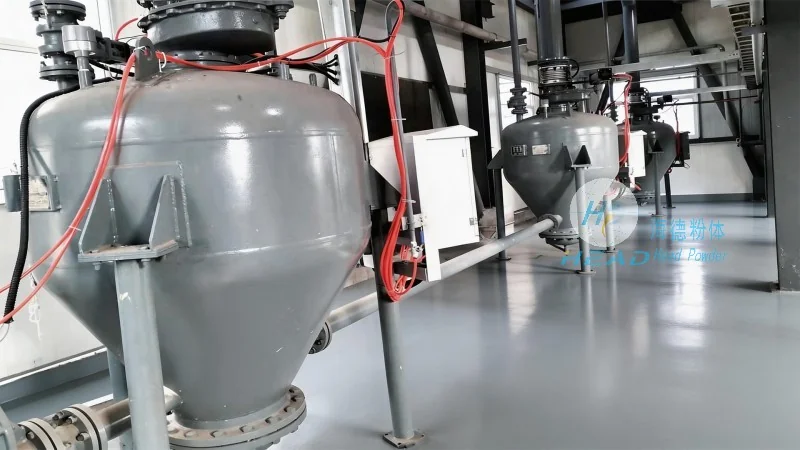
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in providing advanced air-powered conveying solutions tailored to the unique needs of camellia seed processing. With a deep understanding of the challenges faced by oil extraction facilities, HeadPowder designs and manufactures customized systems that optimize seed transport while maintaining the highest standards of cleanliness and efficiency. The company's team of engineers leverages years of experience in pneumatic conveying technology to develop solutions that address specific client requirements, such as varying seed sizes, processing line lengths, and environmental regulations. HeadPowder's commitment to quality is evident in its use of durable materials, such as stainless steel, which is resistant to corrosion and easy to clean, ensuring long-term performance and compliance with industry standards. By partnering with HeadPowder, clients gain access to a reliable and efficient conveying system that enhances their processing capabilities and supports their business growth. The company's location in Shandong, China, allows for close collaboration with clients, enabling on-site assessments and tailored system installations that meet the exact specifications of each facility. This local presence ensures timely support and maintenance, minimizing downtime and maximizing the return on investment for air-powered conveying systems.