

Working Principle and Features of Tote Bag Dust-Free Feeding Station for Powder Pneumatic Conveying
For industrial applications requiring efficient and clean handling of bulk powders, the tote bag dust-free feeding station is a critical component in pneumatic conveying systems. This equipment, designed by Shandong HeadPowder Engineering Co., Ltd. based in China, offers a solution that minimizes dust exposure while ensuring reliable material transfer. The following sections will explore the working principle and key features of this advanced powder handling system.
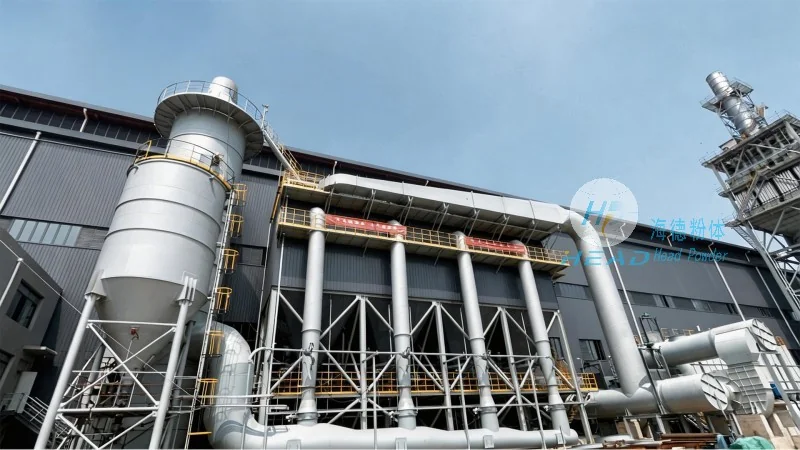
Introduction to Tote Bag Dust-Free Feeding Station
The tote bag dust-free feeding station is engineered to facilitate the safe and hygienic transfer of bulk powders from tote bags into pneumatic conveying pipelines. As a key part of the powder handling process, this system integrates several components to ensure seamless operation and maintain a clean environment. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, has developed this equipment to meet the stringent requirements of various industries, including food, pharmaceuticals, and chemical processing.
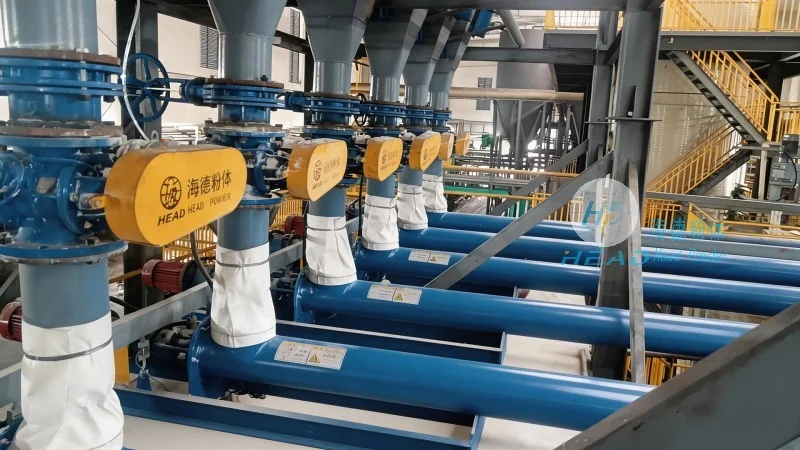
Working Principle of the Tote Bag Dust-Free Feeding Station
The operation of the tote bag dust-free feeding station is based on a pneumatic conveying mechanism that uses compressed air to transport powders. The process begins with the placement of a tote bag containing the bulk material onto the feeding station. The system then uses a combination of vacuum or pressure to draw the powder from the tote bag into the conveying line. The key steps in the working principle include:
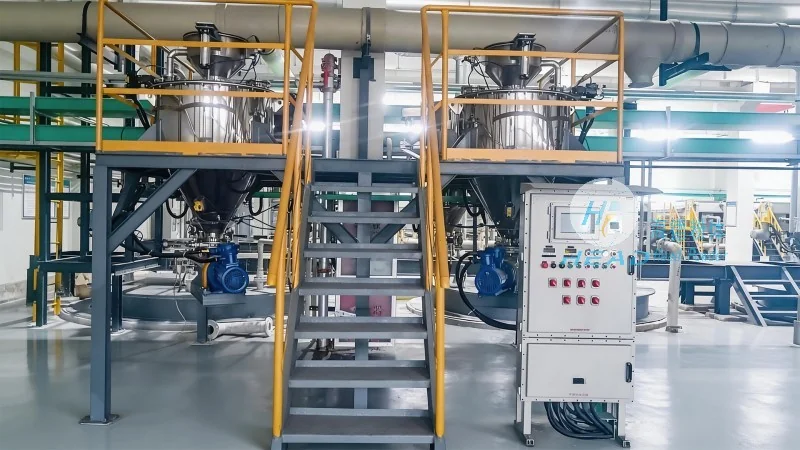
- Material Loading: The bulk powder is loaded into a tote bag, which is then positioned on the feeding station's loading platform.
- Air Intake and Conveying: Compressed air is introduced into the system, creating a flow that draws the powder from the tote bag into the conveying pipeline. The air velocity is carefully controlled to prevent particle degradation and ensure efficient transport.
- Dust Suppression: The feeding station incorporates dust suppression mechanisms, such as sealed hoppers and air filtration systems, to minimize the release of fine particles into the environment. This ensures compliance with occupational health and safety regulations.
- Material Discharge: Once the powder is fully transferred from the tote bag, the system can either discharge the empty bag or prepare it for reuse, depending on the operational requirements.
Key Features of the Tote Bag Dust-Free Feeding Station
Shandong HeadPowder Engineering Co., Ltd. has incorporated several advanced features into the tote bag dust-free feeding station to enhance its performance and usability. These features are designed to address the specific challenges of bulk powder handling, including dust control, material flow management, and operational efficiency. The main features include:
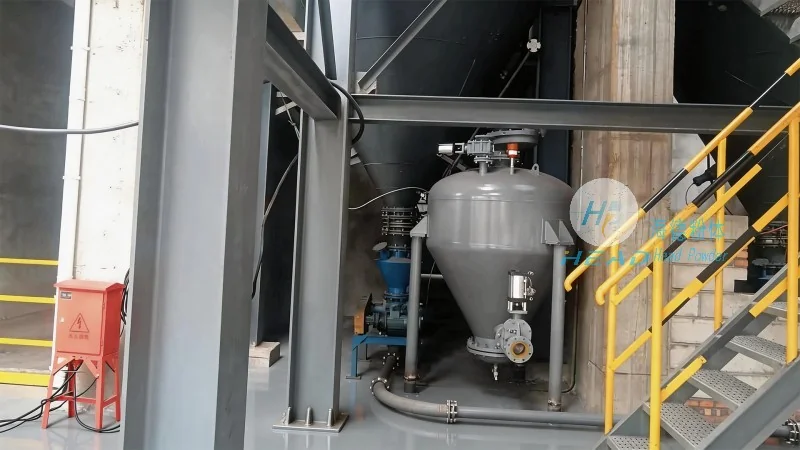
- Sealed Design for Dust-Free Operation: The equipment features a fully sealed hopper and feeding mechanism, which prevents dust from escaping into the surrounding environment. This design is particularly important in industries where dust contamination can affect product quality or pose health risks.
- Adjustable Air Flow Control: The system allows for precise control of air flow and pressure, enabling operators to optimize the conveying process for different powder types and particle sizes. This ensures consistent material transfer rates and minimizes the risk of blockages or material degradation.
- Integrated Material Level Monitoring: The feeding station includes sensors and indicators to monitor the material level in the tote bag and the conveying line. This helps in preventing overfilling or underfilling, ensuring efficient use of the bulk material and reducing waste.
- Easy Maintenance and Cleaning: The design of the equipment facilitates regular maintenance and cleaning, which is crucial for maintaining hygiene standards, especially in food and pharmaceutical applications. The components are constructed from materials that are resistant to corrosion and easy to disassemble for cleaning.
- Compatibility with Various Tote Bag Sizes: The system is designed to accommodate different sizes of tote bags, making it versatile for handling a wide range of bulk materials. This flexibility allows users to adapt the equipment to their specific operational needs without the need for significant modifications.
Benefits of Using Tote Bag Dust-Free Feeding Station
The adoption of the tote bag dust-free feeding station by industries such as food processing, pharmaceutical manufacturing, and chemical production offers several significant benefits. These benefits stem from the equipment's ability to enhance operational efficiency, improve product quality, and ensure compliance with regulatory standards. The key advantages include: