

Polycarbonate Conveying Systems: An Overview and the Advantages of Pneumatic Conveying with Polycarb
Polycarbonate conveying systems represent a sophisticated solution in material handling, particularly for industries requiring efficient, reliable, and low-maintenance transport of various powders and granules. These systems are engineered to deliver optimal performance while ensuring durability and safety. As a key component in modern industrial operations, polycarbonate conveyors are designed to handle a wide range of materials, from fine powders to bulk granules, with precision and efficiency.
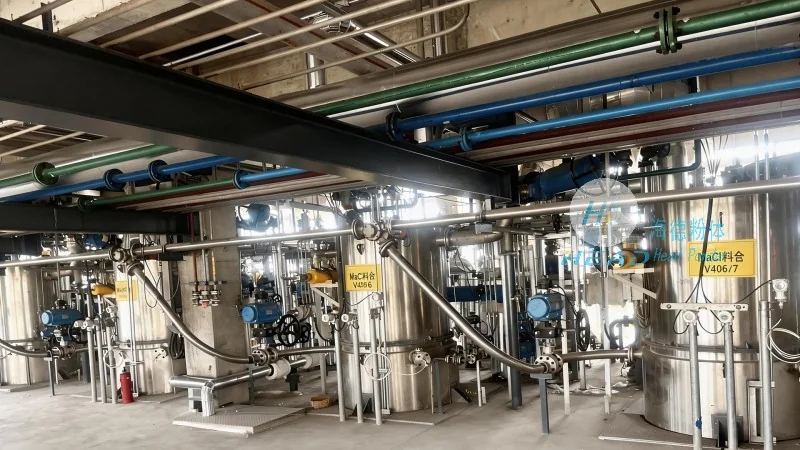
Key Features and Advantages of Polycarbonate Pneumatic Conveying
One of the primary advantages of polycarbonate pneumatic conveying is its exceptional resistance to chemical corrosion and impact. Polycarbonate, a thermoplastic polymer, offers superior strength-to-weight ratios, making it ideal for applications where traditional materials like metal or plastic may not be suitable. This material’s ability to withstand harsh environments, including exposure to acids, bases, and solvents, makes it a preferred choice for industries such as pharmaceuticals, food processing, and chemical manufacturing. Additionally, polycarbonate’s transparency allows for visual monitoring of the conveying process, enhancing operational oversight and reducing downtime.
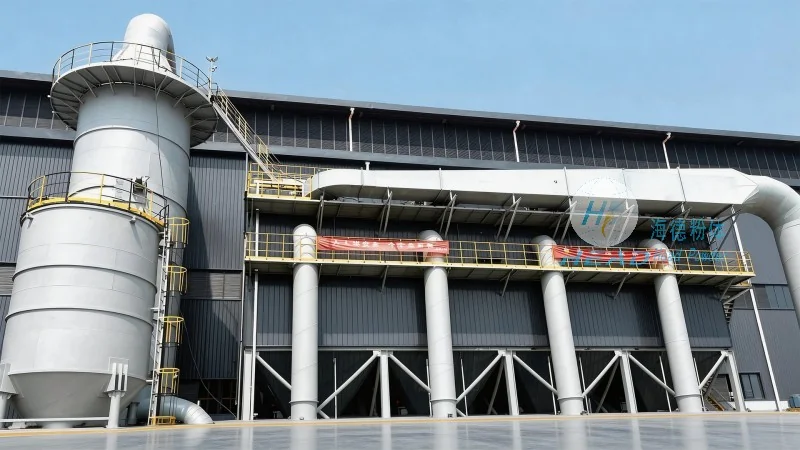
How Polycarbonate Conveying Systems Enhance Operational Efficiency
The design of polycarbonate conveying systems focuses on minimizing friction and wear, which directly contributes to lower maintenance costs and extended service life. Unlike metal or rigid plastic systems, polycarbonate components are less prone to abrasion, ensuring consistent performance over extended periods. This durability is further enhanced by the material’s self-lubricating properties, which reduce the need for frequent maintenance or replacement of parts. Moreover, the lightweight nature of polycarbonate reduces the overall load on the system, allowing for more compact installations and easier integration into existing production lines.
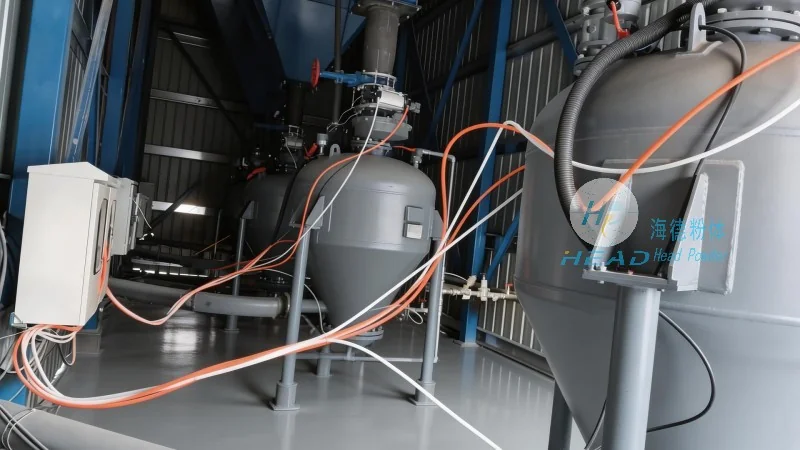
Applications in Diverse Industrial Sectors
Polycarbonate conveying systems are versatile and find applications across multiple industries. In the pharmaceutical sector, these systems are used to transport sensitive powders and granules, ensuring contamination-free handling and compliance with stringent regulatory standards. The food processing industry benefits from polycarbonate’s food-grade certification, making it suitable for conveying ingredients like spices, flour, and other food additives. Similarly, in the chemical industry, polycarbonate’s resistance to corrosive substances allows for the safe handling of hazardous materials, reducing the risk of equipment failure or environmental contamination. These systems also excel in the cosmetics and personal care industries, where the need for hygienic and non-reactive materials is paramount.
Customization and Integration Capabilities
Shandong HeadPowder Engineering Co., Ltd. specializes in providing tailored polycarbonate conveying solutions to meet the specific needs of clients. The company’s expertise lies in designing systems that integrate seamlessly with existing production workflows, ensuring minimal disruption during implementation. Customization options include varying tube diameters, lengths, and the inclusion of additional features such as filters, cyclones, or vacuum pumps, depending on the material being conveyed and the operational requirements. The engineering team at HeadPowder works closely with clients to assess their unique challenges and develop solutions that optimize efficiency, reduce costs, and enhance overall productivity.

Quality Assurance and Reliability
At Shandong HeadPowder Engineering Co., Ltd., quality is a core principle. The company adheres to strict manufacturing standards to ensure that each polycarbonate conveying system meets or exceeds industry benchmarks. Rigorous testing procedures are conducted to verify the system’s performance under various conditions, including pressure, temperature, and material flow rates. This commitment to quality ensures that clients receive reliable, long-lasting equipment that delivers consistent results. The company’s focus on durability and performance has earned it a reputation for delivering high-quality solutions that stand the test of time.