

Analysis of Color Masterbatch Pneumatic Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced pneumatic conveying systems designed for the efficient handling of color masterbatch granules. This article provides a detailed analysis of such systems, focusing on their design, functionality, and practical applications in industrial settings.
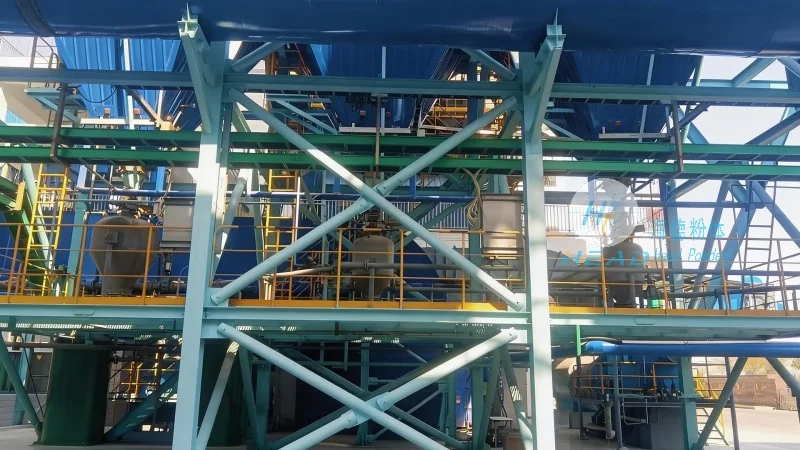
Understanding Pneumatic Conveying for Color Masterbatch Granules
Pneumatic conveying systems are essential for transporting color masterbatch granules, which are crucial additives used in plastic manufacturing to impart specific colors and properties to end products. These systems utilize air or other gases to move granules through pipelines, offering a clean, efficient, and cost-effective solution compared to traditional mechanical conveying methods. The core components of a typical pneumatic conveying system include a hopper for material storage, a blower or compressor to generate airflow, a pipeline network to transport the material, and a receiver or discharge unit for material collection.
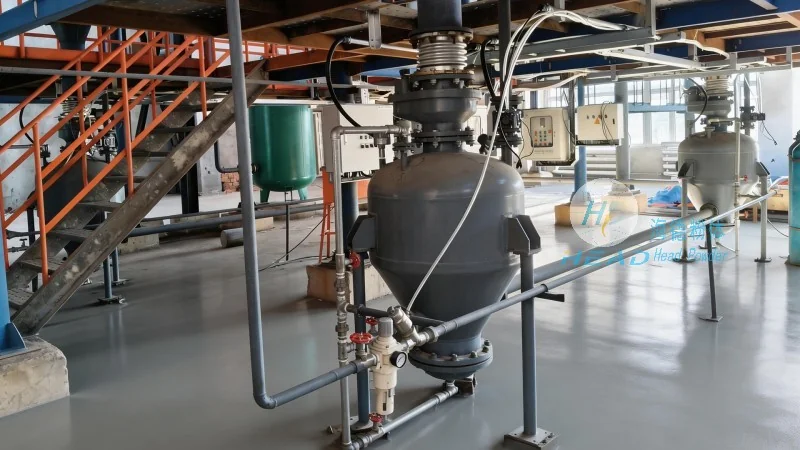
Key Features of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems are engineered with precision to meet the demanding requirements of color masterbatch handling. Key features include adjustable airflow control to optimize material transport speed, robust hopper designs to prevent material degradation and blockages, and high-efficiency filtration systems to maintain air quality and prevent dust contamination. The systems are also designed for easy integration into existing production lines, with modular components that allow for scalability and customization based on specific customer needs.
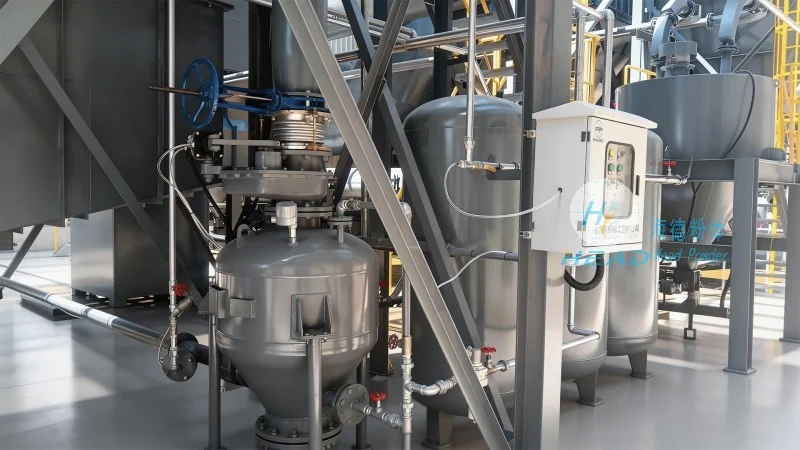
Benefits of Using Pneumatic Conveying for Color Masterbatch Handling
Implementing pneumatic conveying systems for color masterbatch granules offers numerous advantages. Firstly, it significantly reduces material handling time and labor costs by automating the transport process. Secondly, the systems minimize product contamination and degradation, ensuring consistent quality of the color masterbatch. Thirdly, they provide a clean and hygienic operation environment, which is critical in food-grade and pharmaceutical applications where material purity is paramount. Additionally, pneumatic conveying systems are energy-efficient and can handle a wide range of material densities and flow rates, making them versatile for various industrial applications.
Application Scenarios and Performance Metrics
The effectiveness of a pneumatic conveying system for color masterbatch granules is often evaluated based on several performance metrics, including conveying capacity, pressure drop, and material recovery rate. HeadPowder's systems are designed to achieve high conveying capacities, typically ranging from several hundred to several thousand kilograms per hour, depending on the system configuration. The pressure drop across the pipeline is minimized through optimized pipe sizing and the use of smooth, low-friction materials, ensuring efficient energy use. Material recovery rates are consistently high, with minimal loss due to system inefficiencies, which is crucial for maintaining material inventory accuracy and reducing waste.
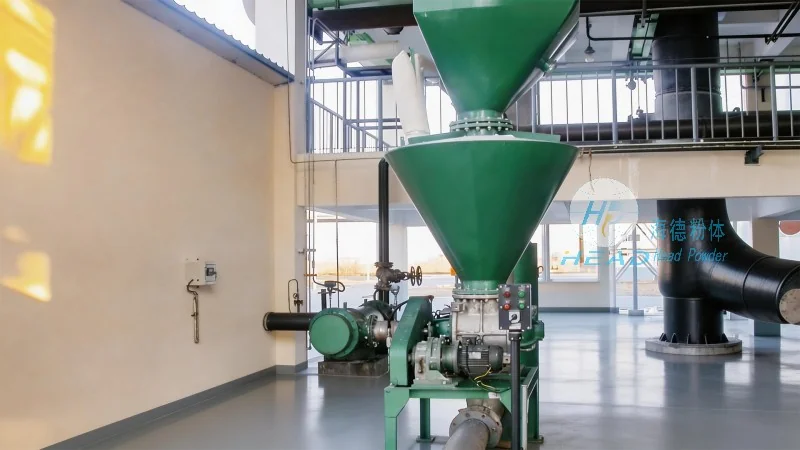
Customization and After-Sales Support from HeadPowder
HeadPowder understands that each industrial application has unique requirements, and therefore, offers comprehensive customization options for its pneumatic conveying systems. This includes adjustments to hopper size, pipeline length and diameter, and control system interfaces to integrate seamlessly with existing production equipment. The company also provides robust after-sales support, including installation assistance, routine maintenance services, and technical support to ensure the system operates at peak efficiency throughout its service life. With a focus on customer satisfaction and long-term partnership, HeadPowder ensures that its clients receive reliable and durable solutions tailored to their specific needs.