

Detailed Explanation of Corn Starch Pneumatic Conveying Systems
For industrial operations dealing with corn starch, efficient material handling is crucial to maintain production flow and product quality. A pneumatic conveying system offers a reliable solution for transporting corn starch from storage to processing units, ensuring minimal dust generation and contamination risks. This article provides an in-depth look at the components, working principles, and benefits of such systems, tailored for applications in the corn starch industry.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in designing and manufacturing customized pneumatic conveying solutions. With years of experience in the field, the company understands the unique challenges faced by corn starch producers, such as handling fine powders and maintaining consistent moisture levels. Their systems are engineered to meet stringent industry standards, ensuring durability and long-term performance.
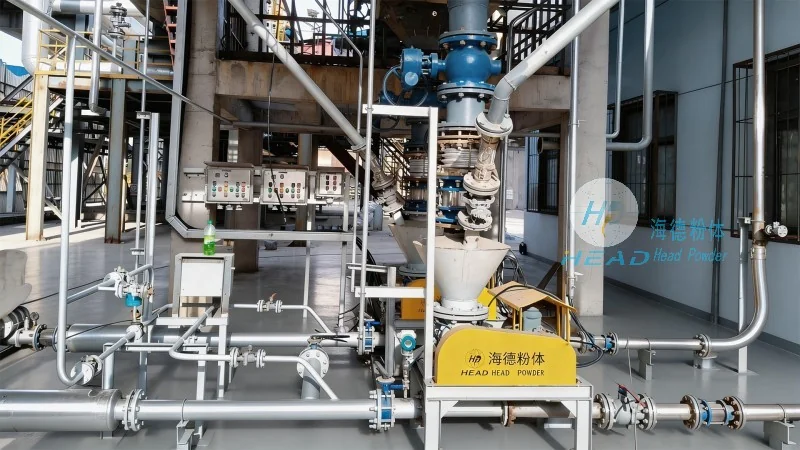
The core of a corn starch pneumatic conveying system consists of several key components. The primary elements include a hopper for material storage, a rotary airlock valve to control the flow of starch into the system, a conveying pipeline, and a receiver for the final product. The system operates by using compressed air to create a flow of air and starch particles, moving the material through the pipeline under pressure. This method eliminates the need for mechanical conveyors, reducing wear and tear on equipment and minimizing the risk of product contamination.
One of the most significant advantages of pneumatic conveying for corn starch is its ability to handle fine powders without clogging. Unlike screw or belt conveyors, which can easily become obstructed by small particles, pneumatic systems use air to keep the material in suspension, preventing blockages and ensuring smooth operation. This is particularly important for corn starch, which is often processed into fine powders for various applications, including food, pharmaceuticals, and industrial chemicals.
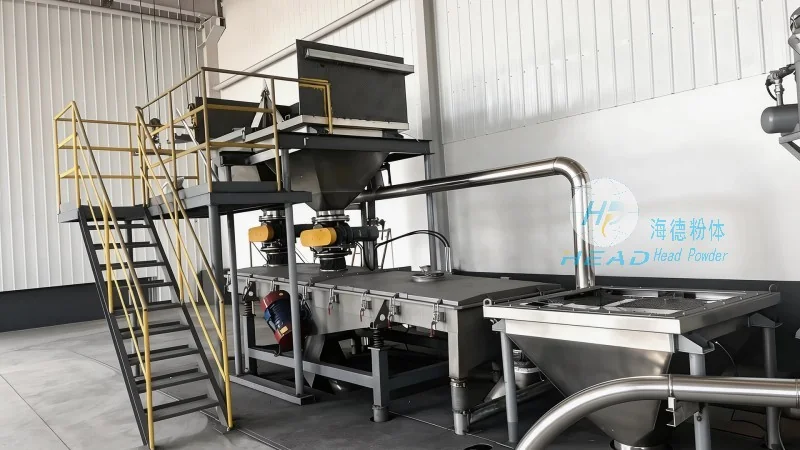
Another key benefit is the reduction in dust and airborne contamination. Traditional bulk handling methods often generate significant dust, which can pose health risks to workers and affect product purity. Pneumatic conveying systems, especially those with enclosed pipelines and proper filtration, minimize dust emissions, creating a safer working environment and maintaining the integrity of the corn starch product.
HeadPowder’s engineers design systems that are tailored to the specific needs of each corn starch facility. They consider factors such as the volume of starch to be conveyed, the distance between storage and processing areas, and the required flow rate. By analyzing these parameters, the company can recommend the most efficient system configuration, whether it’s a pressure or vacuum system, and select appropriate components like air compressors, filters, and control valves.
For example, a typical corn starch pneumatic conveying system might include a large storage hopper with a capacity of several tons, equipped with a rotary airlock valve to regulate the flow of starch into the pipeline. The pipeline, made of corrosion-resistant materials like stainless steel, is designed to handle the abrasive nature of starch particles. At the receiving end, a receiver with a dust collection system ensures that any fine particles are captured and returned to the process, preventing loss and maintaining product quality.

The system’s control panel allows operators to monitor and adjust the conveying process in real-time. Sensors are used to detect flow rates, pressure levels, and any potential blockages, providing immediate feedback to the control system. This automation enhances operational efficiency and reduces the need for manual intervention, minimizing downtime and ensuring consistent production output.
HeadPowder’s commitment to quality and customer satisfaction is evident in their product design and after-sales support. The company provides comprehensive technical support, including installation, commissioning, and maintenance services, ensuring that the pneumatic conveying system operates at peak performance throughout its lifespan. With a strong presence in Shandong, China, HeadPowder serves a wide range of clients in the corn starch industry, helping them optimize their material handling processes and improve overall productivity.
In conclusion, a corn starch pneumatic conveying system is a vital asset for any corn starch production facility. By leveraging the power of compressed air to transport fine powders efficiently and safely, these systems enhance operational efficiency, reduce contamination risks, and improve product quality. HeadPowder’s expertise in designing and manufacturing customized solutions ensures that corn starch producers can achieve optimal performance and meet their production goals with reliability and precision.