

Principle and Working Scene Characteristics of Potash Fertilizer Material Handling System Equipment
For agricultural operations that rely on efficient and reliable material handling, the potash fertilizer material handling system stands out as a critical component in modern fertilizer production and distribution. This system is designed to manage the transport, storage, and processing of potash fertilizer, ensuring that the material is handled safely and effectively from the production stage to the final delivery point. The technology behind these systems combines advanced engineering principles with practical application, making them essential for optimizing workflow in fertilizer manufacturing facilities.
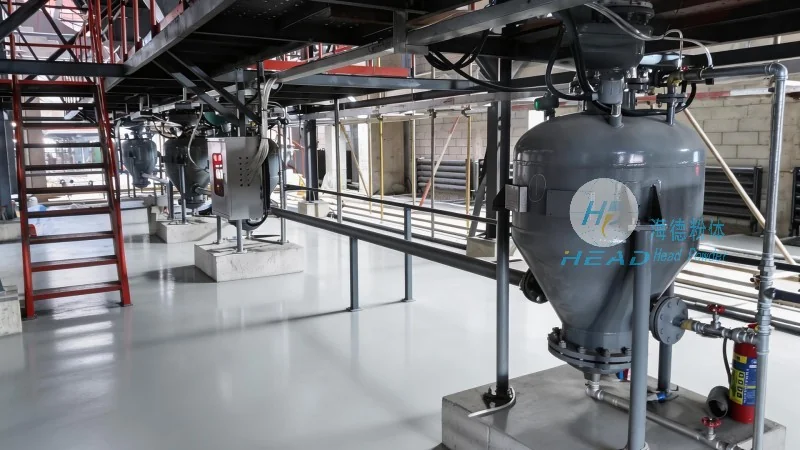
Core Principles of the Potash Fertilizer Material Handling System
The fundamental principle of the potash fertilizer material handling system revolves around the efficient movement of bulk materials. Key components include conveyor belts, bucket elevators, and pneumatic conveying systems, each tailored to handle the specific characteristics of potash fertilizer—such as its granular or crystalline structure, moisture content, and density. The system is engineered to minimize material degradation, prevent dust generation, and maintain consistent flow rates, which are critical for maintaining product quality and operational efficiency. By integrating these components, the system ensures that potash fertilizer is transported with minimal loss and maximum safety, aligning with industry standards for bulk material handling.
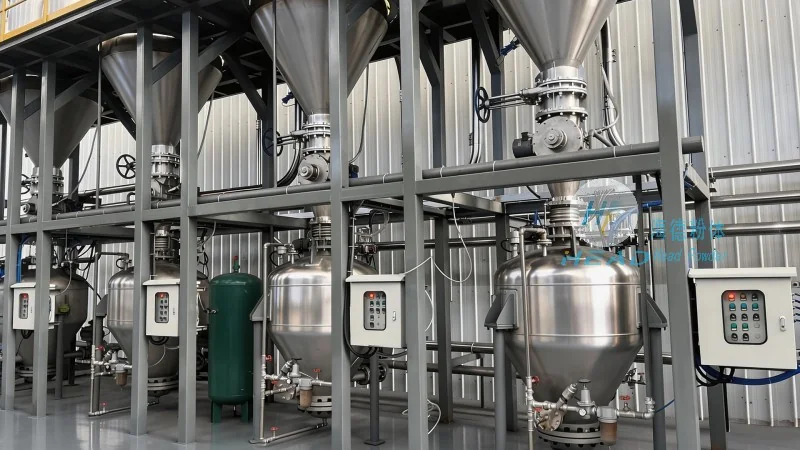
Working Scene Characteristics and Application Scenarios
The working scene characteristics of the potash fertilizer material handling system are shaped by the diverse environments in which it operates. In industrial fertilizer plants, the system is typically integrated into a larger production line, where it connects raw material storage to processing equipment and then to packaging or loading areas. The system’s design accommodates high-volume throughput, often handling thousands of tons of potash fertilizer per day, making it suitable for large-scale agricultural operations. Additionally, the system is adaptable to different operational conditions, including indoor and outdoor settings, and can be customized to fit the specific layout and requirements of a facility. This flexibility allows the system to be deployed in various stages of the fertilizer supply chain, from raw material handling to finished product distribution, ensuring seamless integration with existing infrastructure.
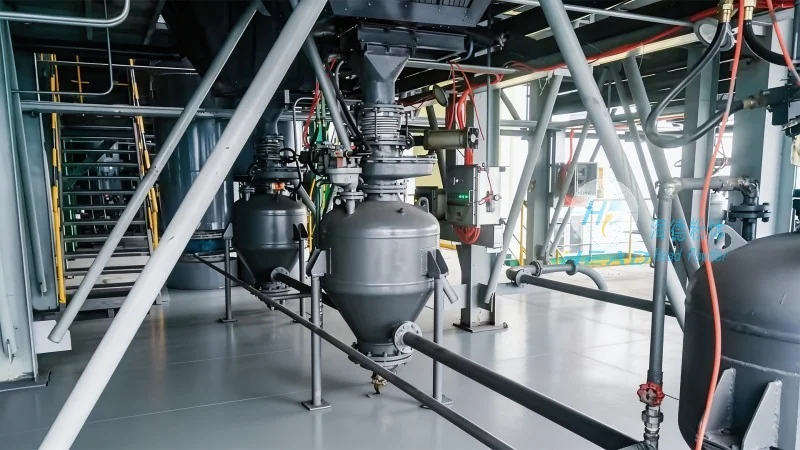
Key Features and Technical Advantages
Headpowder, a leading manufacturer of material handling solutions, offers advanced potash fertilizer material handling systems that incorporate several key features to enhance performance and reliability. The systems are equipped with high-capacity conveyor belts that can handle heavy loads without compromising speed or efficiency. Bucket elevators are designed with durable materials to withstand the abrasive nature of potash fertilizer, reducing wear and tear over time. Pneumatic conveying systems provide a dust-free and low-maintenance option for transporting fine or powdery potash fertilizer, minimizing the risk of contamination and improving workplace safety. Furthermore, the systems are equipped with advanced control systems that allow for real-time monitoring and adjustment of operational parameters, ensuring optimal performance under varying conditions. These features collectively contribute to the system’s ability to maintain consistent product quality, reduce downtime, and lower operational costs for users.
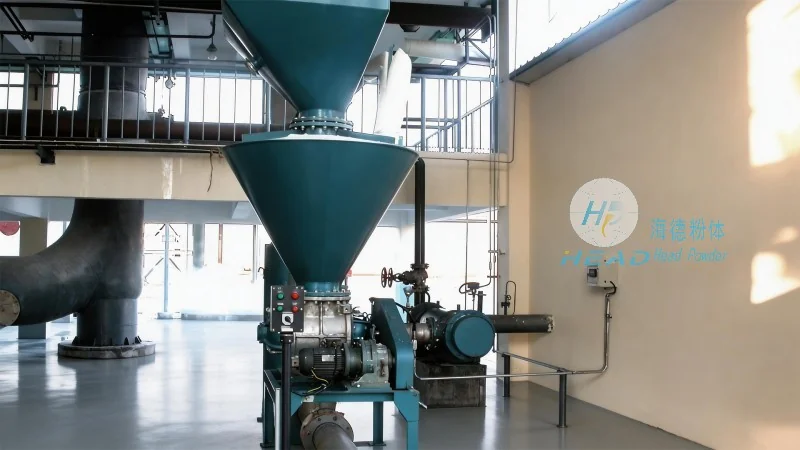
Company Profile and Service Commitment
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable company specializing in the design, manufacturing, and installation of material handling systems for the fertilizer industry. With years of experience in the field, Headpowder has developed a strong reputation for delivering high-quality, reliable solutions that meet the unique needs of its clients. The company’s commitment to innovation and customer satisfaction is reflected in its product development and after-sales support services. By leveraging advanced engineering and manufacturing capabilities, Headpowder ensures that its potash fertilizer material handling systems are built to withstand the demands of industrial operations while providing long-term value to its customers. The company’s team of experts works closely with clients to understand their specific requirements and provide tailored solutions that enhance operational efficiency and product quality.