

Principle and Working Scene Characteristics of Heavy Powder Material Conveying System Equipment
Heavy powder material conveying systems are critical components in industrial processes, designed to transport bulk materials such as powders, granules, and fine particles efficiently and reliably. These systems play a vital role in various industries, including chemical, pharmaceutical, food processing, and mining, where the handling of heavy powders is essential for production continuity and operational efficiency. The design and functionality of these systems are tailored to meet the specific demands of different applications, ensuring optimal performance under diverse operational conditions.
Working Principle of Heavy Powder Material Conveying Equipment
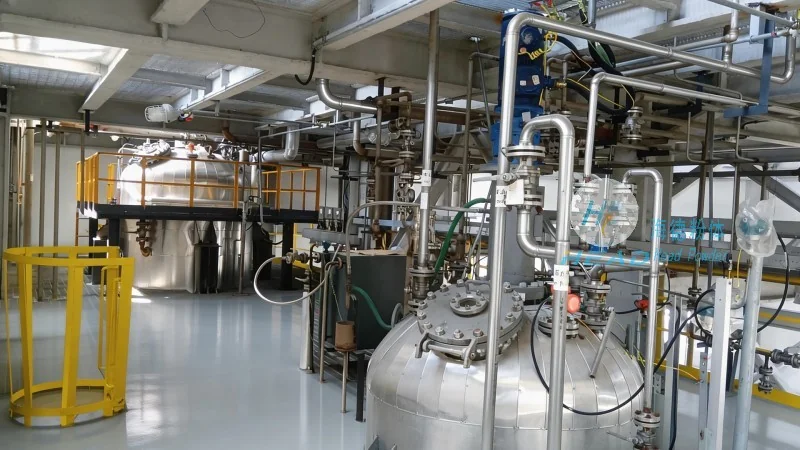
The core principle of heavy powder material conveying systems involves the use of mechanical components to move bulk materials from one location to another. Key components typically include feeders, conveyors, and control systems, each working in tandem to ensure smooth material flow. The system operates by first feeding the material into the conveyor, where it is then transported through a series of mechanisms such as screw conveyors, belt conveyors, or pneumatic systems. The choice of conveyor type depends on factors like material properties, required throughput, and space constraints. For instance, screw conveyors are ideal for handling dry, free-flowing powders, while pneumatic conveyors are suitable for fine powders that require dust control and precise delivery. The control system monitors and adjusts the conveying speed and pressure to maintain consistent material flow, preventing blockages and ensuring the system operates within safe parameters.
Typical Working Scene Characteristics
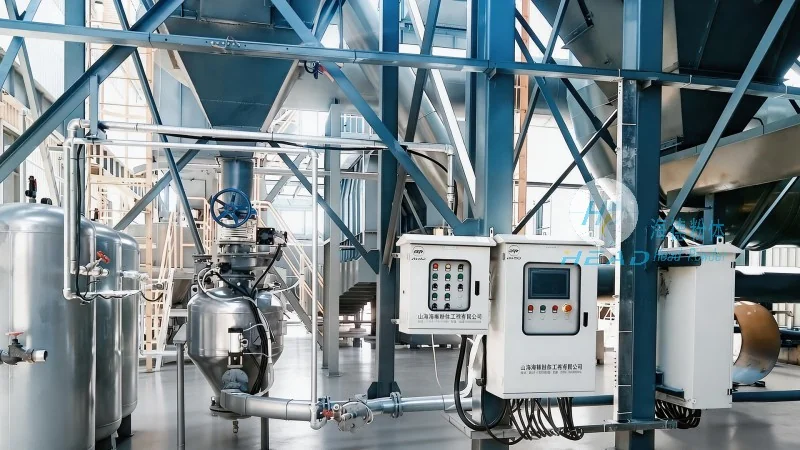
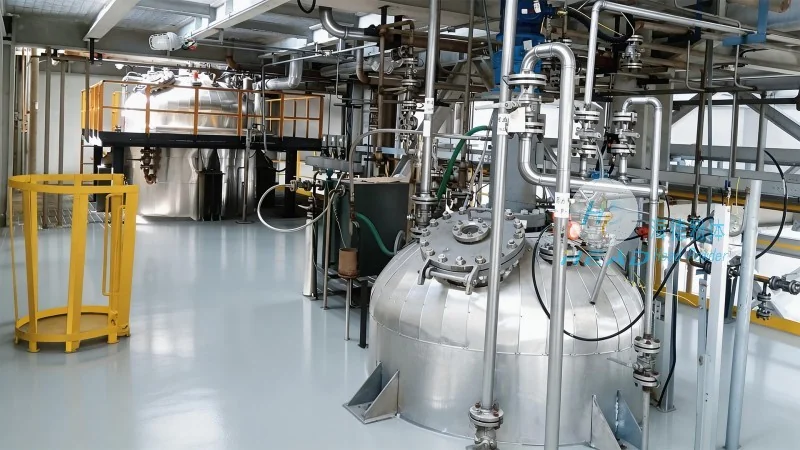
The working scene characteristics of heavy powder material conveying systems vary based on the industry and application. In chemical manufacturing, for example, these systems are often used in environments with strict safety and hygiene standards, requiring dust-proof and explosion-proof designs. The systems may be integrated with other production equipment, such as mixers and reactors, to form a continuous production line. In the pharmaceutical industry, the conveying systems must adhere to GMP (Good Manufacturing Practice) guidelines, ensuring that the materials are handled in a sterile and controlled manner. The working scenes may also involve high-volume production, where the system needs to handle large quantities of material quickly and efficiently. Additionally, the systems may operate in harsh environments, such as mining or construction sites, where durability and resistance to wear and tear are crucial. The characteristics of the working scene, including temperature, humidity, and material properties, directly influence the selection of the appropriate conveying equipment and its maintenance requirements.
Application Advantages and Performance Metrics
Heavy powder material conveying systems offer several advantages in industrial applications. One of the primary benefits is the ability to handle large volumes of material with minimal labor, reducing operational costs and increasing productivity. The systems are also designed to minimize material degradation, ensuring that the quality of the powder is maintained throughout the conveying process. Another advantage is the flexibility in system design, allowing customization to meet specific production needs. Performance metrics, such as throughput capacity, energy efficiency, and system reliability, are critical factors in evaluating the effectiveness of these systems. For instance, a well-designed system may achieve a high throughput while consuming low energy, making it cost-effective and environmentally friendly. The reliability of the system, measured by its uptime and maintenance frequency, is also an important consideration, as downtime can significantly impact production schedules and profitability.
Conclusion and Company Profile
Heavy powder material conveying systems are essential for efficient material handling in various industrial sectors. The principles and working scene characteristics of these systems are tailored to meet the specific requirements of different applications, ensuring optimal performance and reliability. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying systems that meet the diverse needs of its clients. With a focus on innovation and customer satisfaction, the company offers customized solutions that enhance operational efficiency and reduce costs. HeadPowder's systems are built with durability and performance in mind, ensuring long-term reliability and minimal maintenance. Based in Shandong, China, the company leverages its expertise and local resources to deliver top-tier products and services to industries worldwide. By understanding the unique challenges of each application, HeadPowder provides tailored solutions that help businesses achieve their production goals while maintaining safety and efficiency.