

Principle and Working Scene Characteristics of Small Stone Powder Conveying Equipment
Small stone powder conveying equipment, as a specialized device in the field of powder material handling, plays a crucial role in the efficient transportation of small stone powders. This equipment is designed to meet the needs of various industrial applications, ensuring the stable and reliable movement of powders from the source to the destination. The core of this equipment lies in its ability to handle fine powders with small stone particles, which often presents challenges in traditional conveying methods due to issues like dust generation, blockage, and material loss. By leveraging advanced engineering principles, the equipment addresses these challenges through optimized design and operational mechanisms.
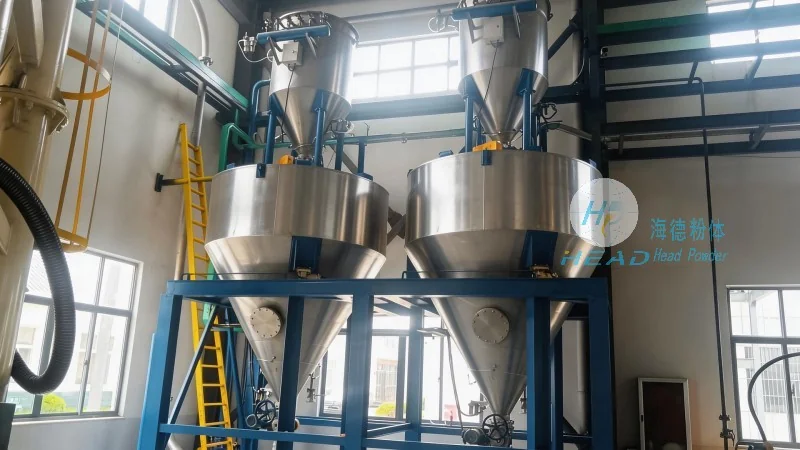
Principle of Operation for Small Stone Powder Conveying Equipment
The working principle of small stone powder conveying equipment is based on the combination of air pressure and mechanical force. The system typically consists of a feeding hopper, a conveying pipeline, a drive unit, and a control system. The process begins with the material being fed into the hopper, where it is then transported through the pipeline by the force of compressed air or a vacuum system. The drive unit, often an electric motor coupled with a fan or blower, generates the necessary airflow to move the powder particles. The control system monitors and adjusts the airflow and pressure to maintain optimal conveying efficiency. This principle ensures that the small stone powders are conveyed without significant degradation or loss, maintaining the integrity of the material throughout the process.
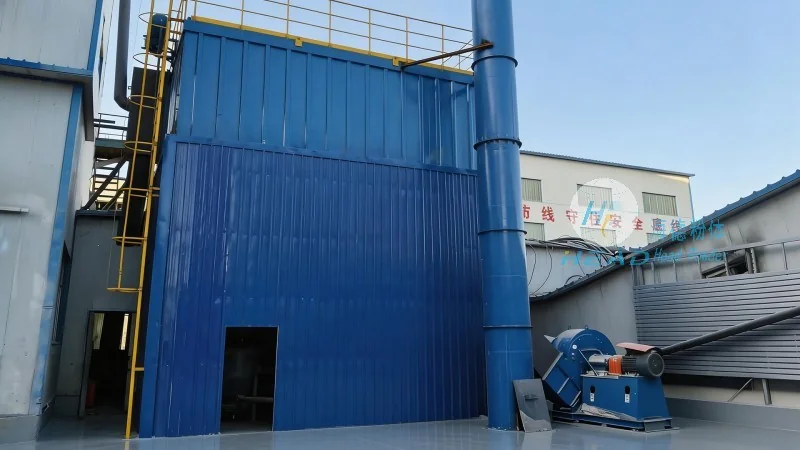
Key Components and Their Functions
Several key components contribute to the effective operation of small stone powder conveying equipment. The feeding hopper is responsible for storing and feeding the material into the system, ensuring a consistent flow rate. The conveying pipeline, usually made of durable materials like stainless steel or plastic, is designed to withstand the abrasive nature of small stone powders and prevent material buildup. The drive unit, which includes the fan or blower, provides the necessary air pressure to move the powder. The control system, equipped with sensors and valves, regulates the airflow and pressure to adapt to varying material conditions and conveying demands. Each component works in harmony to ensure the smooth and efficient operation of the entire system.
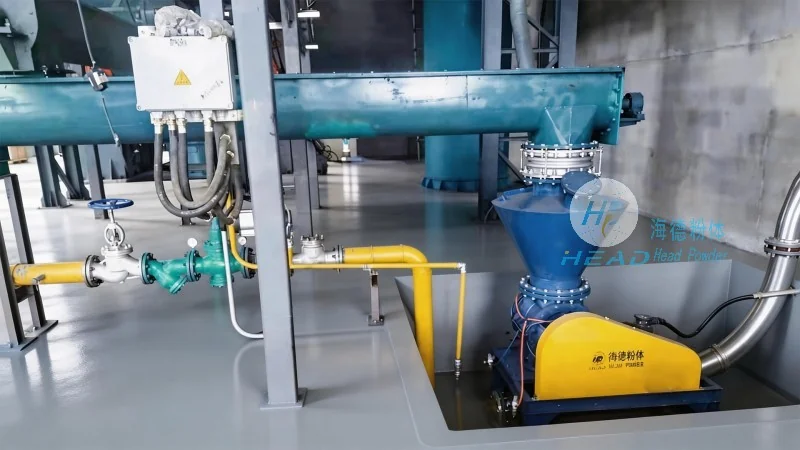
Working Scene Characteristics and Applications
Small stone powder conveying equipment is widely used in various industrial scenarios, including mining, construction, and chemical processing. In mining operations, it is used to transport crushed stone powders from processing plants to storage facilities or for further processing. In construction, it helps in the efficient delivery of cement and other fine powders to construction sites, improving workflow and reducing manual handling. The equipment is also applied in chemical plants for conveying raw materials like limestone powders, which are essential for various chemical reactions. The working scene characteristics include high material throughput, low energy consumption, and minimal dust emission, making it suitable for both indoor and outdoor applications. The adaptability of the equipment to different material types and operational conditions makes it a versatile solution for powder handling needs.
Advantages and Benefits of Using Small Stone Powder Conveying Equipment
Implementing small stone powder conveying equipment offers several advantages over traditional conveying methods. One of the primary benefits is the reduction in labor costs, as the equipment automates the material handling process, minimizing the need for manual labor. It also enhances safety by reducing exposure to dust and preventing material spills, which can lead to accidents or environmental contamination. The equipment is designed for high efficiency, with lower energy consumption compared to other methods like bucket elevators or belt conveyors. This results in cost savings over time and a more sustainable operation. Additionally, the equipment provides consistent material flow, ensuring that downstream processes receive a steady supply of material, which improves overall production efficiency. The durability of the components and the ease of maintenance further contribute to the long-term benefits of using this equipment.
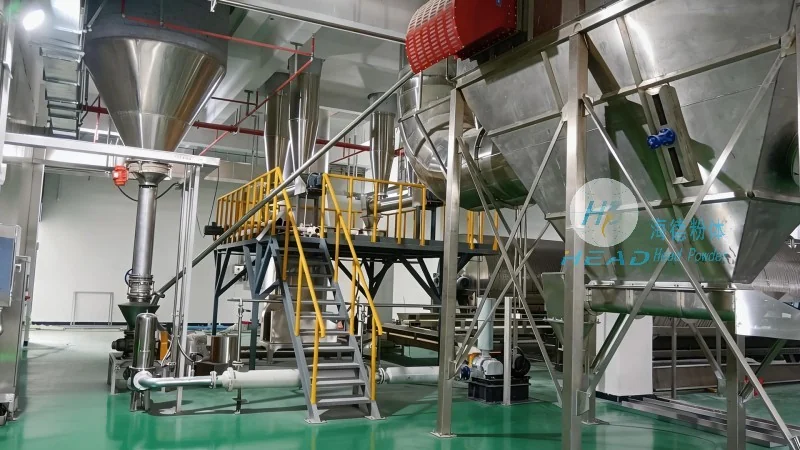
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design, development, and production of advanced powder conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's products are engineered to meet the specific needs of various industries, ensuring reliability and efficiency in powder handling applications. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with modern technology and skilled workforce. HeadPowder adheres to strict quality control standards, ensuring that each product meets international specifications and customer requirements. The company's commitment to customer satisfaction and technological advancement has enabled it to serve a wide range of clients globally, providing tailored solutions for their powder conveying needs.