

Principle and Working Scene Characteristics of Automatic Tote Bag Feeding Powder Material Conveying
For industries that handle bulk powders, the efficient and reliable transfer of material from storage containers to processing lines is critical. The automatic tote bag feeding system, a product of Shandong HeadPowder Engineering Co., Ltd. (headpowder), addresses these needs by integrating advanced technology with practical application. This equipment is engineered to streamline the process of feeding powders from tote bags into downstream equipment, ensuring consistent flow and minimizing downtime. HeadPowder, based in Shandong, China, specializes in developing solutions for efficient powder handling, and this system is a prime example of their commitment to quality and innovation.
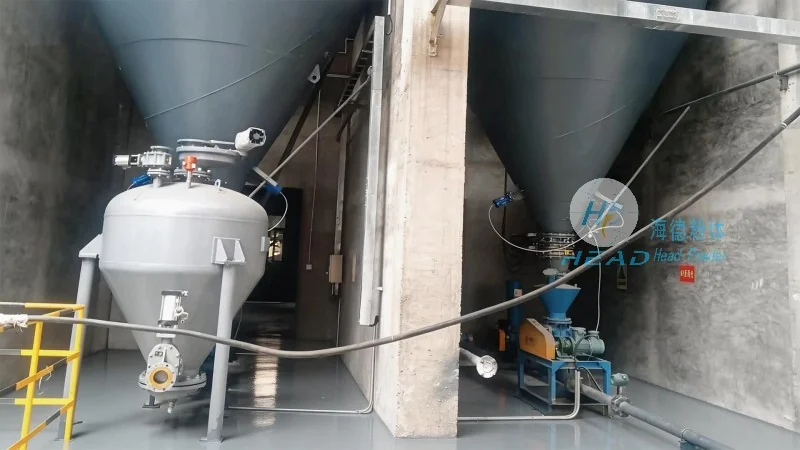
Core Principle of the Automatic Tote Bag Feeding System
The fundamental principle of the automatic tote bag feeding system involves a combination of mechanical and pneumatic components that work in tandem to extract powder from a tote bag and deliver it to the processing equipment. The system typically includes a hopper or receiving chamber that is connected to the tote bag via a sealing mechanism. As the powder is discharged from the tote bag, it is drawn into the hopper under controlled pressure, preventing dust and maintaining a clean transfer process. The design incorporates features such as a level sensor and a flow control valve to regulate the amount of material being fed, ensuring precise dosing and preventing overfilling or underfilling. This principle is crucial for maintaining product quality and operational efficiency in powder handling applications.
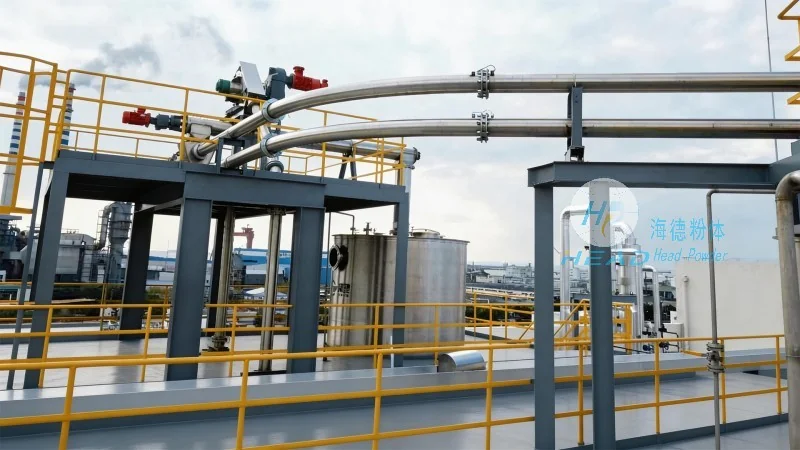
Key Working Scene Characteristics
The working scene characteristics of the automatic tote bag feeding system are tailored to meet the demands of various industrial environments. One key characteristic is its adaptability to different powder types, including fine powders, granules, and bulk materials. The system’s design allows for easy integration with existing processing lines, making it suitable for both new installations and retrofit applications. Another important characteristic is the system’s ability to handle large volumes of material, with some models capable of processing up to several tons per hour. This makes it ideal for high-throughput operations in sectors such as pharmaceuticals, food processing, and chemical manufacturing. Additionally, the system is designed for minimal maintenance, with easy access to components for cleaning and replacement, reducing operational costs and ensuring long-term reliability. The working scene also emphasizes safety features, such as dust extraction and containment systems, which are essential for compliance with industrial safety regulations and environmental standards.
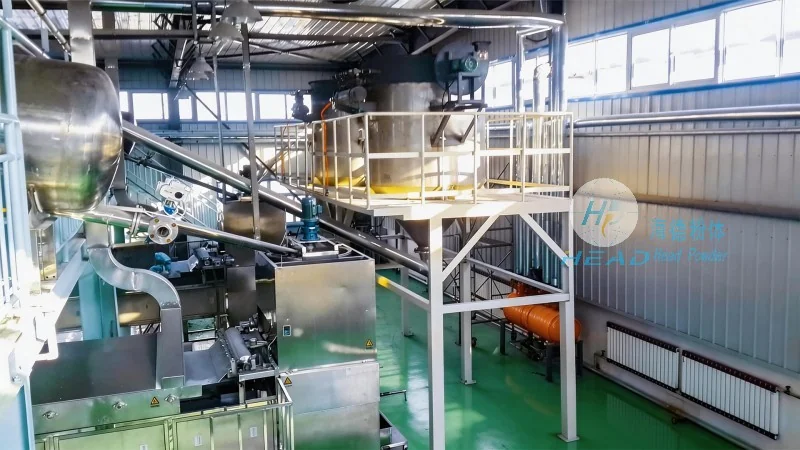
Benefits and Applications in Industrial Settings
The automatic tote bag feeding system offers several benefits that enhance operational performance in industrial settings. One primary benefit is the reduction of manual labor, as the system automates the process of feeding powders from tote bags, minimizing the risk of human error and improving consistency. This automation also leads to increased productivity, as the system can operate continuously without the need for constant monitoring. Another benefit is the improvement in product quality, as the controlled feeding process prevents agglomeration and ensures uniform material flow. This is particularly important in industries where product consistency is critical, such as in the production of pharmaceuticals or food products. The system also contributes to cost savings by reducing material waste and minimizing downtime due to equipment failures. In applications where space is limited, the compact design of the system allows for efficient use of available floor space, making it suitable for both large and small-scale operations. The versatility of the system makes it applicable across multiple industries, including chemical, pharmaceutical, food, and agricultural sectors, where bulk powder handling is a common requirement.