

Principle and Working Scene Characteristics of Calcium Hydroxide Pneumatic Conveyor
Calcium hydroxide, commonly known as slaked lime, is a widely used chemical in various industrial applications. The efficient and safe transportation of this material is crucial for industrial processes, and pneumatic conveyors have emerged as a preferred solution. This article explores the principle and working scene characteristics of a calcium hydroxide pneumatic conveyor, highlighting its operational efficiency and suitability for specific industrial environments.
Introduction to Calcium Hydroxide and Pneumatic Conveying
Calcium hydroxide is an inorganic compound with the chemical formula Ca(OH)₂. It is often used in industries such as construction, agriculture, and water treatment due to its alkaline properties and ability to neutralize acids. Traditional methods of transporting calcium hydroxide, like manual handling or bulk trucks, pose challenges related to dust exposure, material loss, and operational inefficiencies. Pneumatic conveyors offer a solution by using air pressure to move the material through a pipeline system, ensuring a clean, controlled, and efficient transfer process.
The Principle of Pneumatic Conveying for Calcium Hydroxide
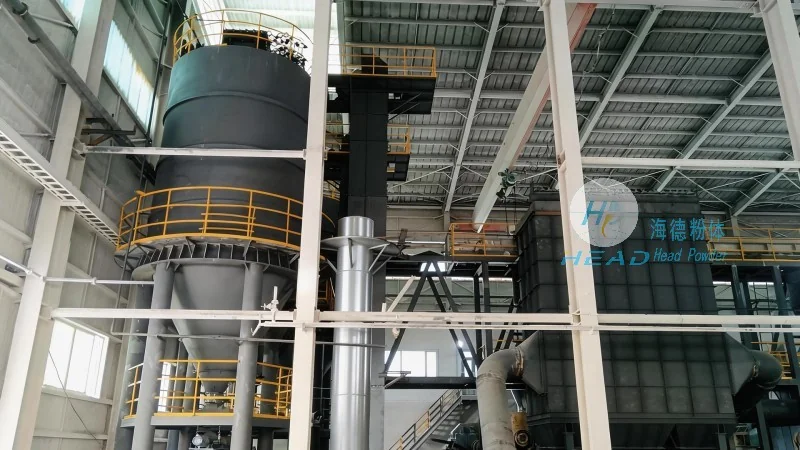
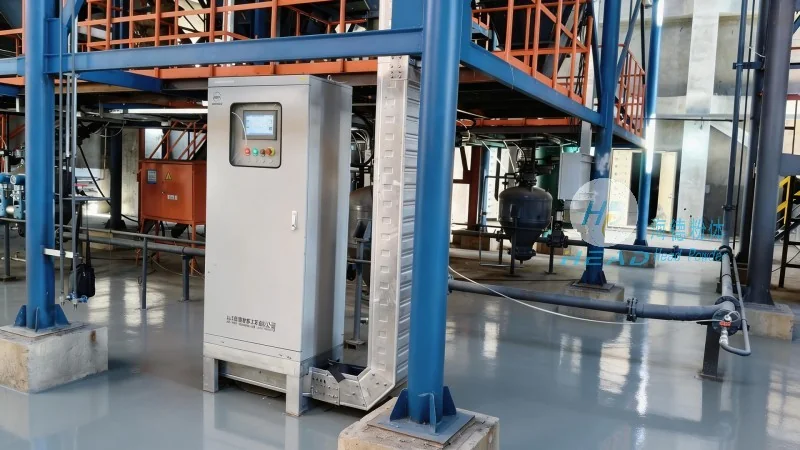
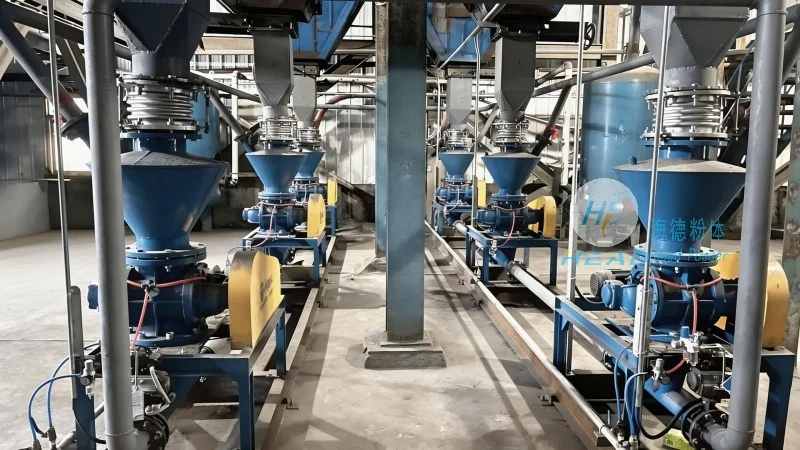
The core principle of a pneumatic conveyor for calcium hydroxide involves the use of compressed air to create a flow that transports the material. The system typically consists of a hopper, a blower or air compressor, a pipeline network, and a discharge point. As the material is introduced into the hopper, it is drawn into the pipeline by the air flow generated by the blower. The air pressure and velocity are carefully controlled to ensure the material is conveyed without degradation or blockage. This method allows for the continuous and automated movement of calcium hydroxide from the storage area to the processing or application points.
Key Working Scene Characteristics
The working scene characteristics of a calcium hydroxide pneumatic conveyor are tailored to meet the demands of industrial applications. These include:
- High Efficiency and Capacity: The system can handle large volumes of calcium hydroxide with minimal downtime, improving overall production throughput.
- Low Maintenance and Longevity: Pneumatic conveyors are designed for durability, with components that resist corrosion and wear from the material, ensuring long operational life.
- Safe and Clean Operation: By containing the material within a sealed pipeline, the conveyor reduces dust emissions and minimizes the risk of exposure to workers, enhancing workplace safety.
- Flexible Layout and Integration: The modular design of pneumatic conveyors allows for easy integration into existing industrial setups, with the ability to adjust the pipeline layout to suit different facility configurations.
Application Scenarios and Industrial Use Cases
The calcium hydroxide pneumatic conveyor is particularly suitable for industrial environments where precise and controlled material handling is essential. Common applications include:
- Construction Materials Production: In the production of lime-based products, such as lime mortar or lime plaster, the conveyor ensures a consistent supply of calcium hydroxide to the mixing and processing units.
- Agricultural and Fertilizer Industry: For the production of lime-based fertilizers or soil conditioners, the system efficiently transports the material to blending and packaging areas.
- Water Treatment Plants: In water treatment processes that require pH adjustment, the conveyor delivers calcium hydroxide to the treatment tanks, ensuring optimal chemical dosing.
- Industrial Manufacturing: Various manufacturing processes that utilize calcium hydroxide as a raw material benefit from the conveyor's ability to provide a steady and controlled feed.
Company Background: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in the design, development, and production of pneumatic conveyors tailored to specific industrial needs. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses requiring reliable and efficient material transportation solutions. HeadPowder's products are engineered to meet international standards and are widely used in various industrial sectors, including chemical processing, construction, and agriculture.
Conclusion
The calcium hydroxide pneumatic conveyor represents a significant advancement in material handling technology, offering enhanced efficiency, safety, and flexibility for industrial applications. By understanding its principle and working scene characteristics, industries can optimize their processes and improve overall operational performance. With the expertise and experience of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access high-quality pneumatic conveyor systems that meet their specific requirements and contribute to their long-term success.