

Working Principle and Features of Sintered Ash Material Pneumatic Conveyor
Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China, specializes in providing advanced industrial solutions, including innovative pneumatic conveying systems for sintered ash materials. This article examines the working principle and key characteristics of a sintered ash material pneumatic conveyor, highlighting its efficiency and practical applications in material handling processes.
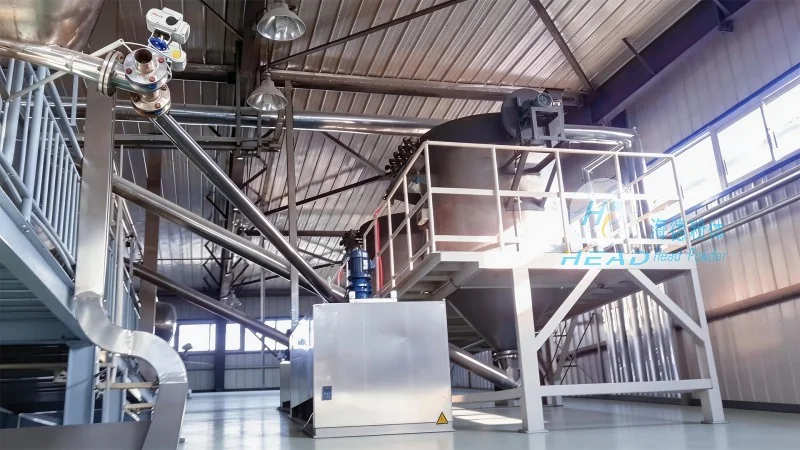
Overview of Sintered Ash Material Pneumatic Conveyor
A sintered ash material pneumatic conveyor is a specialized equipment designed to transport sintered ash, a byproduct commonly generated in industrial processes such as steel production and metallurgy. The system utilizes air as the primary medium to move the material from one location to another, offering a dust-free and efficient method compared to traditional mechanical conveying methods. This technology is particularly valuable in environments where dust control and material cleanliness are critical.
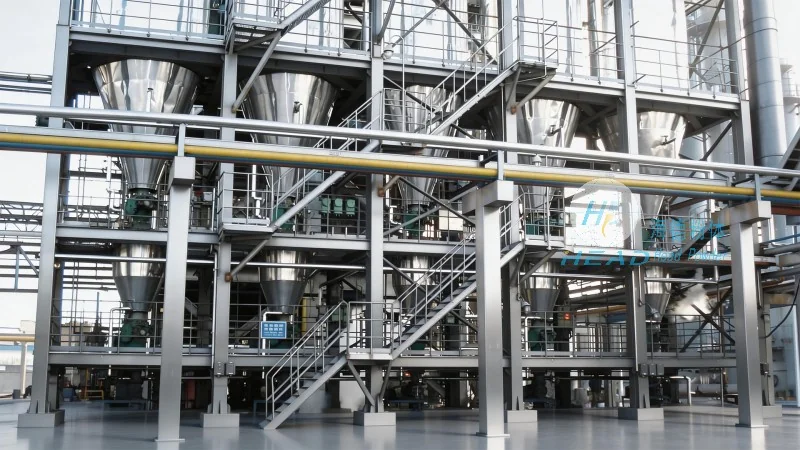
Working Principle of the Pneumatic Conveyor
The operation of a sintered ash material pneumatic conveyor is based on the fundamental principle of pneumatic transport, which involves the use of compressed air to create a flow that carries the material through a pipeline. The system typically consists of a feeding unit, a conveying pipeline, a separation or collection unit, and a control system. When the conveyor is activated, compressed air is introduced into the pipeline, creating a pressure differential that draws the sintered ash material into the system. The material is then carried along the pipeline by the air flow, with the air velocity maintained at a level sufficient to prevent material settling or blockage. At the destination point, the air is filtered and the material is separated from the air stream, often through a cyclone or other separation device. The separated material is then collected for further processing or disposal, while the clean air is discharged back into the environment.
Key Features and Technical Advantages
The sintered ash material pneumatic conveyor from Shandong HeadPowder Engineering Co., Ltd. offers several distinct features and advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free conveying process, which is crucial for maintaining air quality and preventing contamination in production environments. The system is also highly efficient in terms of energy consumption, as it minimizes material loss and reduces the need for manual handling. Additionally, the conveyor is designed for durability and reliability, with components that can withstand the abrasive nature of sintered ash and the demands of continuous operation. The system's modular design allows for easy installation and maintenance, reducing downtime and operational costs. Furthermore, the conveyor can be customized to meet specific process requirements, including varying material flow rates and pipeline lengths, ensuring optimal performance for different industrial settings.
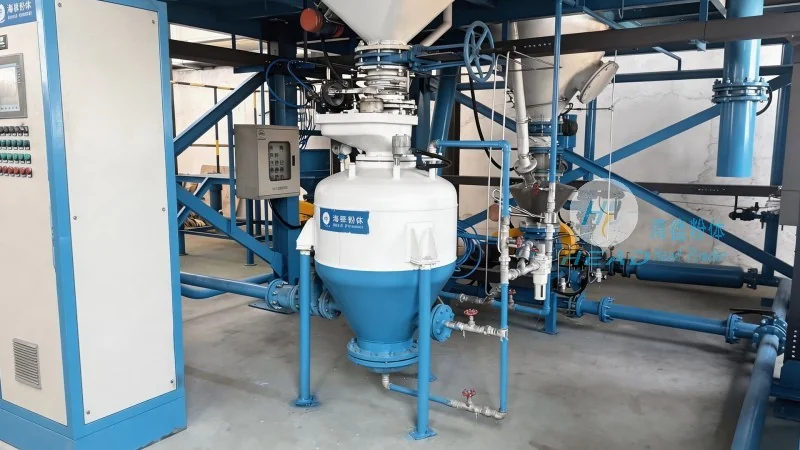
Application and Practical Use
Industrial facilities dealing with sintered ash, such as steel mills and metallurgical plants, benefit significantly from the use of a pneumatic conveyor. The system enables the safe and efficient transport of ash from storage areas to processing or disposal sites, improving overall operational efficiency. By eliminating the need for manual handling and reducing the risk of dust exposure, the conveyor enhances workplace safety and compliance with environmental regulations. The technology also contributes to cost savings by minimizing material waste and reducing the need for additional cleaning or maintenance procedures. In summary, the sintered ash material pneumatic conveyor from Shandong HeadPowder Engineering Co., Ltd. represents a reliable and effective solution for material handling in industrial applications, combining advanced technology with practical benefits for end-users.