

Working Principle and Features of Pneumatic Conveying Equipment for Carbon Black and Coal Powder Mat
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling carbon black and coal powder materials. These systems are engineered to efficiently transport fine powders over long distances with minimal loss and contamination, making them essential in various industrial applications such as chemical, pharmaceutical, and energy sectors.
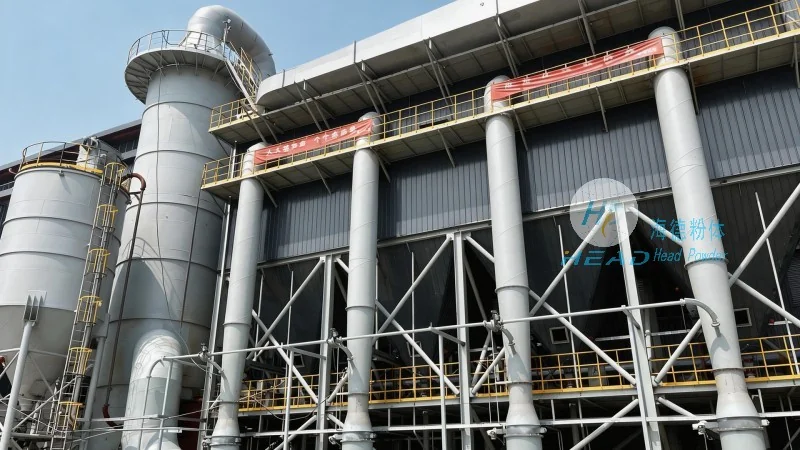
The core working principle of a pneumatic conveying system involves the use of air or gas to transport bulk materials through a pipeline network. There are primarily two types of pneumatic conveying systems: suction (or vacuum) systems and pressure systems. Suction systems operate by creating a negative pressure at the inlet to draw material from a hopper or storage silo into the pipeline. This method is ideal for applications requiring material to be moved from a lower elevation or over short distances, as it relies on the vacuum created by a fan or blower. In contrast, pressure systems use positive pressure to push material through the pipeline, typically from a pressure vessel or a high-pressure blower. This approach is suitable for longer transport distances and when the material needs to be conveyed at higher velocities.
For carbon black and coal powder, the choice of system depends on factors like material properties, required transport distance, and the need for product containment. Carbon black, being a fine, abrasive powder, demands equipment that can handle high wear resistance and maintain particle integrity. Similarly, coal powder, often used in power generation and industrial processes, requires systems that prevent dust emissions and ensure efficient combustion. The pneumatic conveying equipment from HeadPowder addresses these challenges by incorporating robust components such as high-quality stainless steel or wear-resistant materials in the pipeline and hopper areas.
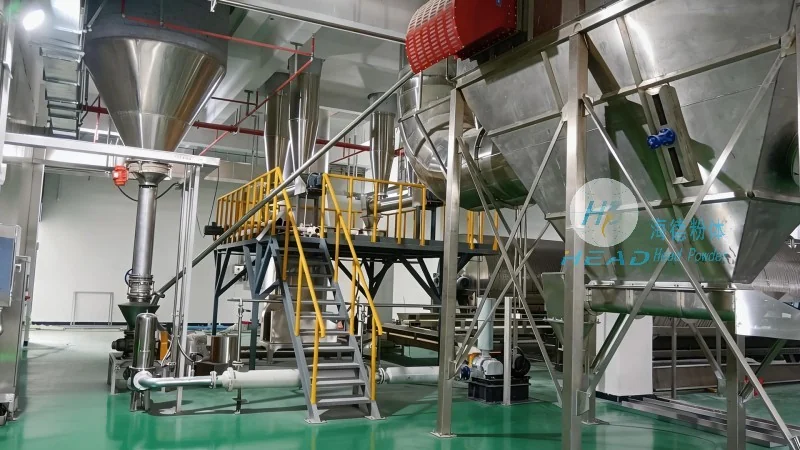
A key feature of these systems is their ability to maintain a closed-loop operation, which significantly reduces dust emissions and enhances workplace safety. The sealed pipeline design prevents the release of fine particles into the environment, aligning with environmental regulations and promoting a healthier working environment. Additionally, the systems are equipped with advanced control mechanisms that allow for precise regulation of air flow and material feed rates, ensuring consistent and reliable performance. This level of control is crucial for maintaining product quality and preventing overloading or underloading of the conveying line.
Another important aspect is the energy efficiency of the pneumatic conveying systems. By optimizing the air pressure and flow rates, the equipment minimizes energy consumption while maximizing material throughput. This not only reduces operational costs for the end-user but also contributes to a more sustainable industrial operation. The systems are designed with energy-saving features such as variable frequency drives (VFDs) that adjust the motor speed based on the actual conveying demand, further enhancing efficiency.

HeadPowder's expertise in customizing pneumatic conveying solutions ensures that each system is tailored to the specific needs of the client. Whether it's a small-scale operation requiring short-distance transport or a large industrial plant needing long-distance, high-capacity conveying, the company provides comprehensive solutions. The equipment is manufactured with precision engineering, adhering to international standards and quality certifications, ensuring durability and long service life.
In summary, the pneumatic conveying equipment for carbon black and coal powder materials operates on principles of air movement to transport fine powders efficiently and safely. The features, including closed-loop operation, energy efficiency, and customizable designs, make these systems indispensable in modern industrial settings. As a reputable manufacturer based in Shandong, China, HeadPowder continues to deliver high-quality solutions that meet the evolving demands of the industry, ensuring reliable and sustainable material handling for its clients.