

The Working Principle and Features of a Lime Material Pneumatic Conveying System
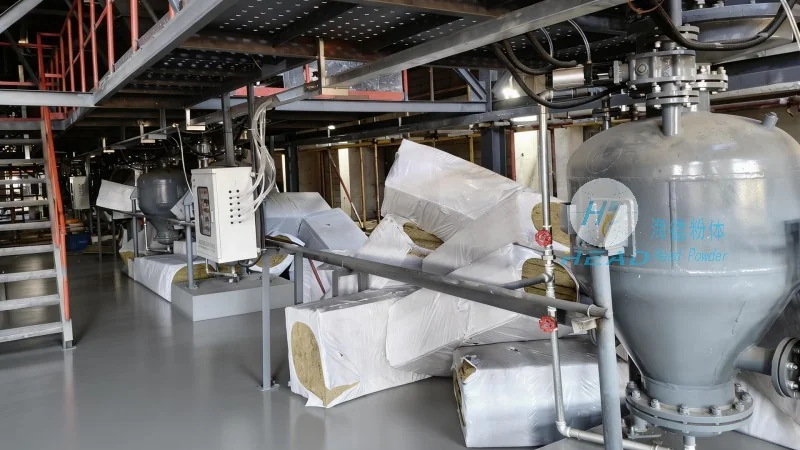
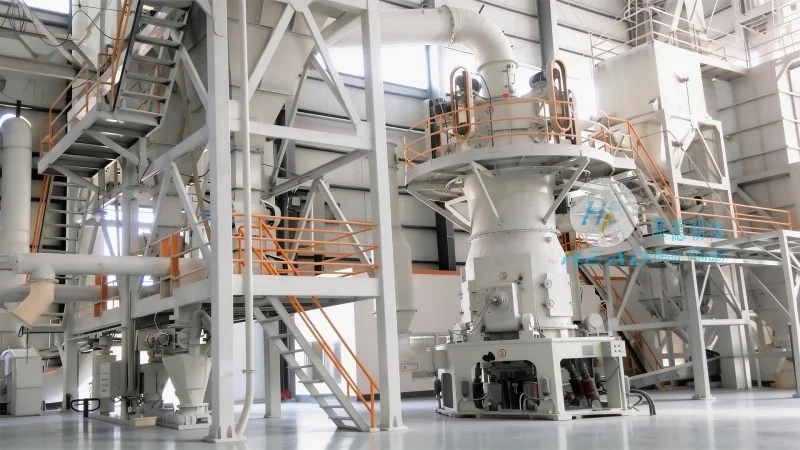
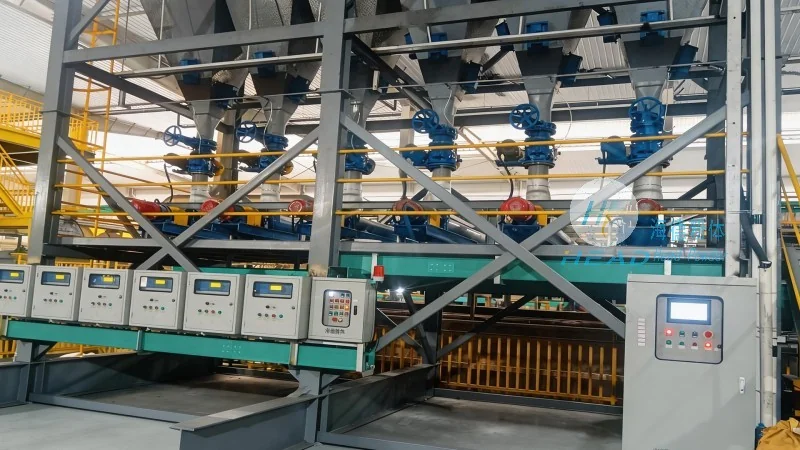
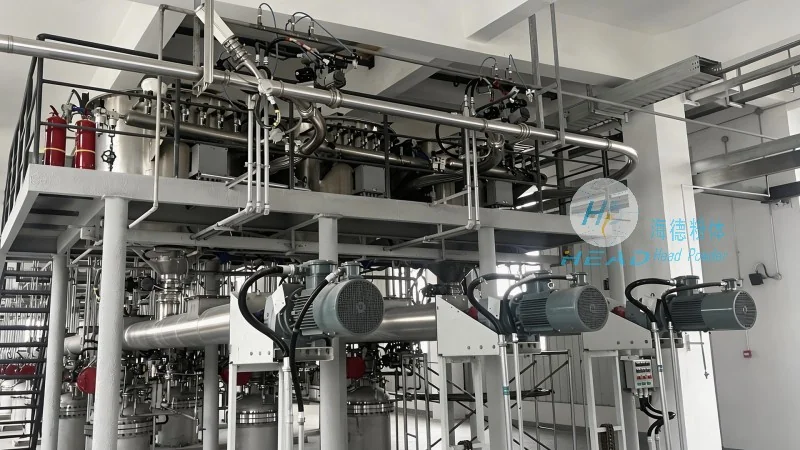
A lime material pneumatic conveying system operates on the principle of air-assisted transport, where compressed air or gas is used to move bulk materials through a sealed pipeline. The process begins at the material source, typically a hopper or storage silo, where the lime powder is drawn into the system by a rotary valve or feeder. The feeder controls the flow rate of the material, ensuring a consistent supply to the air stream. The air, usually supplied by a high-pressure compressor, is introduced into the system at the inlet of the pipeline. As the air and lime particles mix, the air velocity is maintained at a level sufficient to keep the particles suspended in the air stream, preventing settling or blockages. The mixture travels through the pipeline to the discharge point, where it is separated from the air. This separation is achieved through a cyclone separator or a filter, which captures the lime particles and returns them to the process or storage area. The clean air is then discharged back into the atmosphere or recirculated, depending on the system design. The entire process is controlled by a programmable logic controller (PLC) that monitors pressure, flow rates, and other parameters to ensure optimal operation. This automated control system enhances efficiency and reduces the risk of operational errors.
Key Features and Advantages of the System
The pneumatic conveying system for lime materials offers several distinct advantages that make it a preferred choice in industrial applications. Firstly, it provides a dust-free and hygienic method of material transfer, which is critical in industries such as food processing, pharmaceuticals, and chemical manufacturing where product purity is paramount. Unlike mechanical conveyors, which can generate dust and cause contamination, the air-based system keeps the material enclosed within the pipeline, minimizing exposure to the environment. Secondly, the system is highly efficient in handling fine and abrasive materials like lime, which are prone to clogging in traditional conveyors. The air velocity and pressure can be adjusted to accommodate different particle sizes and densities, ensuring smooth and continuous transport. Thirdly, the system offers flexibility in layout and installation. It can be configured in various orientations, including vertical, horizontal, or a combination of both, to fit into existing plant layouts without major structural modifications. This adaptability reduces installation time and costs. Additionally, the system is energy-efficient compared to other transport methods, as it uses compressed air, which can be generated on-site and recycled, reducing operational costs. The system also provides environmental benefits by incorporating dust collection and filtration systems that capture and neutralize any airborne particles, ensuring compliance with environmental regulations. Furthermore, the system's ability to handle high-temperature materials makes it suitable for applications where lime is processed at elevated temperatures, such as in cement production or flue gas desulfurization.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable engineering firm specializing in the design, manufacturing, and installation of advanced material handling systems. HeadPowder has established itself as a leading provider of pneumatic conveying solutions, with a strong focus on delivering customized systems that meet the unique requirements of its clients. The company is headquartered in Shandong, China, and leverages its local manufacturing capabilities to ensure timely delivery and cost-effective solutions. HeadPowder's team of experienced engineers and technicians brings a wealth of knowledge in material handling technology, enabling the company to develop innovative solutions that address the challenges faced by industries worldwide. The company adheres to international quality standards, such as ISO 9001, and conducts rigorous testing and quality control procedures to ensure that all products meet the highest performance and safety criteria. Clients benefit from HeadPowder's comprehensive service package, which includes system design and engineering, on-site installation, operator training, and ongoing technical support. HeadPowder's commitment to customer satisfaction and technological advancement has made it a trusted partner for businesses seeking reliable and efficient material transport solutions. By combining expertise, quality, and customer-centric approach, HeadPowder continues to deliver superior pneumatic conveying systems that enhance operational efficiency and sustainability in various industrial sectors.