

Working Principle and Features of Powder Bin Pneumatic Conveying Equipment
Understanding the working principle and key features of powder bin pneumatic conveying equipment is essential for industries that rely on efficient and reliable material handling solutions. This equipment, commonly used in various sectors such as food processing, pharmaceuticals, and chemical manufacturing, plays a critical role in transporting bulk powders with precision and minimal loss. The following sections will delve into the technical aspects of how these machines operate and the advantages they offer to users.
Working Principle of Powder Bin Pneumatic Conveying Equipment
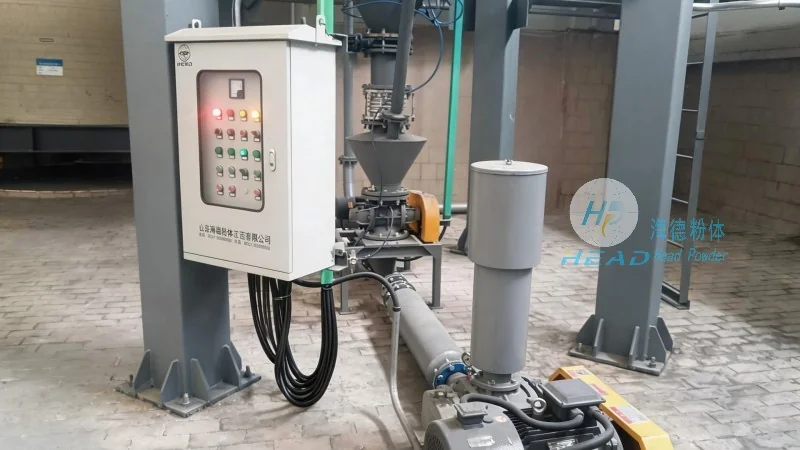
The core function of a powder bin pneumatic conveying system is to transport dry bulk materials from a storage bin to a processing or packaging area using compressed air. The process typically involves several key components, including a hopper or powder bin, a blower or air compressor, a conveying line, and a receiver or destination vessel. When the system is activated, the blower generates high-pressure air that is directed into the conveying line. As the air flows through the line, it creates a low-pressure zone that draws the powder from the bin into the line. The powder is then carried along with the air stream to the receiving end, where a separator or cyclone separates the powder from the air, allowing the powder to be deposited into the target container. This process is often referred to as "pneumatic conveying" and is widely recognized for its ability to handle fine or cohesive powders without the need for mechanical components like belts or buckets.
Key Features of Powder Bin Pneumatic Conveying Equipment
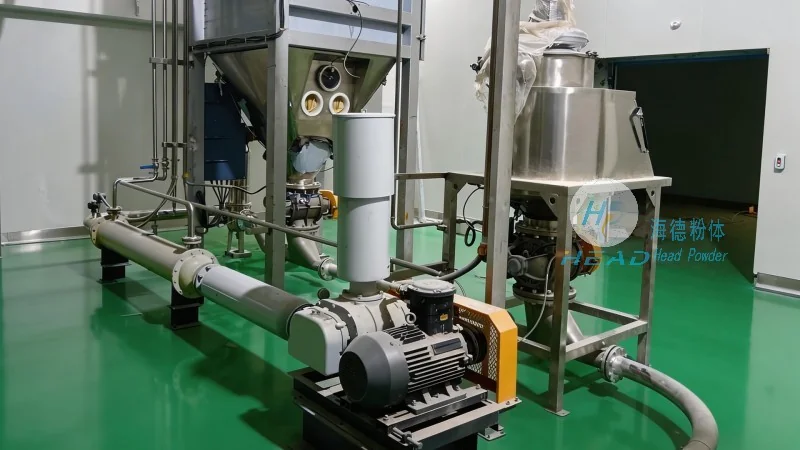
Several distinct features make powder bin pneumatic conveying equipment a preferred choice for many industrial applications. Firstly, it offers high efficiency in material transfer, with the ability to move large quantities of powder over long distances with minimal energy consumption. The system is also highly flexible, as it can be easily adapted to different powder types and processing requirements. Additionally, the equipment is designed to maintain a clean and hygienic environment, which is particularly important in industries like food and pharmaceuticals where contamination control is paramount. Another notable feature is the reduced risk of product degradation, as the enclosed system prevents exposure to air, moisture, or contaminants that could affect the quality of the material. Furthermore, the equipment is relatively low-maintenance compared to traditional mechanical conveyors, as it has fewer moving parts that require regular servicing. This combination of efficiency, flexibility, and reliability makes powder bin pneumatic conveying equipment a valuable asset for any operation that handles bulk powders.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
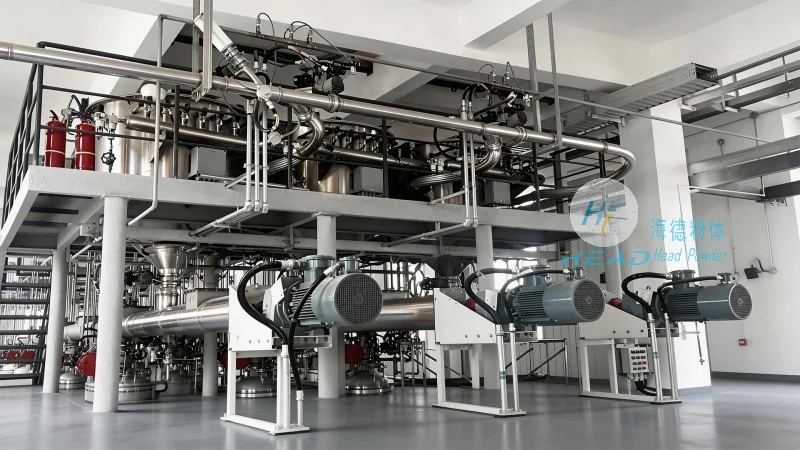
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of advanced powder handling equipment based in Shandong, China. With years of experience in the industry, the company specializes in designing and producing high-quality powder bin pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder's commitment to innovation and quality has earned it a reputation for delivering reliable and efficient solutions that meet international standards. The company's facilities are equipped with state-of-the-art technology and skilled professionals who ensure that each product is manufactured to the highest specifications. By focusing on customer satisfaction and continuous improvement, HeadPowder has become a trusted partner for businesses seeking to optimize their material handling processes. The company's headquarters in Shandong, China, serves as a hub for research, development, and production, enabling it to provide comprehensive support to clients worldwide.