

Working Principle and Features of a Calcined Sand Powder Pneumatic Conveying System
This article explores the working principle and distinctive features of a calcined sand powder pneumatic conveying system, a vital piece of equipment for efficient material handling in industrial settings. The system leverages air pressure to transport calcined sand powder through a pipeline, offering a reliable and flexible solution for various industrial processes. By understanding its core functionality and advantages, users can appreciate how this technology enhances operational efficiency and product quality in material transport applications.
Working Principle of the Pneumatic Conveying System
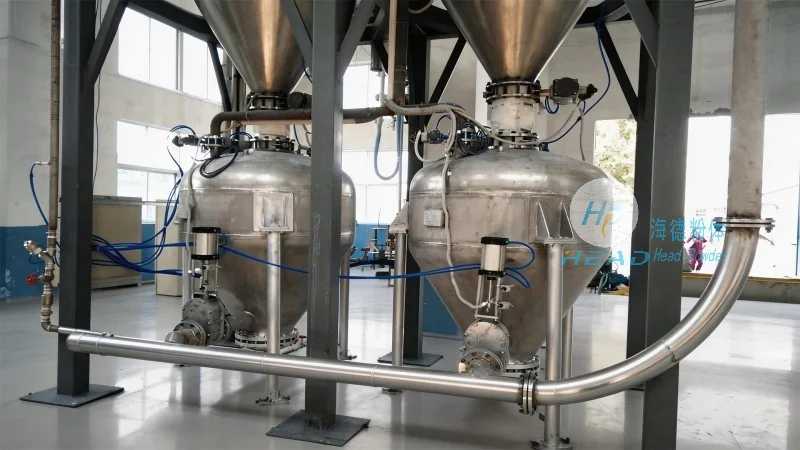
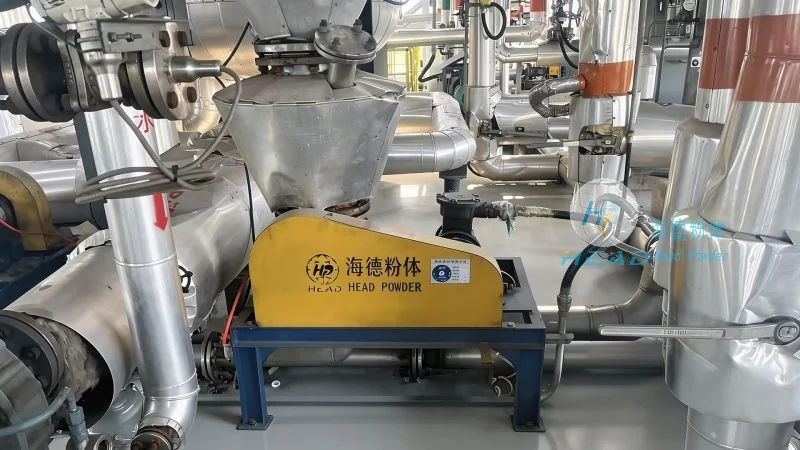
The calcined sand powder pneumatic conveying system operates on the fundamental principle of air flow to move powder materials. The system typically comprises several key components: a hopper for material storage, a feeder to control the powder flow rate, a pipeline for conveying the material, and a receiver to collect the material at the destination. The process begins with calcined sand powder being fed from a storage silo into the hopper. The feeder then regulates the amount of powder entering the pipeline. Compressed air is introduced into the pipeline, creating a flow that carries the powder particles along the pipeline to the receiver. At the receiver, the air and powder mixture is separated, with the powder collected and the air either discharged or recirculated. This continuous cycle ensures efficient and consistent material transport without the need for mechanical components like belts or buckets, minimizing wear and tear and reducing maintenance costs.
Key Features and Advantages of the System
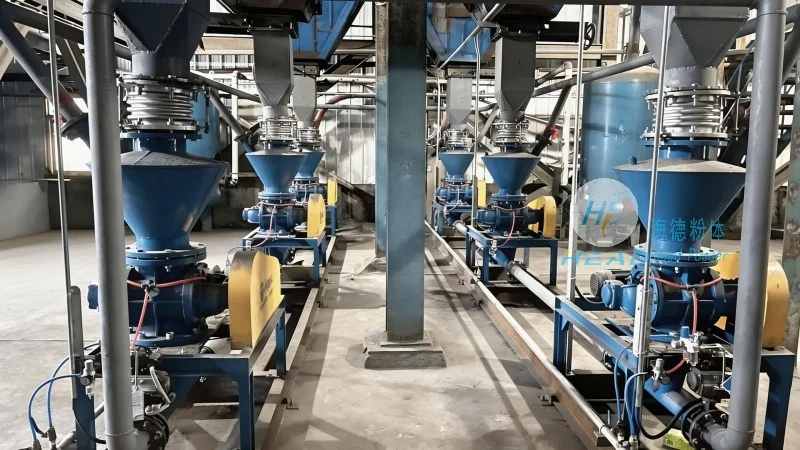
The calcined sand powder pneumatic conveying system offers several key features that make it an ideal choice for handling calcined sand powder. Firstly, it provides a dust-free and clean operation, which is critical for maintaining product purity and ensuring a safe working environment. The system’s design minimizes dust generation and allows for easy cleaning, reducing the risk of contamination and improving overall hygiene. Secondly, the system is highly flexible and can be easily integrated into existing production lines or modified to accommodate varying material flow rates. This adaptability makes it suitable for a wide range of industrial applications, from small-scale operations to large-scale production facilities. Thirdly, the system offers high efficiency in material transport, with minimal material loss and low energy consumption. The use of air as the conveying medium allows for the transport of materials over long distances with minimal friction and resistance, resulting in lower operational costs. Additionally, the system is capable of handling a wide range of particle sizes and moisture contents, making it versatile for different calcined sand applications. The air flow can be adjusted to suit the specific characteristics of the powder, ensuring optimal conveying performance.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related industrial equipment. The company is headquartered in Shandong, China, and has established itself as a trusted partner in providing high-quality material handling solutions for various industries. With a strong commitment to innovation and customer satisfaction, HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. The company’s products are widely used in sectors such as mining, cement, chemical, and food processing, where efficient and safe material transport is essential for operational success. HeadPowder’s team of experienced engineers and technicians work closely with clients to understand their unique requirements and develop solutions that enhance productivity, reduce costs, and improve overall operational efficiency. The company adheres to strict quality control standards and uses advanced manufacturing techniques to ensure that its products meet the highest industry standards and deliver reliable performance over the long term.