

Working Principle and Features of Heptahydrate Magnesium Sulfate Powder Conveying System Equipment
Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial and agricultural applications. The efficient and reliable transport of this powder is crucial for maintaining production efficiency and product quality. This article explores the working principle and key features of the heptahydrate magnesium sulfate powder conveying system equipment, highlighting its design and operational advantages.
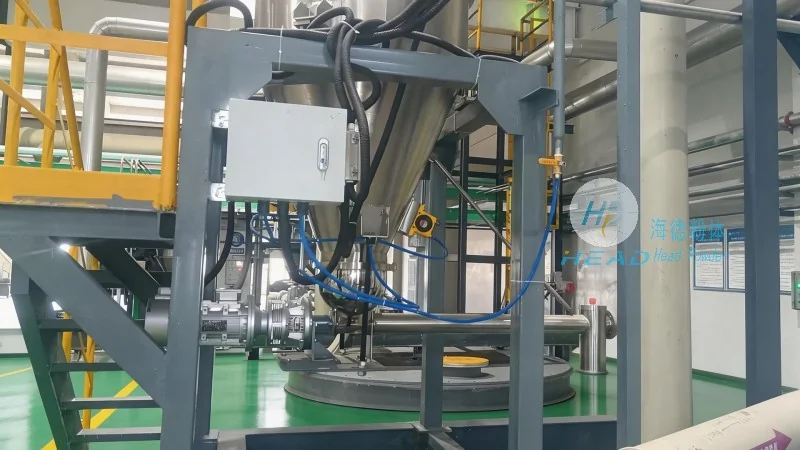
Manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the powder handling industry, this system is engineered to meet the demanding requirements of bulk material transport. The company, often referred to as HeadPowder, is based in Shandong, China, and specializes in developing advanced solutions for powder processing and conveying.
Working Principle of the Heptahydrate Magnesium Sulfate Powder Conveying System
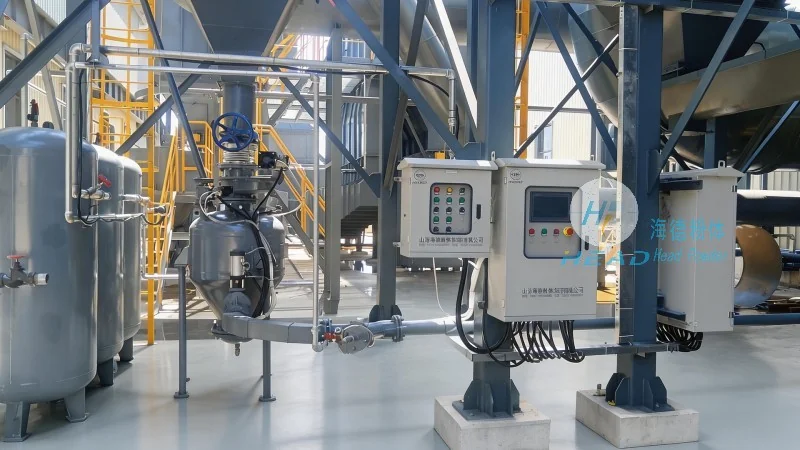
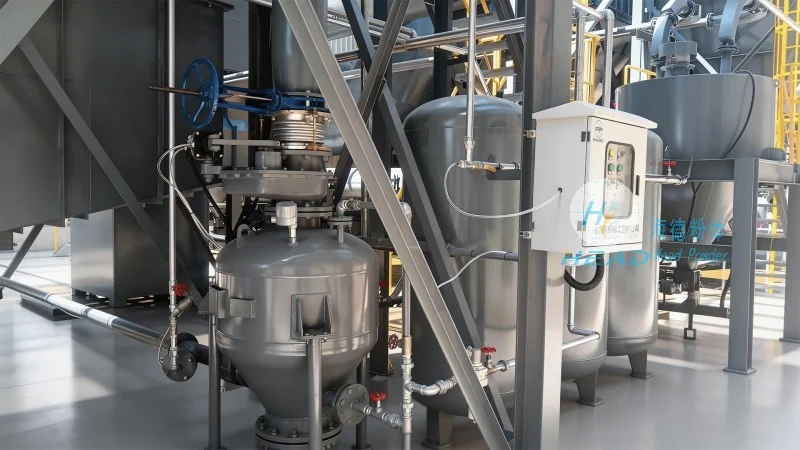
The system operates on a principle of pneumatic or mechanical conveying, depending on the specific design. For pneumatic systems, compressed air is used to create a flow that moves the powder through a pipeline. The equipment typically includes a hopper for material storage, a feeder to control the flow rate, and a conveyor section that transports the powder to the destination. The design ensures minimal product degradation and loss, maintaining the integrity of the heptahydrate magnesium sulfate during transport.
Key Features of the Powder Conveying System
Several notable features distinguish this conveying system. Firstly, it offers high conveying efficiency, capable of handling large volumes of powder with minimal energy consumption. The system is also designed for easy maintenance, with accessible components that simplify routine checks and repairs. Another key feature is its adaptability, allowing integration with existing production lines or new setups. Additionally, the equipment is constructed from materials resistant to corrosion and wear, ensuring long-term durability and reliable performance.
Advantages in Industrial Applications
The heptahydrate magnesium sulfate powder conveying system is particularly beneficial in industries such as pharmaceuticals, agriculture, and chemical manufacturing. By ensuring consistent and efficient transport, it helps maintain product quality and reduces downtime. The system's ability to handle fine powders without clogging or agglomeration is a significant advantage, as it prevents product contamination and improves overall process reliability.
Shandong HeadPowder Engineering Co., Ltd. continues to innovate in powder handling technology, providing solutions that enhance operational efficiency and product integrity. The heptahydrate magnesium sulfate powder conveying system exemplifies the company's commitment to quality and performance, serving as a reliable choice for businesses requiring dependable bulk material transport.