

Working Principle and Features of Paper Chip Powder Conveying Equipment
When it comes to efficiently transporting paper chip powders, specialized equipment is essential for maintaining process efficiency and product integrity. The paper chip powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is designed to meet these demands with advanced engineering and robust construction. This article explores the working principle and key features of this equipment, providing insights into its functionality and benefits for industrial applications.
Company Introduction
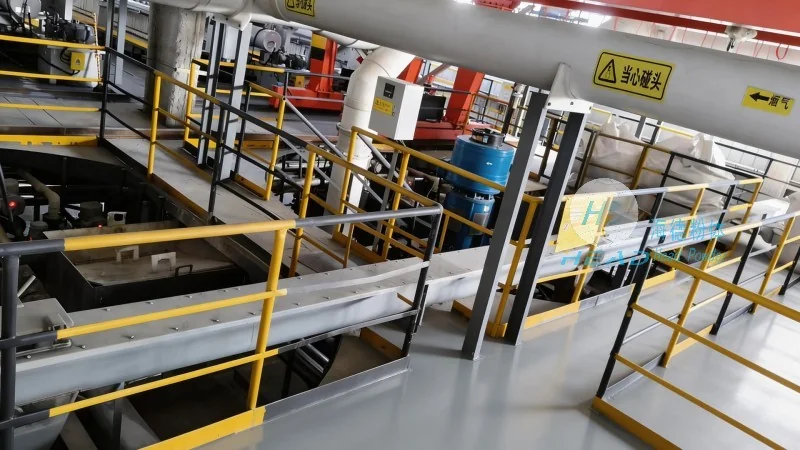
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of powder handling solutions. Based in Shandong, China, the company specializes in developing and supplying high-quality conveying systems tailored to the unique requirements of various industries. With a focus on innovation and customer satisfaction, headpowder delivers reliable equipment that enhances operational performance and reduces downtime.
Working Principle of Paper Chip Powder Conveying Equipment
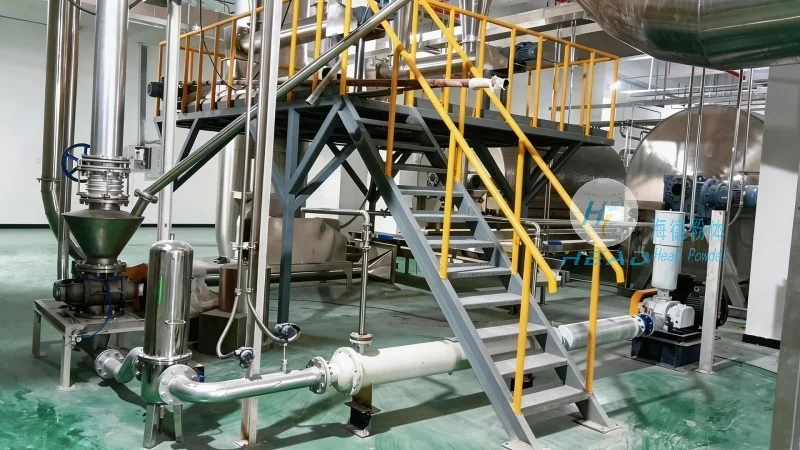
The core working principle of paper chip powder conveying equipment involves the use of mechanical components to transport bulk materials from one location to another. For paper chip powders, which are typically lightweight and can be prone to dust generation, the system is engineered to handle these characteristics effectively. The equipment commonly employs a combination of components such as feed hoppers, conveyor belts or screws, and control mechanisms to ensure smooth material flow. The feed hopper collects the paper chips and feeds them into the conveyor system, where they are transported through a sealed or semi-sealed pathway. The conveyor mechanism, often a screw or belt, moves the material along the designated route, while control valves and sensors regulate the flow rate and prevent blockages. This integrated approach ensures that the paper chips are moved efficiently without causing contamination or degradation.
Key Features of the Conveying Equipment
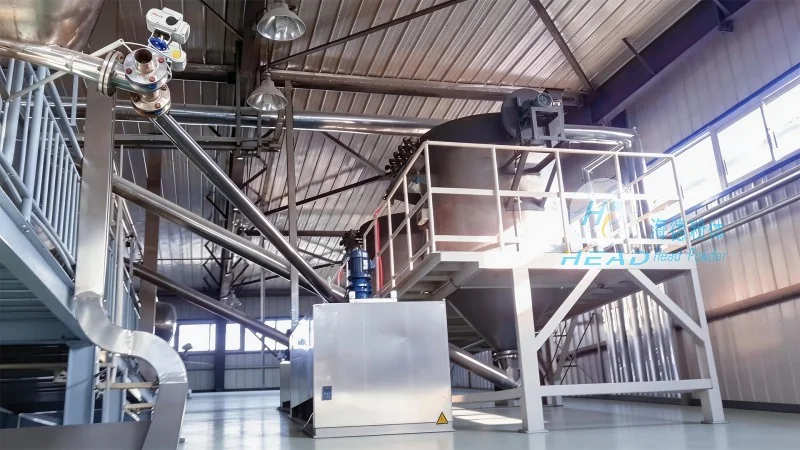
The paper chip powder conveying equipment from headpowder is distinguished by several key features that enhance its performance and usability. Firstly, the equipment is designed with a focus on dust control, which is critical for maintaining a clean and safe working environment. The sealed or semi-sealed conveyor system minimizes the release of fine particles, reducing the risk of inhalation and ensuring compliance with occupational health standards. Secondly, the equipment offers high efficiency in material transport, with adjustable speed settings that allow operators to optimize the flow rate based on the specific application requirements. This adaptability ensures that the system can handle varying loads and production volumes without compromising performance. Thirdly, the robust construction of the equipment ensures durability and long-term reliability. Made from high-quality materials, the components are resistant to wear and corrosion, reducing the need for frequent maintenance and extending the equipment's service life. Additionally, the equipment incorporates user-friendly control interfaces, making it easy for operators to monitor and adjust the system parameters as needed. This feature enhances operational flexibility and reduces the learning curve for new users.
Benefits and Applications
The implementation of paper chip powder conveying equipment brings numerous benefits to industrial processes. By streamlining the material transport process, the equipment reduces labor costs and improves overall productivity. The efficient handling of paper chips minimizes material loss and contamination, which is crucial for maintaining product quality. Furthermore, the equipment's ability to handle bulk materials in a controlled manner enhances safety in the workplace by reducing the need for manual handling of heavy or dusty materials. The applications of this equipment span various industries, including paper manufacturing, recycling, and waste management. In paper mills, the equipment is used to transport paper chips from collection points to processing facilities, ensuring a continuous supply of raw materials. In recycling operations, it helps in moving processed paper chips to storage or further processing stages. Overall, the equipment plays a vital role in optimizing material flow and enhancing operational efficiency across different industrial settings.
Conclusion
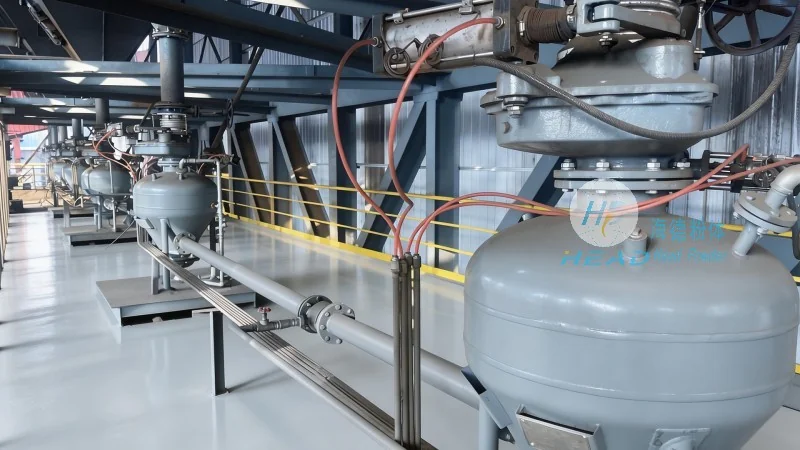
Shandong HeadPowder Engineering Co., Ltd.'s paper chip powder conveying equipment exemplifies advanced technology and practical design, addressing the unique challenges of handling paper chip powders. Through its efficient working principle and comprehensive features, the equipment provides reliable and effective solutions for industrial applications. By prioritizing dust control, efficiency, and durability, headpowder's equipment ensures that businesses can maintain high standards of performance while operating safely and sustainably. For industries requiring reliable bulk material transport, this equipment from headpowder is a valuable investment that enhances operational capabilities and supports long-term success.