

Working Principle and Features of Coal Ash Powder Conveying Equipment
Coal ash powder conveying equipment is a specialized system engineered for the efficient and safe transportation of coal ash, a fine powder byproduct of coal combustion. This equipment is indispensable in industrial settings, particularly in power generation and waste management facilities, where handling such materials requires precise control and minimal environmental impact. The design and functionality of these systems are tailored to address the unique challenges posed by coal ash, including its abrasive nature, tendency to generate dust, and the need for reliable, low-maintenance operation. By leveraging advanced technology and robust construction, these conveyors ensure consistent and safe material transport, supporting the overall efficiency of industrial processes.
Working Principle of Coal Ash Powder Conveying Equipment
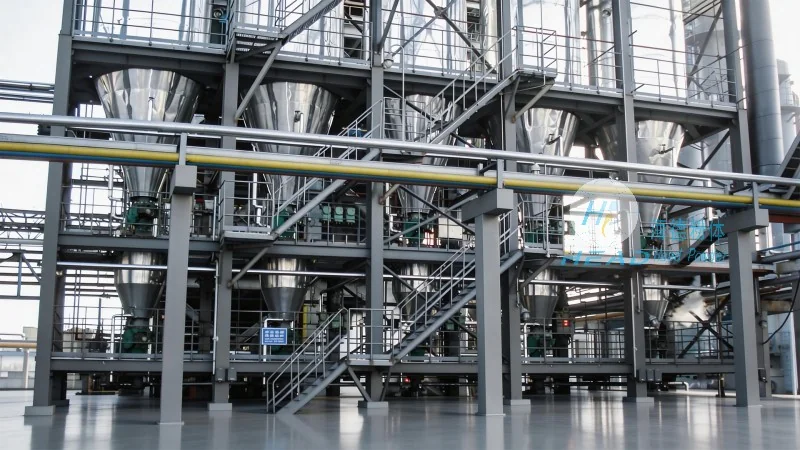
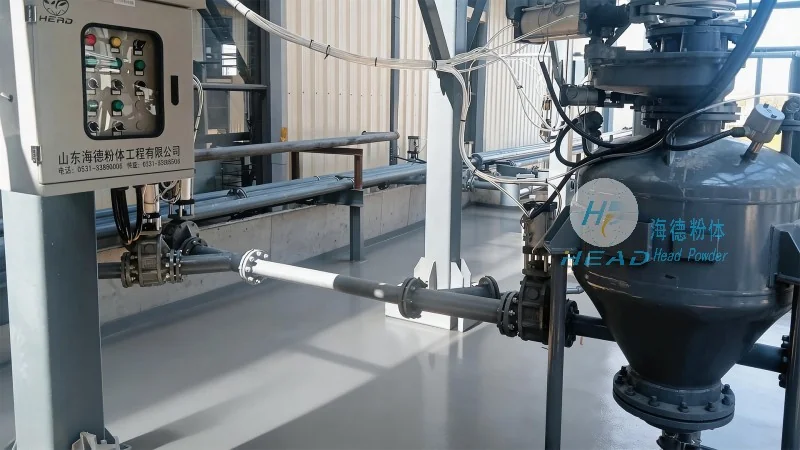
The fundamental working principle of coal ash powder conveying equipment centers on the use of positive pressure or negative pressure systems to move the material through a pipeline. In positive pressure systems, a high-capacity fan or blower generates a high-pressure air stream that carries the coal ash particles along the pipeline. This method is ideal for short to medium-distance applications, such as transporting coal ash from a storage silo to a processing unit or disposal site. The equipment typically comprises a hopper for material feeding, a rotary valve or feeder to regulate the flow rate, and a pipeline system equipped with appropriate fittings, valves, and sensors to direct and monitor the flow. The air velocity within the pipeline is carefully controlled to maintain the coal ash particles in suspension, preventing blockages and ensuring consistent delivery. For longer distances or more complex layouts, negative pressure systems may be employed, where a vacuum pump creates a low-pressure environment that draws the material through the pipeline. Both systems are designed to optimize material transport while minimizing energy consumption and operational costs.
Key Features of Coal Ash Powder Conveying Equipment
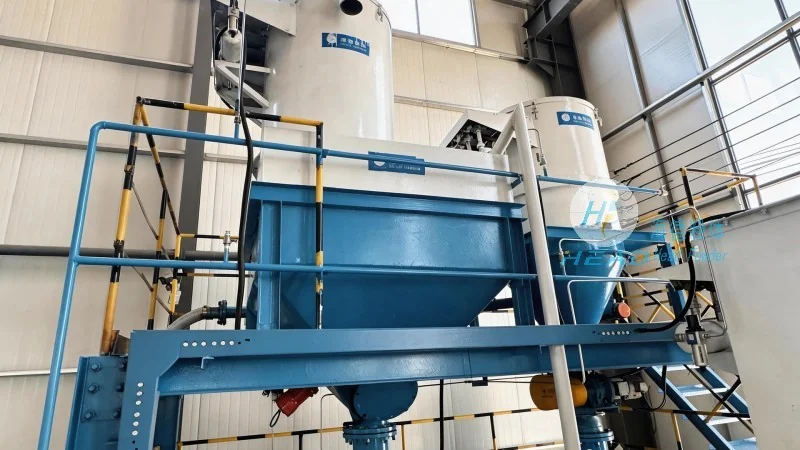
Coal ash powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is distinguished by several key features that enhance performance, reliability, and user experience. One of the primary features is the robust construction, which incorporates high-quality materials like stainless steel or wear-resistant alloys to withstand the abrasive and corrosive properties of coal ash. This design minimizes wear and extends the equipment's service life, reducing long-term maintenance costs. The system also includes advanced material handling components, such as precision rotary valves and adjustable feeders, which allow for precise control of the flow rate and pressure, ensuring consistent and efficient conveying. Another critical feature is the integration of dust control mechanisms, including filters and containment systems, to mitigate the environmental impact of coal ash dust and comply with environmental regulations. The equipment is further equipped with automated control systems that enable real-time monitoring and adjustment of operational parameters, enhancing operational efficiency and reducing the need for manual intervention. Additionally, the design emphasizes energy efficiency, with optimized fan and blower designs that reduce power consumption while maintaining high conveying capacity, making it a cost-effective solution for industrial applications.
Applications and Benefits in Industrial Settings
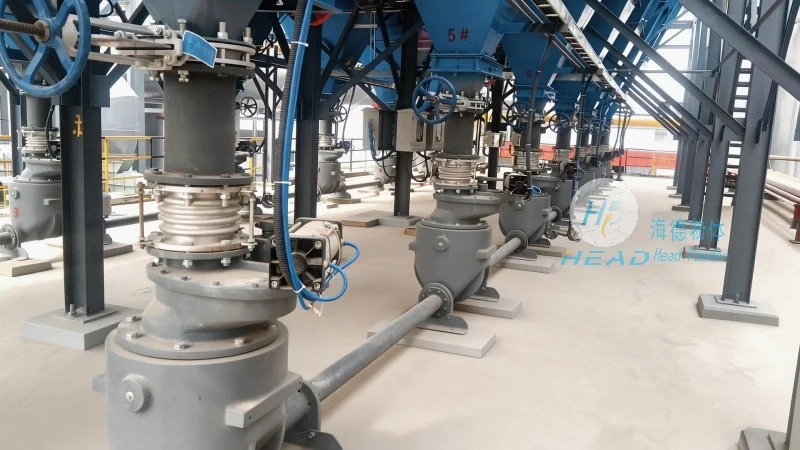
Coal ash powder conveying equipment is widely utilized in various industrial applications where the handling of coal ash is essential. In power plants, these systems play a vital role in transporting coal ash from the boiler to storage facilities or for reusing it in cement production processes. The equipment's ability to handle large volumes of fine powder with minimal downtime enhances the overall efficiency of power generation operations. In waste management facilities, the equipment streamlines the process of transporting coal ash from collection points to disposal or recycling sites, improving operational workflow and reducing labor costs. The benefits of using specialized conveying equipment extend beyond efficiency; it also improves workplace safety by reducing the need for manual handling of coal ash, which can pose respiratory and other health risks due to its dust content. Furthermore, the reliability of the system contributes to reduced maintenance costs and longer equipment lifespan, making it a sustainable and economical solution for long-term use. The integration of advanced technology in these systems ensures that they can adapt to varying operational conditions, providing consistent performance and supporting the sustainability goals of industrial facilities.