

Working Principle and Characteristics of Slurry and Powder Conveying
Slurry and powder conveying systems operate based on fundamental principles that ensure efficient and reliable transport of particulate materials. The core mechanism involves the use of specialized equipment designed to handle the unique properties of slurry—mixtures of solid particles suspended in a liquid medium. In these systems, the primary goal is to move the material from a source to a destination while maintaining the integrity of the mixture and minimizing degradation or separation of components.
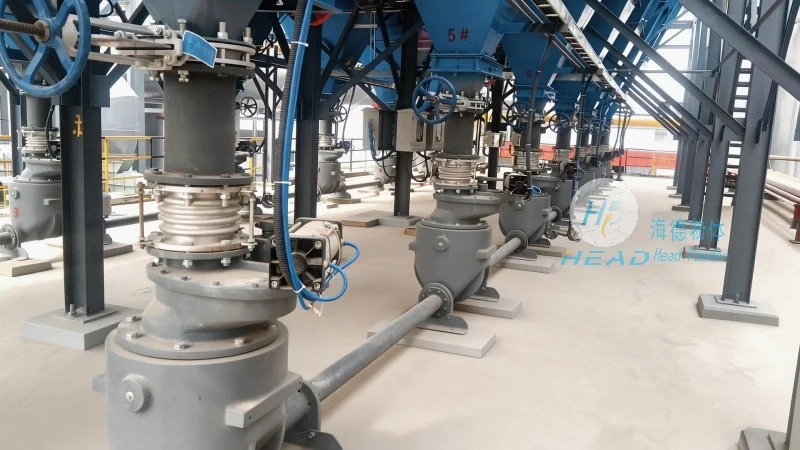
One of the key working principles is the utilization of pressure or vacuum to create a flow path. For example, pneumatic conveying systems use compressed air to push the slurry through pipelines, while hydraulic systems rely on pumps to generate the necessary pressure. In some cases, a combination of both methods is employed to optimize performance, especially for materials with varying particle sizes and moisture content. The selection of the conveying method depends on factors such as the type of material, its flow characteristics, and the distance to be covered. Each approach has its advantages and limitations, which are critical considerations for system design.
Key Characteristics of Slurry and Powder Conveying Systems
Slurry and powder conveying systems exhibit several distinct characteristics that set them apart from traditional bulk material handling methods. One of the most notable features is their ability to handle a wide range of materials, including fine powders, coarse particles, and even wet mixtures. This versatility makes them suitable for industries such as mining, construction, and chemical processing, where diverse material types are common.
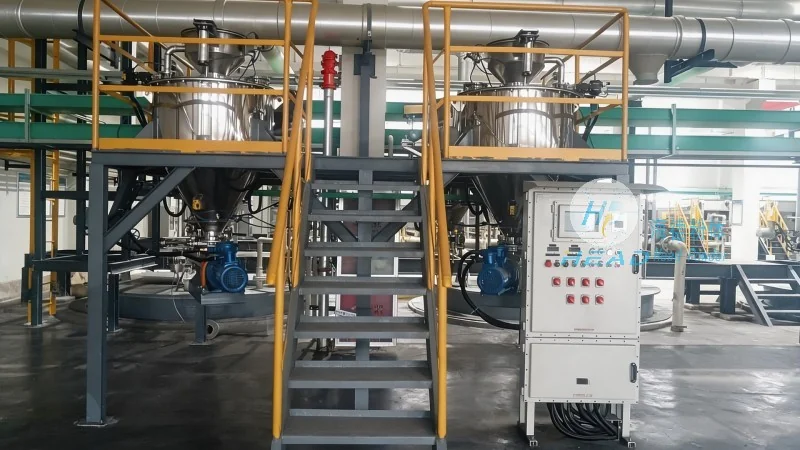
Another important characteristic is the efficiency in terms of energy consumption and operational costs. Modern systems are designed to minimize energy waste by optimizing the flow rate and pressure, reducing the need for excessive power. Additionally, the use of advanced control technologies allows for precise regulation of the conveying process, ensuring consistent material delivery and reducing downtime. This efficiency is particularly valuable in large-scale operations where continuous production is essential.
Advantages and Applications in Industrial Settings
The advantages of slurry and powder conveying systems extend beyond their operational efficiency. They offer significant benefits in terms of safety and environmental impact. By transporting materials in a closed system, these systems prevent dust emissions and reduce the risk of airborne contamination, which is crucial in industries dealing with hazardous or fine powders. This not only enhances workplace safety but also complies with environmental regulations.
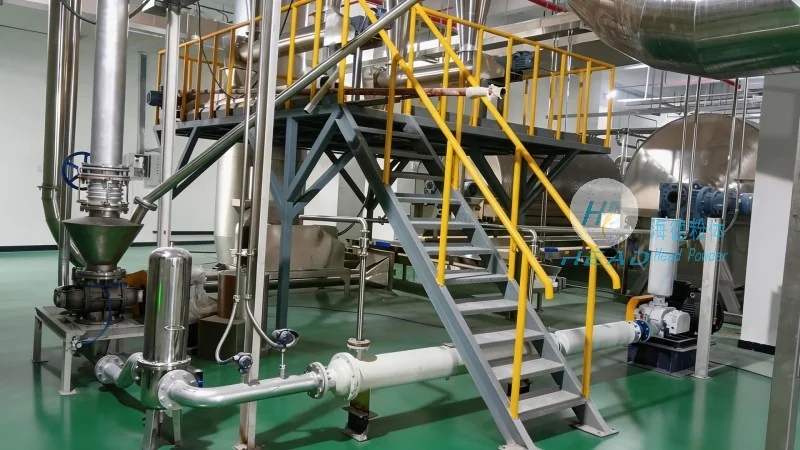
Furthermore, the systems provide flexibility in terms of layout and integration with existing infrastructure. They can be easily adapted to different plant configurations, allowing for seamless integration with other processing equipment. This adaptability is particularly beneficial in retrofitting older facilities or expanding production capabilities without major disruptions.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of slurry and powder conveying solutions. With a strong focus on innovation and customer satisfaction, the company specializes in designing, manufacturing, and implementing advanced conveying systems tailored to the specific needs of various industries. HeadPowder's expertise lies in understanding the unique challenges of material handling and developing customized solutions that address these challenges effectively.
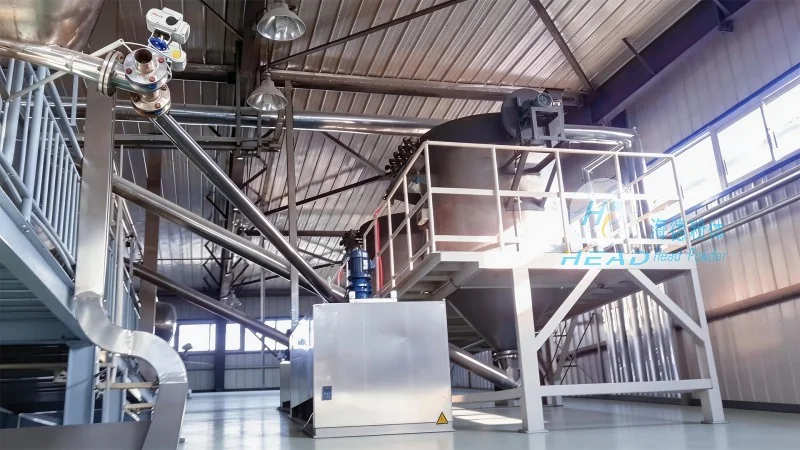
HeadPowder operates from China, where it leverages local resources and expertise to deliver high-quality products and services. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols. By combining technical excellence with a customer-centric approach, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient slurry and powder conveying systems.
Conclusion: The Future of Slurry and Powder Conveying
As industries continue to evolve, the demand for advanced slurry and powder conveying systems remains high. The integration of technology, such as automation and data analytics, is expected to further enhance the performance and efficiency of these systems. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of this evolution, continuously innovating to meet the changing needs of the market. By leveraging their expertise and commitment to quality, they are helping businesses optimize their material handling processes and achieve greater productivity and sustainability.