

Working Principle and Characteristics of Light Calcium Powder Pneumatic Conveying
Light calcium powder, also known as precipitated calcium carbonate (PCC), is a widely used industrial material in sectors such as plastics, paper, and coatings. Efficient transportation of this fine powder is critical for industrial processes, and pneumatic conveying has become a preferred method due to its advantages over traditional mechanical systems.
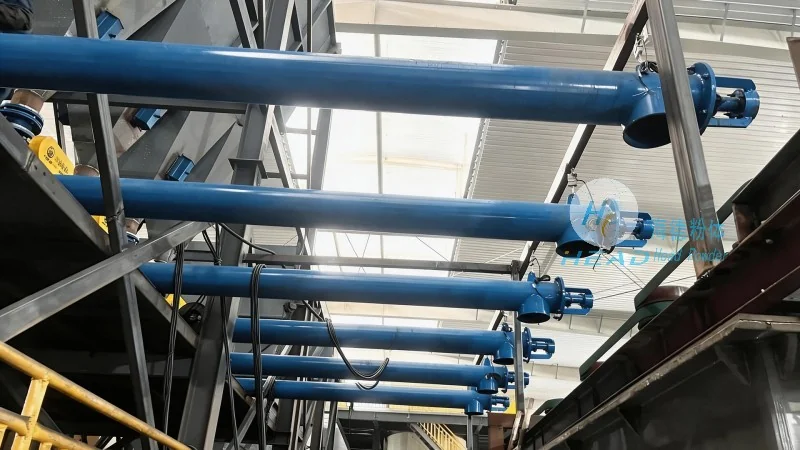
Working Principle of Light Calcium Powder Pneumatic Conveying
Pneumatic conveying systems for light calcium powder operate by utilizing air or gas to transport powder particles through a pipeline. The core mechanism involves creating a pressure differential between the inlet and outlet of the conveying line. Typically, the powder is fed into a hopper or feeder, where it is introduced into the pipeline alongside a stream of air. The air flow, generated by a blower or compressor, lifts and transports the powder particles. The air velocity must be sufficient to overcome gravitational forces and maintain a stable suspension. Key components include a feeder, conveying line, receiver, and often a filter or separator to remove entrained air or fine particles.
Key Characteristics of Light Calcium Powder Pneumatic Conveying
The characteristics of pneumatic conveying for light calcium powder are defined by system type (positive/negative pressure), powder properties, and equipment design. A primary characteristic is handling fine, dusty powders without segregation or agglomeration. Light calcium powder particles (sub-micron to micrometer range) are prone to sticking; pneumatic systems maintain uniform size distribution and prevent particle attrition. Another key characteristic is energy efficiency and high throughput capacity, with modern systems achieving cost-effective large-scale transport. Flexibility in adjusting flow rates and pressure settings also enhances adaptability to process requirements.
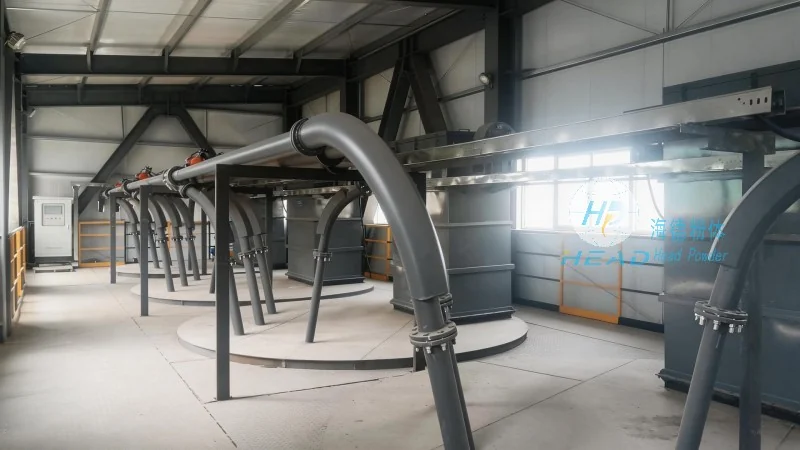
Advantages of Pneumatic Conveying for Light Calcium Powder
Compared to mechanical conveying, pneumatic systems offer several benefits. First, they eliminate moving parts in contact with powder, reducing wear and contamination risks. Mechanical conveyors (screws, belts) can degrade particles or introduce foreign materials, while pneumatic systems use air as the medium for a clean transport. Second, the sealed pipeline prevents dust contamination and environmental pollution, ensuring workplace safety and regulatory compliance. Third, the system accommodates both horizontal and vertical transport, making it versatile for facility integration. Finally, low maintenance and long service life contribute to economic viability for industrial operations.
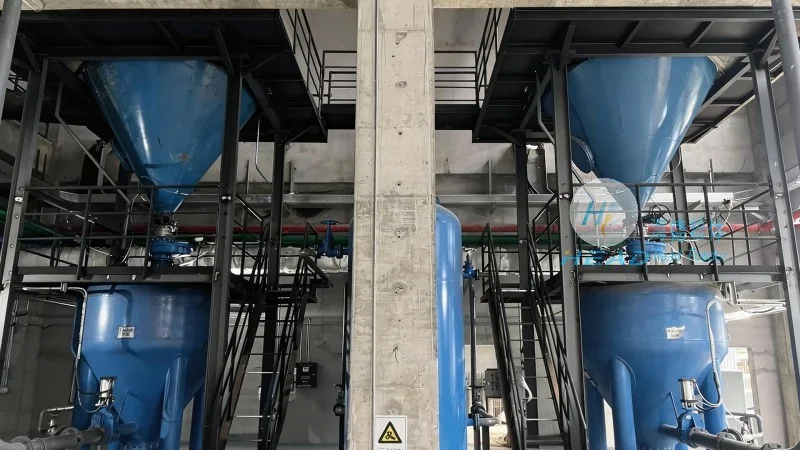
Applications of Light Calcium Powder Pneumatic Conveying
Pneumatic conveying is applied across diverse industries. In plastics, light calcium powder is used as a filler to enhance mechanical properties and reduce costs. Systems transport powder from silos to processing equipment, ensuring consistent feed. In the paper industry, it serves as a coating pigment to improve brightness and smoothness, with precise flow control for uniform coating. In coatings and paints, it acts as a pigment/extender for durability and appearance. For food and pharmaceuticals, where light calcium powder is a food additive or filler, the system provides hygienic, contamination-free transport, meeting strict quality standards.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., or HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems for light calcium powder and other fine powders. The company specializes in designing, manufacturing, and installing customized solutions tailored to client needs. With a focus on innovation and quality, HeadPowder has established itself as a trusted partner, providing reliable and efficient material handling solutions. HeadPowder’s headquarters is in Shandong, China, where a dedicated team of engineers and technicians collaborate with clients to develop optimal conveying systems. The company’s commitment to customer satisfaction and technological advancement makes it a preferred choice for businesses seeking to improve operational efficiency and process reliability.