

What is a Metering Bin Pump Pneumatic Conveying Equipment? And What Are Its Design Principles?
For industrial applications requiring precise material handling, the metering bin pump is a critical component in pneumatic conveying systems. This equipment is designed to efficiently transport bulk materials through a pipeline network using compressed air or other gases. Understanding its function and design principles is essential for selecting the right system for specific industrial needs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and production of advanced pneumatic conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries such as food processing, pharmaceuticals, chemicals, and more. HeadPowder's commitment to excellence ensures that their products meet the highest standards of performance and reliability.
How Metering Bin Pumps Work
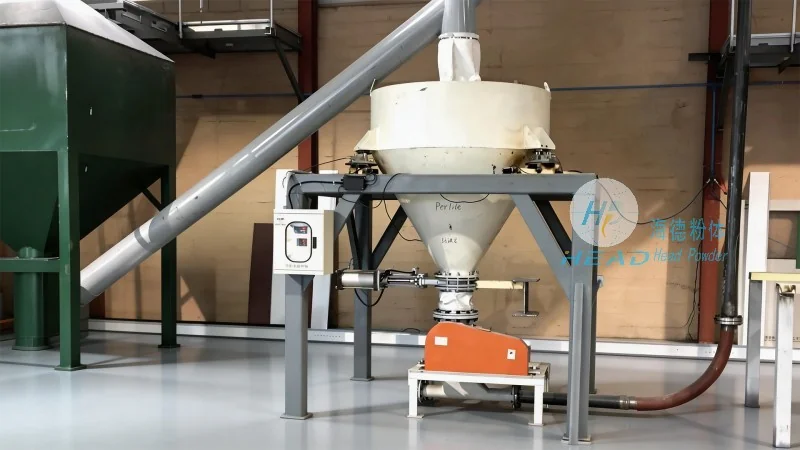
The metering bin pump operates by utilizing a hopper or bin to store bulk materials. The material is then fed into a pump chamber where it is mixed with compressed air or gas. The air pressure forces the material through a pipeline to the destination point. The design allows for precise control over the flow rate, ensuring consistent and accurate material delivery. This method is particularly effective for handling materials that are difficult to convey using traditional methods, such as powders, granules, and fine particles.
Design Principles of Metering Bin Pumps
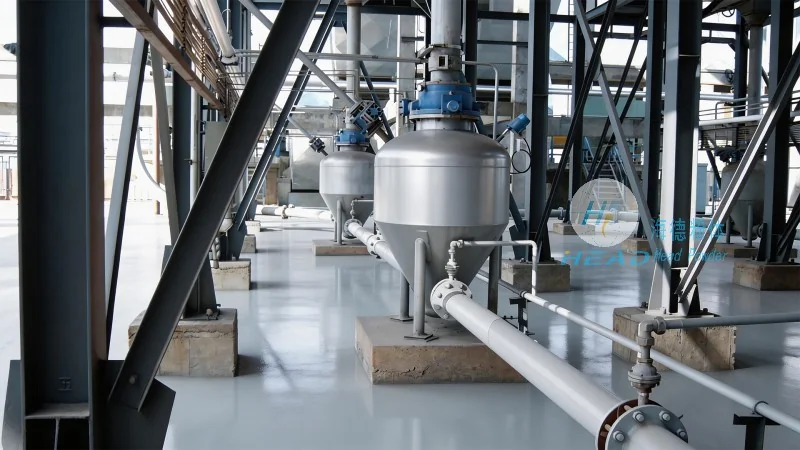
The design of a metering bin pump focuses on several key principles to ensure optimal performance. First, the pump must be able to handle a wide range of materials, from low to high density. The hopper design is crucial, as it needs to prevent material bridging and ensure a smooth flow into the pump chamber. Second, the air-to-material ratio is carefully controlled to maintain a stable conveying condition. This ratio determines the efficiency of the system and the pressure required to move the material. Third, the pump's construction must be robust and durable to withstand the abrasive nature of many bulk materials. Materials like stainless steel or special alloys are often used to prevent corrosion and wear.
Key Advantages of Metering Bin Pumps
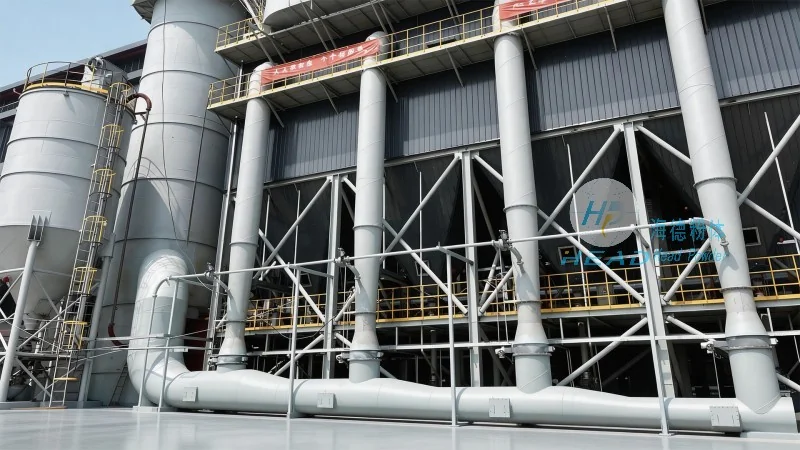
Using a metering bin pump offers several advantages over traditional conveying methods. One of the primary benefits is the ability to achieve precise control over the material flow rate. This is particularly important in processes where accurate dosing is required, such as in chemical mixing or pharmaceutical production. Additionally, the system is compact and can be integrated into existing facilities with minimal modifications. The pneumatic conveying method also reduces the risk of contamination, making it suitable for handling food-grade or pharmaceutical materials. Furthermore, the equipment is energy-efficient compared to other bulk handling solutions, contributing to lower operational costs.
Conclusion
Metering bin pumps are an essential component in modern industrial material handling systems. Their ability to provide precise, reliable, and efficient conveying of bulk materials makes them a preferred choice for many industries. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of advanced metering bin pump systems, ensuring that customers receive high-quality equipment tailored to their specific needs. By understanding the design principles and operational capabilities of this equipment, businesses can make informed decisions to enhance their material handling processes and improve overall productivity.