

Introduction to Intelligent Pneumatic Conveying Systems: Overview of Structure and Working Principle
Intelligent pneumatic conveying systems represent a sophisticated solution for bulk material handling, integrating advanced technology with efficient design to meet the demands of modern industrial processes. This overview will explore the key components, working principles, and advantages of such systems, highlighting their role in enhancing operational efficiency and reliability.
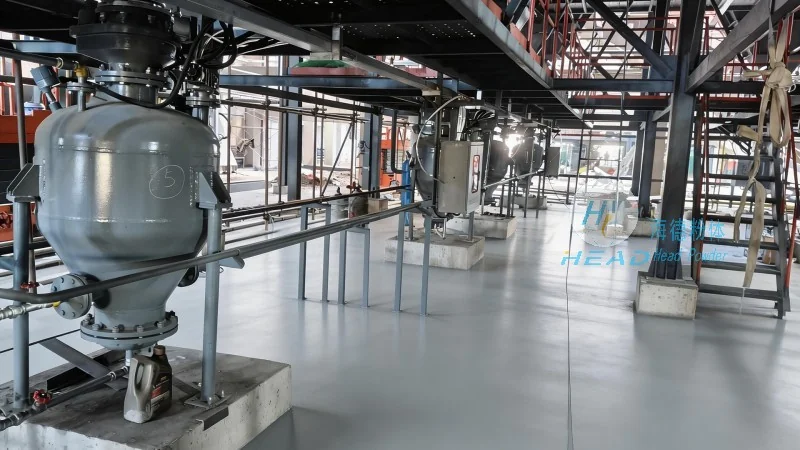
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Headpowder, a leading provider in the field, is dedicated to delivering high-quality pneumatic conveying solutions. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for industries requiring reliable bulk material transport. The company's expertise lies in customizing systems to suit specific operational needs, ensuring optimal performance and longevity.
Core Components and Structure of the Intelligent Pneumatic Conveying System
The intelligent pneumatic conveying system typically comprises several critical components that work in harmony to facilitate material transport. These include the material hopper, which serves as the storage and feeding unit; the air compressor or blower, responsible for generating the necessary air pressure; the conveying line, which may consist of flexible hoses or rigid pipes; and the control system, equipped with sensors and automation features for real-time monitoring and adjustment. Additionally, the system may incorporate features like material classifiers, cyclones, or filters to ensure material quality and separation.

Working Principle of the Pneumatic Conveying System
The fundamental working principle of the system involves the use of compressed air to transport bulk materials through a pipeline. When the material is released from the hopper, it is drawn into the conveying line by the air flow generated by the compressor. The air and material mixture travels through the pipeline, with the air pressure maintaining the material in suspension. At the destination point, the air is separated from the material, often through a cyclone or filter, allowing the material to be discharged while the air is recirculated or vented. The intelligent control system plays a crucial role by monitoring parameters such as pressure, flow rate, and material level, adjusting the air supply as needed to maintain optimal conveying conditions.
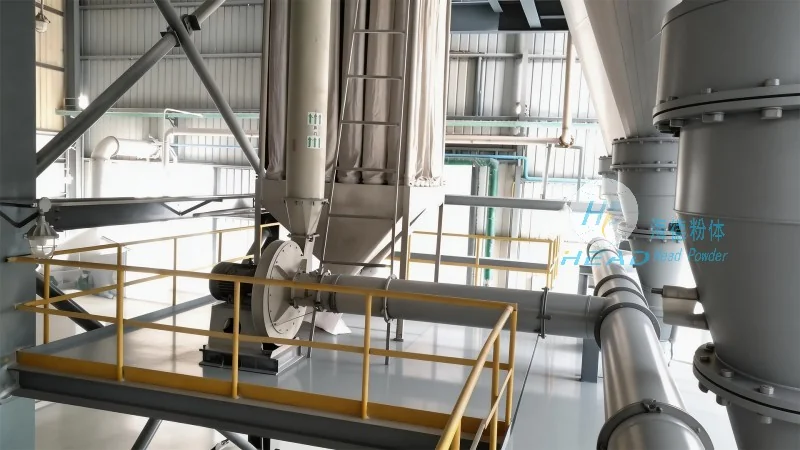
Key Features and Advantages of the Intelligent System
The intelligent pneumatic conveying system offers several advantages over traditional methods. Firstly, it provides a dust-free and hygienic environment, which is particularly important for food, pharmaceutical, and chemical industries where contamination control is critical. Secondly, the system is highly flexible, allowing for easy reconfiguration and expansion to accommodate changing production needs. Thirdly, the automation features enhance operational efficiency by reducing manual intervention and minimizing downtime. Furthermore, the system is energy-efficient, with the ability to recycle air and optimize pressure settings to reduce energy consumption. These features make the intelligent pneumatic conveying system a cost-effective and sustainable solution for bulk material handling.
Application Scenarios and Practical Benefits
The intelligent pneumatic conveying system is widely applicable across various industries, including food processing, pharmaceutical manufacturing, chemical processing, and mining. In the food industry, it is used for transporting powders like flour, sugar, and spices, ensuring product safety and quality. In pharmaceuticals, the system facilitates the transport of active ingredients and excipients, maintaining strict contamination standards. In chemical processing, it handles a range of materials from powders to granules, supporting efficient production lines. The practical benefits of the system include improved productivity, reduced labor costs, and enhanced safety, as the automated process minimizes human exposure to dust and hazardous materials. By integrating advanced technology with robust design, the intelligent pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers a reliable and efficient solution for bulk material handling, meeting the evolving demands of modern industrial operations.