

Introduction to Bin Bottom Pneumatic Conveying: Structure and Working Principle
Bin bottom pneumatic conveying systems represent a sophisticated method for transporting bulk materials from storage silos or hoppers to processing units. This technology is widely used in industries such as food processing, pharmaceuticals, and chemical manufacturing due to its efficiency and ability to handle a variety of materials. The system operates by creating a vacuum or pressure differential to move powders or granules through a pipeline network.
Core Components and Structural Design
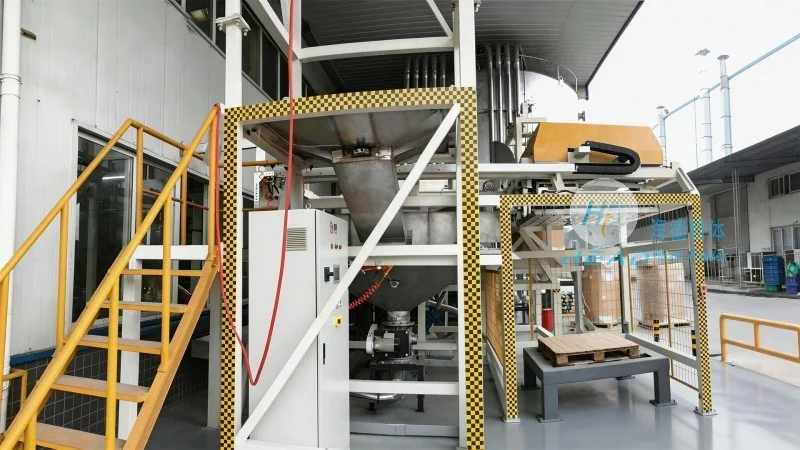
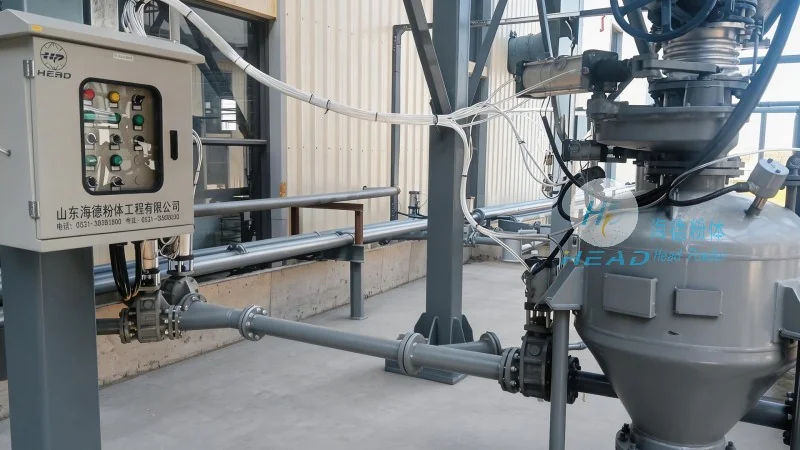
The bin bottom pneumatic conveying system consists of several key components that work in concert to ensure reliable material transport. These include the storage bin or hopper, a discharge valve (often a rotary or slide valve), a conveying line, a filter or cyclone separator, and a dust collection system. The storage bin is typically designed with a conical bottom to facilitate material flow, while the discharge valve controls the rate of material release. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is equipped with bends and elbows to navigate the system layout. The filter or cyclone separator is crucial for capturing and returning any fines back to the bin, maintaining material quality and preventing contamination. The dust collection system ensures compliance with environmental regulations by capturing and treating airborne particles.
Working Principle of the Conveying Process
The operation of a bin bottom pneumatic conveying system involves a sequence of steps that convert the stored material into a flowing stream. Initially, the discharge valve opens, allowing material to fall into the conveying line. Simultaneously, a vacuum or pressure is created within the line, which draws the material along with air or a carrier gas. The material is then transported through the pipeline to the destination point, such as a mixer or processing machine. At the receiving end, the material is separated from the air using a filter or cyclone, and the air is either vented or recirculated. This process is continuous and can be controlled to match production demands, providing flexibility in material handling.

Advantages of Bin Bottom Pneumatic Conveying
Bin bottom pneumatic conveying offers several advantages over traditional mechanical conveying methods. One of the primary benefits is its ability to handle a wide range of materials, including fine powders and abrasive substances, without causing degradation or contamination. The system is also relatively compact, requiring less floor space compared to belt or screw conveyors. Additionally, it can be integrated with existing infrastructure, making it a cost-effective solution for many applications. The enclosed nature of the system helps maintain product integrity and reduces dust emissions, which is critical in industries where hygiene and environmental compliance are paramount.
Applications in Industrial Settings
Bin bottom pneumatic conveying systems are applied in various industrial processes where bulk material handling is essential. In the food industry, they are used to transport ingredients like flour, sugar, and spices from storage bins to production lines. In pharmaceutical manufacturing, the system ensures that active pharmaceutical ingredients (APIs) are handled in a sterile and controlled environment, minimizing the risk of contamination. The chemical industry also benefits from this technology, as it can handle corrosive or hazardous materials safely and efficiently. Furthermore, the system's flexibility allows it to be adapted for different production scales, from small-scale batch processing to large-scale continuous operations.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems. With a focus on innovation and quality, the company specializes in designing and manufacturing bin bottom pneumatic conveying equipment tailored to the needs of various industries. HeadPowder's products are known for their durability, efficiency, and compliance with international standards. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing capabilities and technical expertise to deliver reliable solutions to clients worldwide. By combining years of experience with cutting-edge technology, HeadPowder aims to provide sustainable and effective material handling solutions that enhance operational efficiency and product quality.