

Operation Process and Working Principle of Barley Malt Powder Conveying System
For a comprehensive understanding of the operation process and working principle of the barley malt powder conveying system, this analysis is presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized powder handling solutions. The system is engineered to meet the unique demands of barley malt powder transportation in industrial applications.
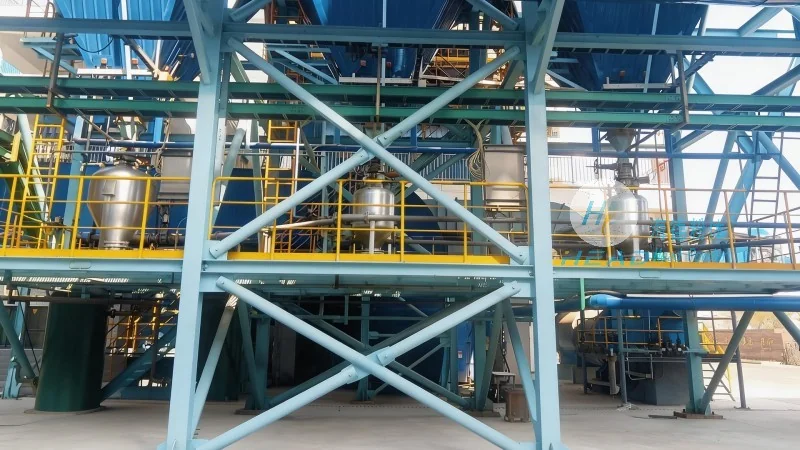
System Overview and Core Objectives
The barley malt powder conveying system is designed to efficiently transport barley malt powder from storage facilities to processing or packaging stages. Shandong HeadPowder Engineering Co., Ltd. has developed this system to address the challenges associated with handling fine, hygroscopic powders like barley malt. The system integrates advanced mechanical and pneumatic components to ensure reliable, hygienic, and efficient material transfer. Its primary objectives include maintaining product integrity, minimizing material loss, and optimizing production line throughput. The system is constructed with stainless steel components to comply with food industry hygiene standards and is tailored to handle the specific flow characteristics of barley malt powder.
Key Components and Their Functional Roles
The barley malt powder conveying system comprises several critical components, each playing a vital role in the overall operation. The main components include the material hopper, conveyor mechanism (either screw or pneumatic), control panel, and safety devices. The hopper is typically equipped with level sensors to monitor material inventory and trigger conveyor activation when the hopper reaches a predefined level. The conveyor system, which may feature a rotating screw or a pneumatic pipeline, is responsible for the actual movement of the powder. The control panel allows operators to adjust parameters such as speed, pressure, and flow rate, ensuring precise control over the conveying process. Safety devices, including overload protection and emergency stop buttons, are integrated to prevent operational hazards and protect personnel. The system's modular design enables easy integration into existing production lines and customization to meet specific production requirements.
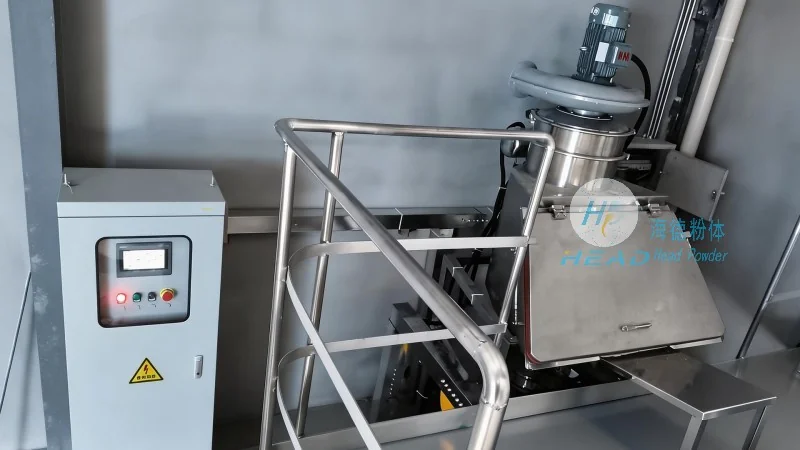
Step-by-Step Operation Process
The operation of the barley malt powder conveying system follows a systematic sequence to ensure smooth material transfer. Initially, barley malt powder is fed into the hopper from the storage silo or processing unit. The material level in the hopper is continuously monitored by sensors, which initiate the conveyor system when the hopper reaches a certain level. In a mechanical screw conveyor setup, the rotating screw pushes the powder forward along the trough, while in a pneumatic system, compressed air creates a pressure differential to propel the powder through the pipeline. The control panel manages the speed and direction of the conveyor, allowing for adjustments based on production demands. Once the powder reaches the destination point, such as a mixer or packaging machine, the system stops automatically or based on the signal from the receiving equipment. The entire process is designed to minimize material loss, prevent clogging, and maintain consistent flow rates, which are crucial for maintaining product quality and production efficiency. The system also incorporates features like pulse-jetting to clear blockages and maintain consistent flow, ensuring reliability and performance.
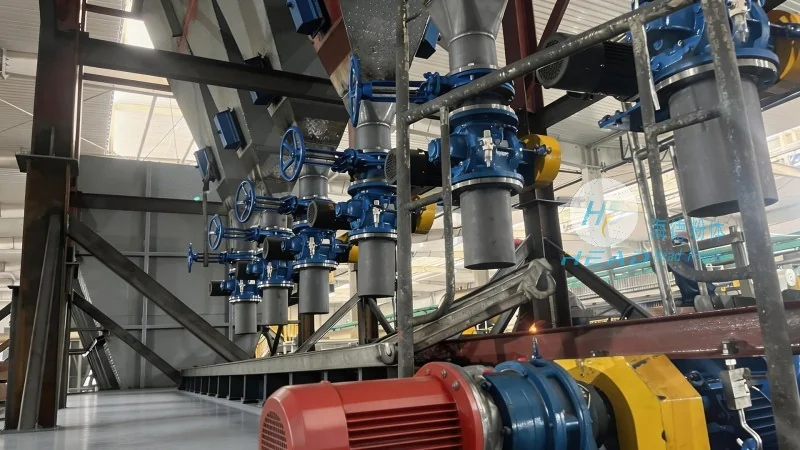
Working Principle Explained
The working principle of the barley malt powder conveying system is based on either mechanical or pneumatic transport, depending on the system design. In a mechanical screw conveyor, the rotating screw creates a self-priming action that pulls the powder into the conveyor and pushes it forward. The pitch and speed of the screw determine the conveying capacity and the pressure exerted on the material. The system operates under a closed environment to prevent dust emission and maintain air quality. In a pneumatic conveying system, the principle of fluid dynamics is applied, where compressed air is introduced into the pipeline to create a flow that carries the powder particles. The system uses either positive pressure (blowing air into the pipeline) or negative pressure (sucking air out of the pipeline) to transport the material. The pressure differential between the inlet and outlet of the pipeline determines the conveying distance and the material flow rate. The control system regulates the air pressure and flow rate to ensure stable operation and prevent system overload. The working principle also includes features such as cyclone separators and filters to separate the powder from the air stream, ensuring clean and efficient material transfer.
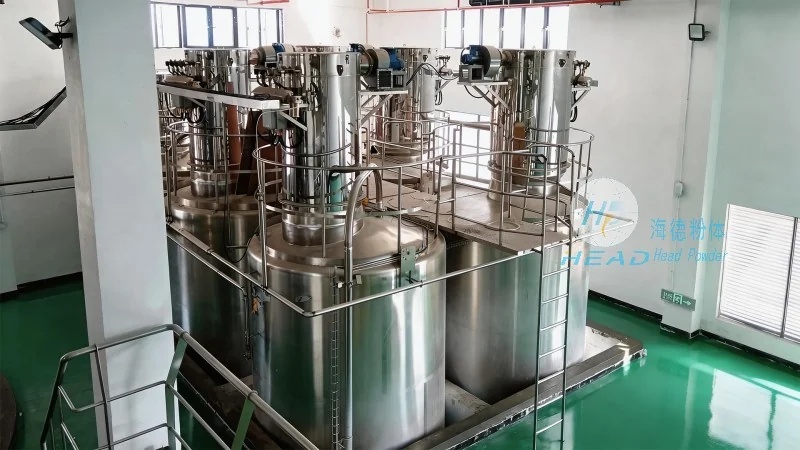
Advantages and Practical Applications
The barley malt powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it suitable for various industrial applications. The system is designed to handle the delicate nature of barley malt powder, preventing breakage or agglomeration during transport. The stainless steel construction ensures hygiene compliance, which is essential in food processing industries. The system's modular design allows for easy integration into existing production lines and can be customized to meet specific production requirements. It is widely used in breweries, malt houses, and food processing facilities where the efficient and hygienic transfer of barley malt powder is critical. The system's ability to maintain consistent flow rates and minimize material loss contributes to improved production efficiency and cost savings. Additionally, the system's control panel provides real-time monitoring and data logging, enabling operators to optimize performance and troubleshoot issues quickly. The system is also designed for low maintenance, reducing downtime and operational costs.
Conclusion and Company Background
In conclusion, the barley malt powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is a sophisticated and reliable solution for the efficient handling of barley malt powder. By integrating advanced components and following a systematic operation process, the system ensures consistent material transfer, maintains product quality, and enhances production efficiency. The working principle, which may involve mechanical or pneumatic transport, is tailored to the unique characteristics of barley malt powder, ensuring optimal performance. With its robust construction, hygienic design, and user-friendly control system, this system is an essential asset for any industrial facility involved in the processing of barley malt. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored solutions to meet the evolving needs of the industry, ensuring that their systems remain at the forefront of powder handling technology. The company, with its headquarters in Shandong, China, specializes in developing customized powder handling solutions that meet the stringent requirements of the food and beverage industry.