

Principles and Application Scenarios of Pneumatic Conveying for Pharmaceutical Materials
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying solutions tailored for the pharmaceutical industry. Pneumatic conveying is a critical technology used to transport bulk materials, including powders and granules, within pharmaceutical manufacturing facilities. This method offers a hygienic, efficient, and flexible approach to material handling, which is essential for maintaining compliance with stringent regulatory standards in the pharmaceutical sector.
The Fundamental Principles of Pneumatic Conveying
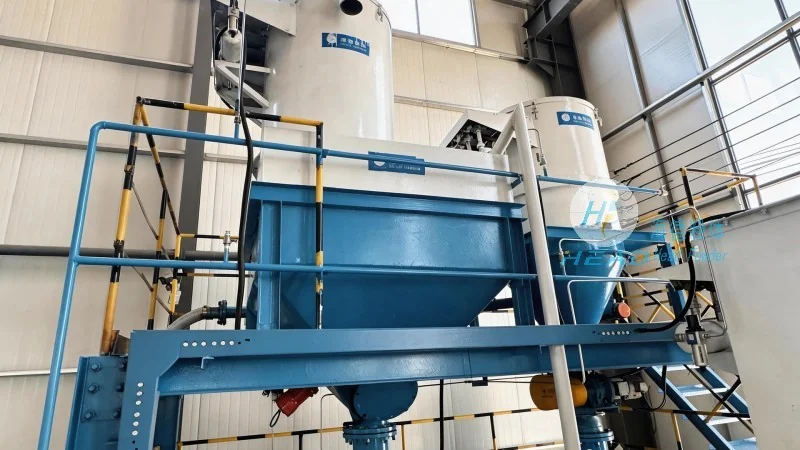
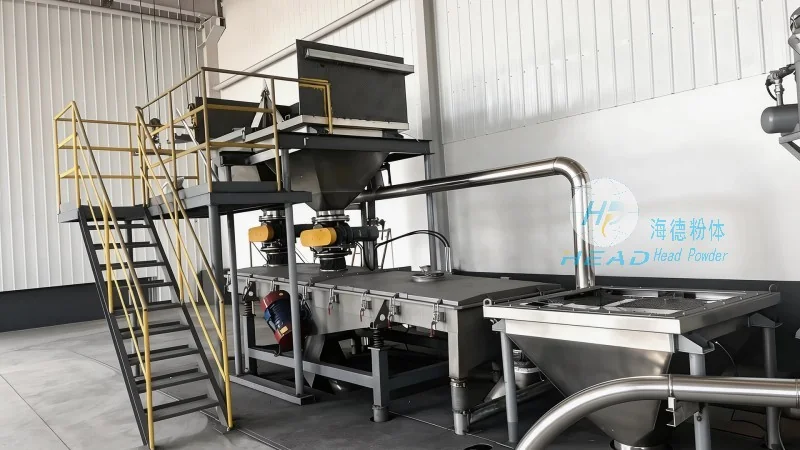
Pneumatic conveying operates by using air or other gases to move material through a pipeline system. The core principle involves creating a pressure differential between the material source and the destination. There are two primary types of pneumatic conveying systems: pressure and vacuum. Pressure systems use compressed air to push material forward, while vacuum systems employ a vacuum to pull material into the system. For pharmaceutical applications, pressure systems are often preferred due to their ability to maintain positive pressure, which helps prevent contamination from external sources. The system typically consists of a hopper, a conveyor line, and a receiver. The material is fed into the hopper, and the air is introduced to create a flow that transports the material through the pipeline to the desired location.
Key Advantages of Pneumatic Conveying in Pharmaceutical Settings
Implementing pneumatic conveying in pharmaceutical manufacturing offers several advantages. Firstly, it provides a highly hygienic environment, as the material is enclosed within a sealed system, minimizing the risk of contamination from dust, airborne particles, or external contaminants. This is crucial for maintaining product quality and ensuring compliance with Good Manufacturing Practices (GMP). Secondly, pneumatic conveying systems are highly flexible and can be easily integrated into existing production lines. They can handle a wide range of materials, from fine powders to larger granules, and can be adapted to different processing requirements. Additionally, these systems are energy-efficient compared to traditional methods like belt conveyors or bucket elevators, reducing operational costs and environmental impact. The ability to control the flow rate and pressure allows for precise material handling, which is essential for maintaining consistent product quality and reducing waste.
Common Application Scenarios in Pharmaceutical Manufacturing
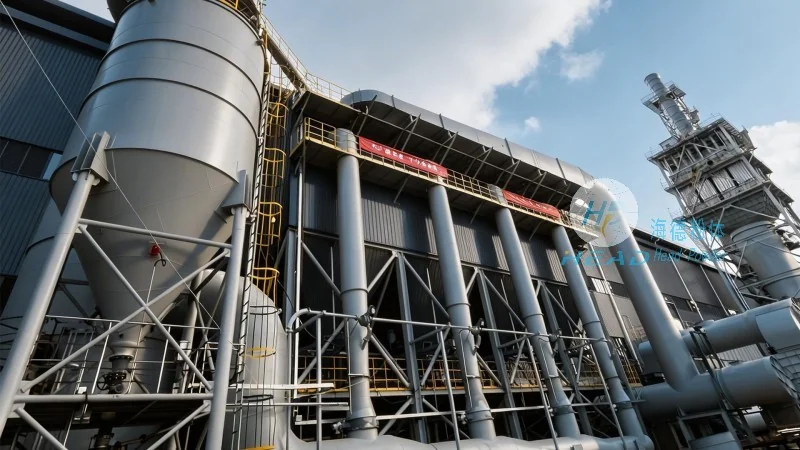
Pneumatic conveying is widely used in various stages of pharmaceutical production. One common application is in the transfer of raw materials from storage silos to processing equipment. This ensures that raw materials are delivered to the production line in a controlled manner, reducing the risk of cross-contamination and improving operational efficiency. Another key scenario is the handling of finished products, such as tablets or capsules, from packaging lines to storage areas. Pneumatic conveying can efficiently move these products through the packaging and quality control stages, ensuring that they are handled gently and hygienically. Furthermore, in the context of bulk material storage, pneumatic conveying systems can be used to transfer materials between different storage silos or to and from processing equipment, optimizing inventory management and reducing downtime. The versatility of pneumatic conveying makes it suitable for a wide range of pharmaceutical processes, including powder blending, granulation, and packaging.
Customized Solutions by HeadPowder Engineering
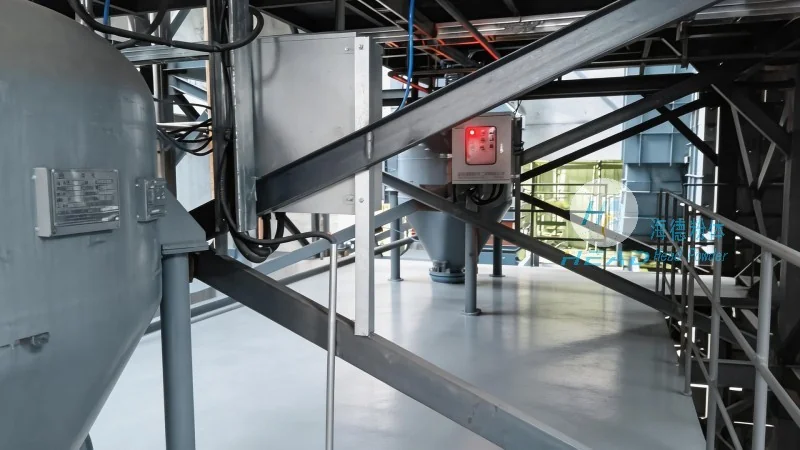
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers customized pneumatic conveying solutions tailored to the specific needs of pharmaceutical manufacturers. The company understands the unique challenges faced by the pharmaceutical industry, such as maintaining high standards of hygiene, ensuring product integrity, and adhering to regulatory requirements. By leveraging advanced engineering and manufacturing capabilities, HeadPowder provides systems that are designed to meet these demands. The company’s solutions include a range of components, such as high-quality hoppers, conveyor lines, and receivers, all constructed from materials that are compatible with pharmaceutical applications, such as stainless steel. These components are designed to be easy to clean and maintain, ensuring that the system remains in compliance with GMP standards. Additionally, HeadPowder offers comprehensive support services, including system design, installation, and maintenance, to ensure that clients can operate their pneumatic conveying systems efficiently and reliably. The company’s commitment to quality and customer satisfaction has made it a trusted partner for pharmaceutical manufacturers seeking reliable material handling solutions.