

Principle and Application Scenarios of Positive Pressure Dilute Phase Material Conveying Systems
Positive pressure dilute phase material conveying systems represent a sophisticated approach to transporting bulk materials over long distances with efficiency and reliability. This technology operates by pressurizing the conveying line, ensuring that the material is suspended in a gas stream, which allows for smooth and continuous movement. The core principle involves using a positive pressure system where the entire pipeline is maintained at a pressure higher than the ambient air pressure, preventing air from entering and ensuring the material remains in a fluidized state. This method is particularly effective for handling fine powders and granular materials that are prone to clogging or segregation in traditional conveying methods.
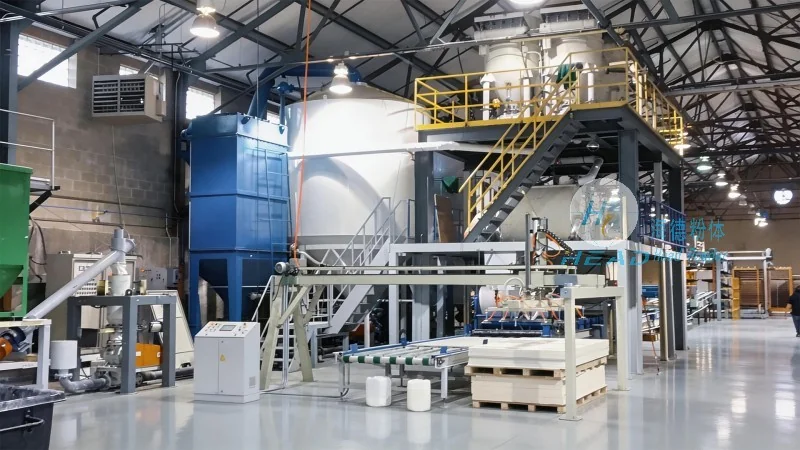
How the System Works: A Technical Overview
The operation of a positive pressure dilute phase conveyor begins with the material being fed into the inlet of the system. A blower or compressor generates the necessary pressure, which then propels the material through the pipeline. The material is typically suspended in a carrier gas, such as air, which is introduced at a controlled rate to maintain the material in a dilute phase. This phase ensures that the particles are well-separated and do not settle out, preventing blockages and ensuring consistent flow. The system includes components like feeders, pressure vessels, and control valves that work in tandem to regulate the flow rate and pressure, optimizing the conveying process for different material types and distances.
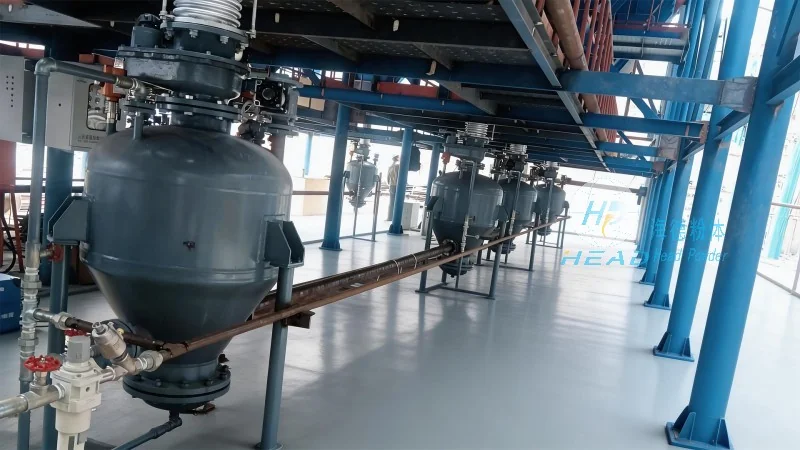
Key Advantages and Application Scenarios
Positive pressure dilute phase conveying offers several advantages over other material handling methods. It is highly efficient for long-distance transport, capable of moving materials over several kilometers with minimal energy loss. The system is also gentle on the material, reducing particle degradation and preserving product quality, which is crucial for sensitive materials like pharmaceuticals or food products. Additionally, it can handle a wide range of material sizes and densities, from fine powders to small granules, making it versatile for various industries. Common applications include the transportation of cement, coal, flour, and other bulk materials in manufacturing, mining, and construction sectors. The ability to operate in a closed system also minimizes dust emissions, enhancing safety and environmental compliance.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of advanced material handling solutions. With a focus on innovation and customer-centric design, the company specializes in developing and manufacturing positive pressure dilute phase conveying systems tailored to the needs of various industries. Headpowder's expertise lies in integrating cutting-edge technology with practical applications, ensuring that their systems meet the highest standards of efficiency, reliability, and safety. The company's facilities are located in Shandong, China, where they leverage local manufacturing capabilities to deliver high-quality products to global markets. By combining technical excellence with comprehensive support, headpowder aims to be a trusted partner for businesses seeking reliable material transport solutions.