

Principle and Working Scene Characteristics of Negative Pressure Vacuum Powder Conveying Lines
HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced negative pressure vacuum powder conveying systems. These systems are engineered to efficiently transport bulk powders over long distances with precision and reliability. The following article delves into the fundamental principles behind these systems and highlights key working scene characteristics that make them indispensable in various industrial applications.
The Core Principle of Negative Pressure Vacuum Conveying
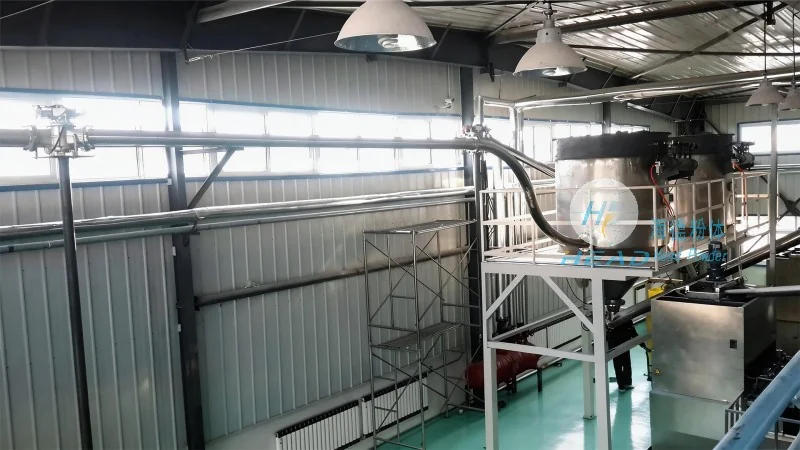
The negative pressure vacuum powder conveying line operates on the principle of creating a partial vacuum within the conveying pipeline. This vacuum is generated by a vacuum pump, which draws air and the powder mixture from the source container into the system. As the air and powder are drawn into the pipeline, they are transported to the destination point under the pressure differential created by the vacuum. The system typically includes a hopper for material storage, a vacuum pump to maintain the vacuum, and a filter to separate the powder from the air before releasing the air back to the atmosphere. This process ensures that the powder is conveyed without the need for mechanical components like augers or belts that might cause contamination or wear.
Key Working Scene Characteristics
One of the primary advantages of negative pressure vacuum conveying is its ability to handle powders in a clean and controlled manner. The system is particularly suitable for applications where contamination control is critical, such as in pharmaceutical, food, and chemical industries. The enclosed pipeline design prevents dust from escaping into the environment, reducing health hazards and maintaining product purity. Additionally, the system can handle a wide range of powder types, including fine powders, granules, and even sticky or cohesive materials, by adjusting the vacuum pressure and conveying speed to ensure smooth flow.
Applications in Diverse Industrial Settings
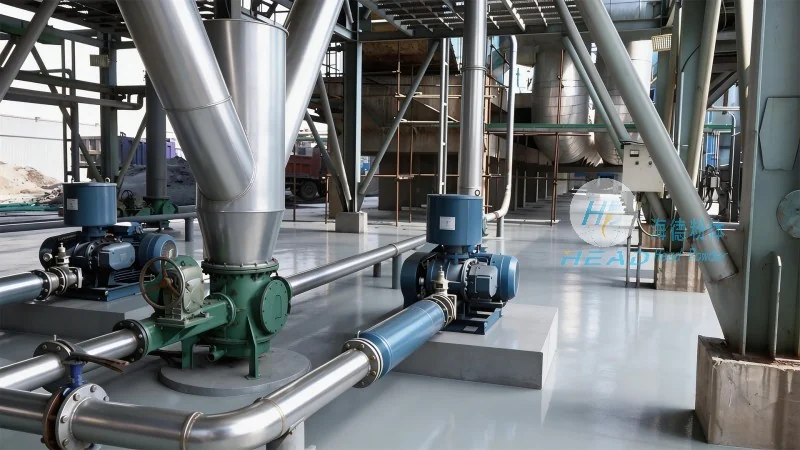
HeadPowder's negative pressure vacuum powder conveying lines are deployed in various industrial settings across China, particularly in Shandong province. These systems are commonly used in the chemical industry for transporting raw materials like powders and granules to reactors and processing units. In the food industry, they are employed to handle ingredients such as flour, sugar, and spices, ensuring hygienic and efficient transfer from storage to production lines. The pharmaceutical sector also benefits from these systems, as they provide a sterile and contamination-free method for moving active pharmaceutical ingredients (APIs) and excipients. Furthermore, the system's flexibility allows it to be integrated into existing production lines, minimizing downtime and enhancing overall operational efficiency.
Advantages in Material Handling
Compared to other conveying methods like pneumatic positive pressure systems or mechanical conveyors, negative pressure vacuum conveying offers several distinct advantages. The system is gentler on the material, reducing particle breakage and preserving the physical properties of the powder. This is crucial for products that are sensitive to handling, such as delicate pharmaceutical powders or high-value food ingredients. Additionally, the vacuum system can handle powders with higher moisture content or those that are prone to caking, as the low pressure environment prevents the formation of clumps. The enclosed design also minimizes the risk of dust explosions, making it safer for operations involving flammable or explosive powders.
Customization and Scalability
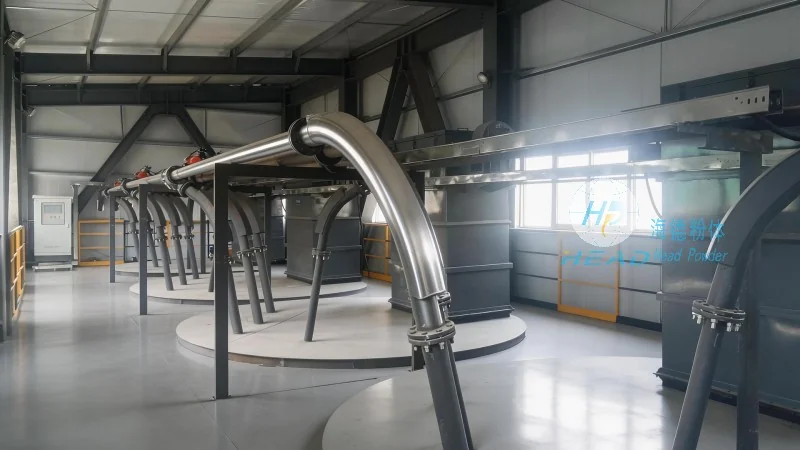
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers customized solutions tailored to the specific needs of each client. The company's engineers work closely with customers to design systems that meet their unique requirements, including the type of powder, conveying distance, and production capacity. The systems can be scaled from small laboratory-scale units to large industrial plants, ensuring that they can accommodate the growing needs of businesses. Furthermore, the modular design of the systems allows for easy expansion or modification as production processes evolve. This flexibility makes negative pressure vacuum conveying a long-term investment that can adapt to changing industrial demands.
Conclusion and Service Commitment
In conclusion, negative pressure vacuum powder conveying lines represent a sophisticated and efficient solution for bulk powder handling. The principles of creating a vacuum to transport materials offer a clean, reliable, and versatile method that is widely applicable across various industries. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is committed to providing high-quality, customized systems that enhance operational efficiency and product quality. By leveraging advanced technology and expert engineering, the company ensures that its clients receive solutions that meet the highest standards of performance and safety.