

Working Principle and Features of Automatic Quantitative Powder Material Pneumatic Conveying System
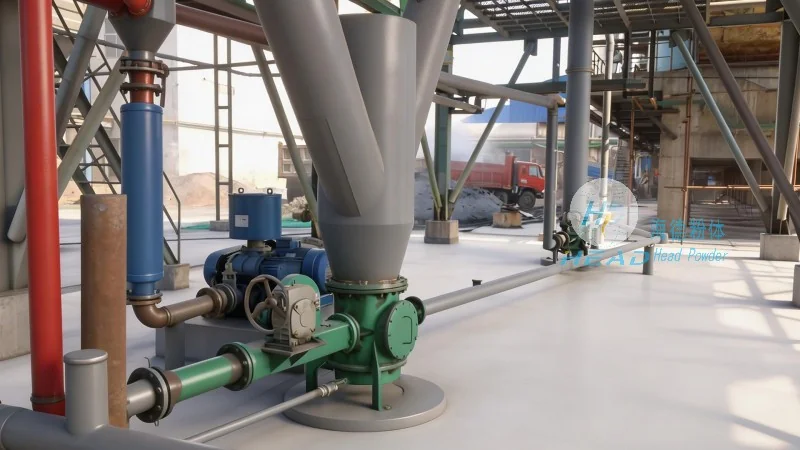
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems for handling bulk powders. The automatic quantitative powder material pneumatic conveying system is a sophisticated solution that integrates precision measurement and efficient material transport, catering to industries requiring accurate and reliable powder handling. This system is engineered to meet the demands of modern manufacturing processes where consistency and efficiency are paramount.
Company Overview
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing high-quality pneumatic conveying solutions. With its headquarters in Shandong, China, the company leverages years of experience and technical expertise to develop systems that enhance operational efficiency and product quality. The company's commitment to innovation and customer satisfaction has positioned it as a trusted partner in the powder handling industry.
Working Principle of the System
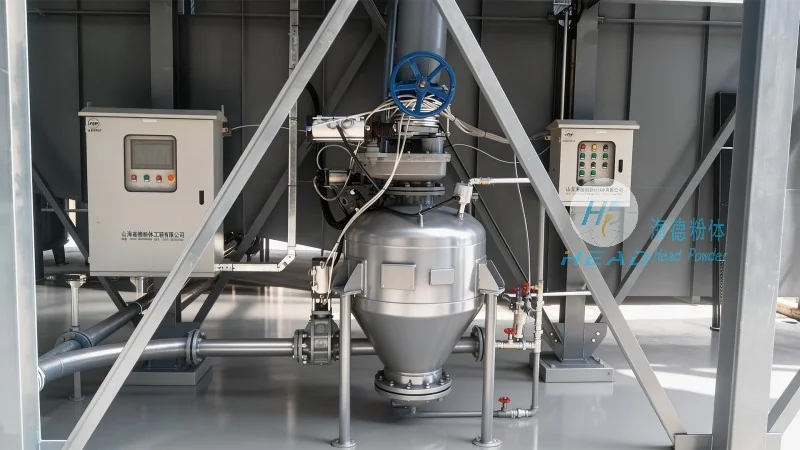
The automatic quantitative powder material pneumatic conveying system operates on the principle of pneumatic transport, where bulk powders are conveyed through a pipeline using a carrier gas, typically air. The system incorporates advanced measurement technology to ensure precise dosing of the material. The process begins with the material being fed into a hopper, where it is then transferred to a dosing unit. The dosing unit, equipped with a high-precision sensor, measures the exact quantity of powder to be conveyed. This measured material is then introduced into the conveying pipeline, where it is mixed with the carrier gas and transported to the destination point. The system maintains consistent flow rates and pressure levels to ensure reliable and uniform material transport. The control system continuously monitors the process parameters, adjusting the gas flow and dosing rate as needed to maintain optimal performance.
Key Features of the System
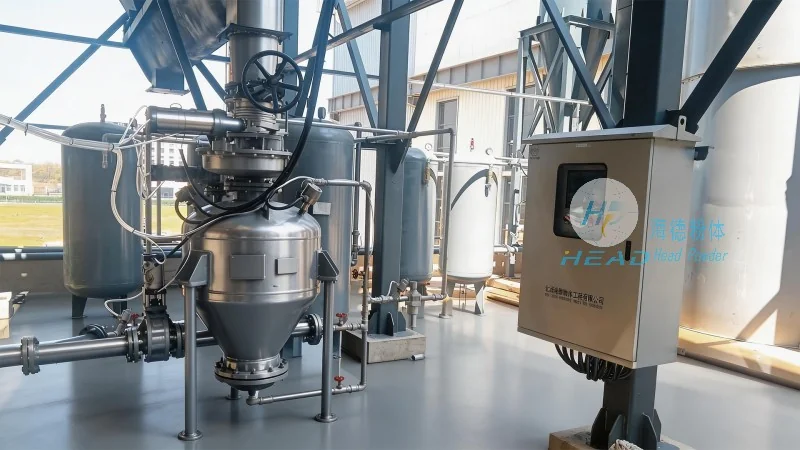
The automatic quantitative powder material pneumatic conveying system offers several distinct features that set it apart from conventional conveying methods. Firstly, the system provides high accuracy in material dosing, with the ability to achieve precise measurement and control of powder quantities. This is crucial for applications where exact material amounts are required, such as in pharmaceutical manufacturing, food processing, and chemical production. Secondly, the system is designed for efficient and low-maintenance operation. The use of pneumatic transport reduces the need for mechanical components, minimizing wear and tear and extending the system's lifespan. Additionally, the system is equipped with advanced safety features, including pressure relief valves and overcurrent protection, ensuring safe and reliable operation. The modular design of the system allows for easy integration into existing production lines and facilitates future expansion or upgrades. Another notable feature is the system's ability to handle a wide range of powder types, from fine powders to bulk materials, with minimal adjustments to the conveying parameters. This versatility makes the system suitable for diverse industrial applications.
Benefits and Applications
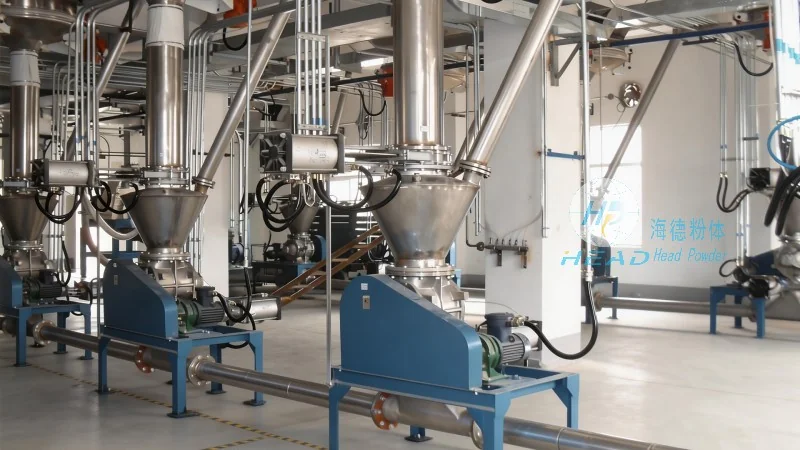
The implementation of the automatic quantitative powder material pneumatic conveying system brings numerous benefits to industrial operations. The primary advantage is the improved accuracy and consistency in material handling, which directly impacts product quality and reduces waste. By eliminating manual measurement errors, the system ensures that each batch of material meets the required specifications. Additionally, the system enhances operational efficiency by automating the material transport process, reducing labor costs and increasing production throughput. The low maintenance requirements of the system contribute to lower operational costs and increased uptime. The system is particularly beneficial in industries where powder handling is critical, such as pharmaceuticals, food and beverage, chemicals, and plastics. In pharmaceutical manufacturing, for example, the system ensures that active ingredients are accurately dosed, meeting stringent regulatory requirements. In the food industry, the system maintains hygiene standards while ensuring precise ingredient measurement. The chemical industry benefits from the system's ability to handle corrosive or abrasive powders without damage to the equipment. Overall, the automatic quantitative powder material pneumatic conveying system is a versatile and reliable solution that enhances productivity and product quality across various sectors.