

Working Principle and Characteristics of Pneumatic Conveying for White Bean Flakes Material
For those in the food processing industry, particularly those handling white bean flakes, understanding the efficiency and reliability of material handling systems is crucial. Pneumatic conveying, a technology widely used for transporting bulk materials like white bean flakes, offers a solution that combines simplicity with effectiveness. This article delves into the working principle and key characteristics of pneumatic conveying systems specifically designed for white bean flakes, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. leverage this technology to enhance operational performance.
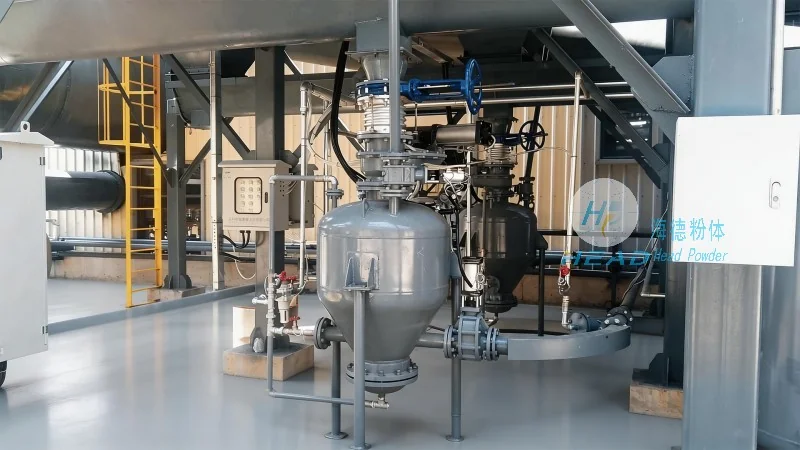
Company Background: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field of material handling solutions, is headquartered in Shandong, China. With a strong commitment to innovation and quality, the company specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of various industries, including food processing. Their expertise in white bean flakes handling has enabled them to develop systems that ensure minimal product degradation, consistent flow rates, and efficient transport from storage to processing lines.
The Working Principle of Pneumatic Conveying for White Bean Flakes
Pneumatic conveying operates on the principle of using air or gas to transport solid materials through a pipeline. In the case of white bean flakes, the system typically involves a combination of positive and negative pressure or vacuum to move the material. The process begins with the material being introduced into a hopper or feeder, where it is then drawn into the conveying line by a vacuum or pushed by a positive pressure system. The air flow, often generated by a blower or fan, carries the white bean flakes through the pipeline to the destination point, such as a silo, processing unit, or packaging line. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of product contamination.
Key Characteristics of Pneumatic Conveying Systems for White Bean Flakes
When considering pneumatic conveying for white bean flakes, several key characteristics stand out, making it an ideal choice for food processing applications:
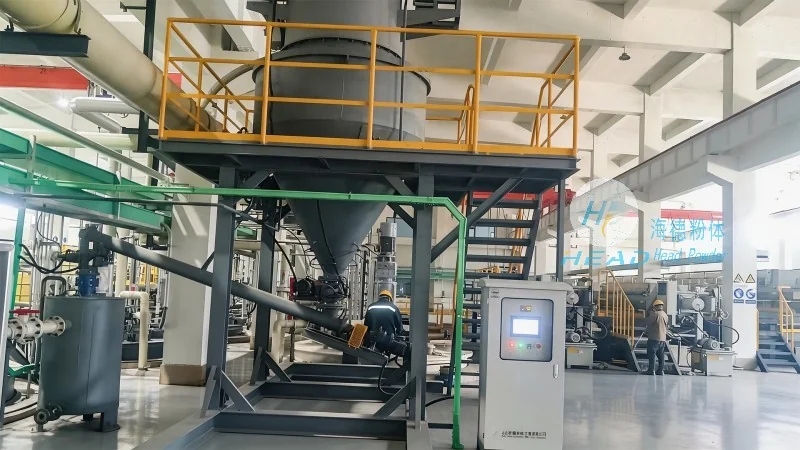
1. Hygienic and Clean Operation: Pneumatic systems are designed with smooth, easy-to-clean surfaces and minimal contact points, ensuring compliance with food safety regulations. The absence of moving parts in the conveying line reduces the risk of product contamination, which is critical for white bean flakes used in food products.
2. Low Product Damage: The gentle handling of white bean flakes through the air flow minimizes breakage and bruising, preserving the quality and integrity of the product. This is particularly important for delicate food items where texture and appearance are key to consumer acceptance.
3. Flexible and Scalable: Pneumatic conveying systems can be easily scaled to accommodate varying production volumes, from small-scale operations to large industrial facilities. The modular design allows for the addition or removal of conveying lines as production needs change, providing flexibility in plant layout and expansion.
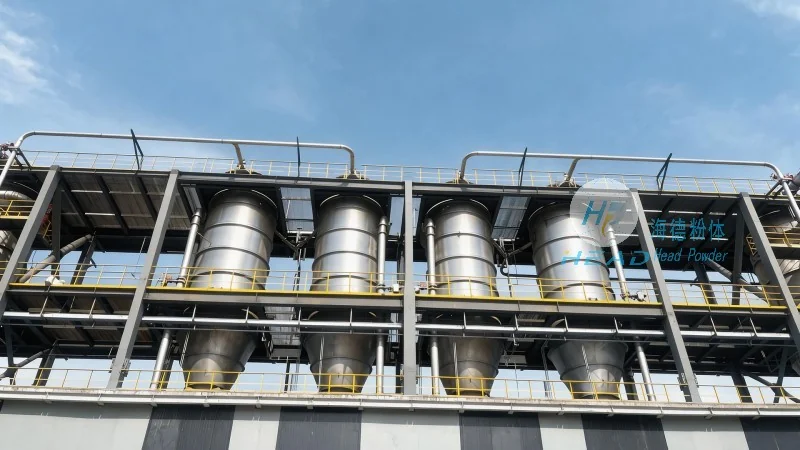
4. Energy Efficiency: Modern pneumatic systems utilize energy-efficient blowers and optimized air flow designs, reducing operational costs while maintaining high conveying rates. This efficiency is achieved through advanced control systems that adjust air pressure and flow based on the material being transported.
Benefits of Choosing HeadPowder's Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. offers customized pneumatic conveying solutions that address the specific challenges of white bean flakes handling. By integrating advanced technology with a deep understanding of food processing requirements, their systems provide consistent performance, reduced downtime, and improved overall productivity. The company's commitment to quality and customer satisfaction ensures that each system is tailored to meet the unique needs of their clients, whether it's for small-scale processing or large-scale industrial applications.
From the initial design phase to installation and ongoing maintenance, HeadPowder provides comprehensive support to ensure that their pneumatic conveying systems operate at peak efficiency. With a focus on durability, reliability, and compliance with industry standards, their solutions are built to withstand the demands of continuous operation in food processing environments.