

Working Principle and Features of Barley Material Handling System Equipment
Barley is a vital agricultural commodity utilized across multiple sectors, including brewing, animal feed production, and food processing. Efficient material handling systems are critical for optimizing the movement of barley from storage to processing facilities. This article examines the working principle and key characteristics of modern barley material handling systems, illustrating how they enhance operational efficiency and product quality.

Working Principle of Barley Material Handling Systems
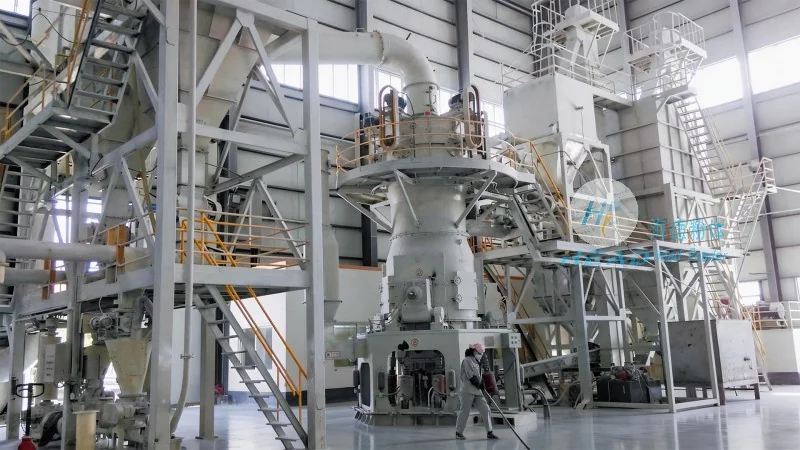
The fundamental working principle of barley material handling systems involves the continuous transfer of bulk barley from storage silos or bins to processing units. These systems typically comprise a combination of components, including conveyors, elevators, and storage bins, engineered to manage the bulk nature of barley. The process initiates with the storage of harvested barley in large, airtight silos to preserve quality and prevent spoilage. From these silos, the barley is then transported through a series of mechanical systems to reach the processing line.
Conveyor systems, such as belt conveyors or screw conveyors, are commonly employed to move barley horizontally or vertically. Belt conveyors are ideal for transporting large quantities of barley over extended distances, while screw conveyors are effective for vertical lifting and compact storage. Elevators, often equipped with buckets or buckets, are used to lift barley from lower to higher levels, ensuring a continuous flow. The entire system is controlled by a centralized control panel that monitors flow rate, pressure, and other critical parameters to maintain optimal operation.
Key Features of Barley Material Handling Equipment
Modern barley material handling equipment is designed with several key features that enhance performance and reliability. One of the most important features is the ability to handle bulk materials with minimal loss or damage. This is achieved through the use of gentle handling mechanisms, such as belt conveyors with soft surfaces or flexible augers, which prevent the barley from being crushed or broken during transport.
Another critical feature is the system's adaptability to varying barley conditions. The equipment can handle different moisture levels, grain sizes, and impurity contents without compromising efficiency. This flexibility is essential for processing barley from different regions or batches, ensuring consistent quality in the final product.
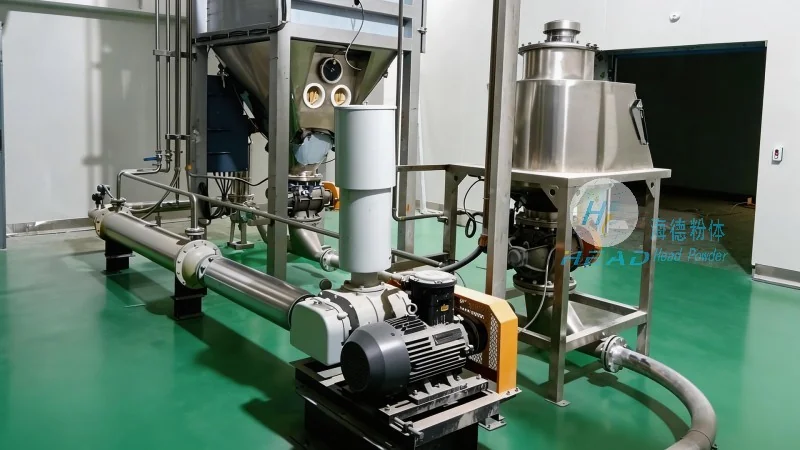
Efficiency and energy conservation are also key considerations in modern barley material handling systems. Advanced systems incorporate energy-efficient motors and variable speed drives that adjust the conveyor speed based on the load, reducing energy consumption while maintaining optimal throughput. Additionally, the use of automated controls minimizes human intervention, reducing labor costs and improving operational safety.
Reliability and Maintenance of Barley Handling Systems
Reliability is a top priority for barley material handling systems, as downtime can lead to significant losses in production and revenue. Manufacturers, such as Shandong HeadPowder Engineering Co., Ltd., focus on designing robust systems with durable components that can withstand the harsh conditions of agricultural environments. Regular maintenance is essential to ensure the longevity of the equipment, and many systems include built-in monitoring tools that alert operators to potential issues before they become major problems.
The integration of advanced materials, such as corrosion-resistant steel and wear-resistant coatings, further enhances the durability of the equipment. These features ensure that the systems can operate continuously for extended periods without requiring frequent repairs or replacements.
Application in Different Industries
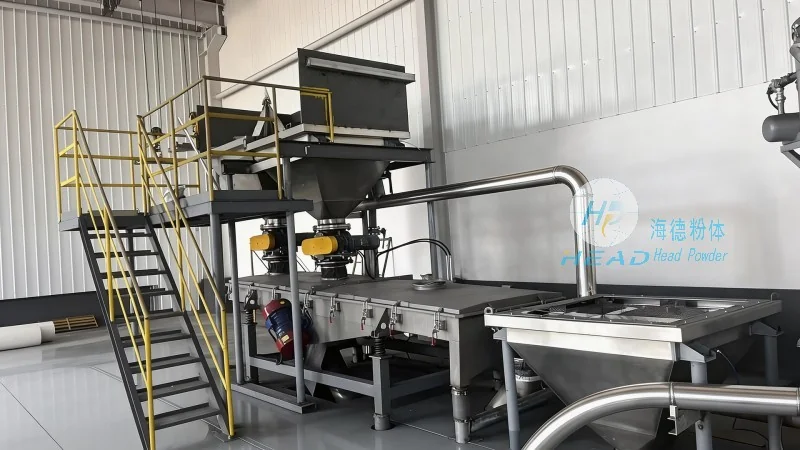
Barley material handling systems are widely utilized in various industries beyond brewing. In the animal feed industry, these systems efficiently transport barley to feed mills, where it is mixed with other ingredients to create high-quality feed. In the food processing industry, the equipment is used to move barley for milling into flour or other food products. The versatility of these systems makes them suitable for a wide range of applications, from small-scale farms to large industrial processing plants.
For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, the development of reliable and efficient barley handling systems is a core part of their commitment to supporting the agricultural and processing industries. By providing high-quality equipment, they help their clients optimize their operations and improve overall productivity.