

Working Principle and Characteristics of Calcite Material Handling
Calcite, a widely used calcium carbonate mineral, is integral to industries including construction, chemicals, and pharmaceuticals. Efficient material handling of calcite is essential for optimizing production workflows and maintaining consistent product quality. This article examines the working principle and key features of calcite material handling systems, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider based in Shandong, China.
Understanding the Working Principle of Calcite Material Handling
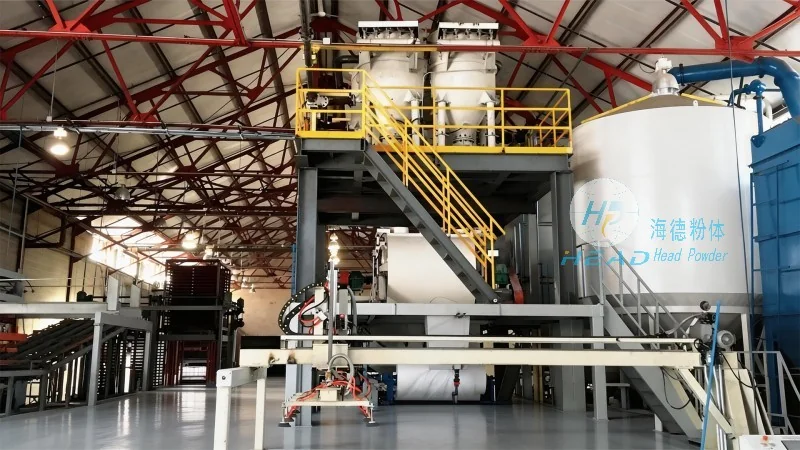
The working principle of calcite material handling revolves around specialized equipment designed to transport bulk calcite from one location to another. Common systems include belt conveyors, bucket elevators, and screw conveyors, each optimized for specific operational needs. Belt conveyors utilize a continuous loop of conveyor belt supported by rollers and pulleys to move calcite horizontally or at a slight incline, ensuring smooth and continuous flow. Bucket elevators employ rotating buckets attached to a vertical or inclined chain to lift calcite vertically, making them ideal for vertical transport in processing plants. Screw conveyors use a rotating screw within a tube to push calcite forward, suitable for horizontal or gentle incline transport. These systems integrate with feeding mechanisms like hoppers and feeders to regulate flow rates and prevent blockages, ensuring efficient and reliable calcite movement.
Key Characteristics of Calcite Material Handling Systems
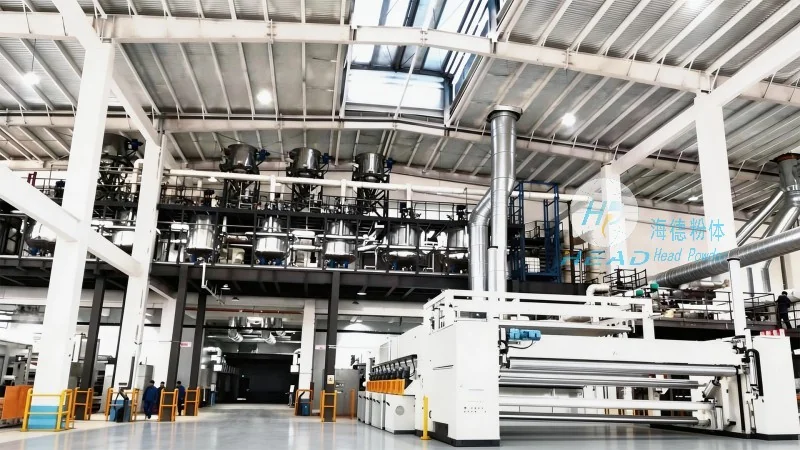
Calcite material handling systems exhibit several defining characteristics that enhance industrial applications. Firstly, they are engineered for high efficiency, capable of processing large volumes of calcite continuously. Robust construction and durable components withstand the abrasive nature of calcite particles, ensuring longevity. Secondly, these systems offer high reliability with minimal maintenance, reducing operational costs and downtime. Precision engineering in components such as conveyor belts and buckets, combined with high-quality materials, minimizes repairs and enhances performance. Thirdly, the systems are adaptable to diverse conditions, including varying particle sizes, moisture levels, and temperature ranges. This flexibility allows integration into diverse production lines, from raw material storage to final product packaging. Modern systems also incorporate advanced control technologies like variable speed drives and sensors, optimizing flow and detecting issues in real-time to improve efficiency.
Expertise of Shandong HeadPowder Engineering Co., Ltd. in Calcite Material Handling
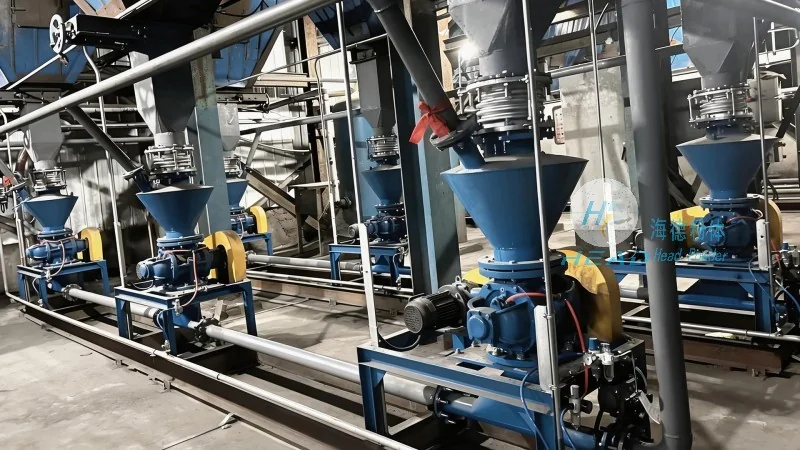
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, specializes in designing, manufacturing, and installing calcite material handling solutions. With extensive industry experience, the company understands the unique challenges of calcite handling, such as fine particle size and dust generation. HeadPowder engineers develop customized systems to address these challenges, ensuring optimal performance and safety. The company's expertise lies in tailoring solutions to meet client-specific requirements, whether for small-scale operations or large industrial plants. By leveraging advanced engineering techniques and rigorous quality control, HeadPowder delivers reliable and efficient calcite handling systems that boost productivity and reduce costs. Clients benefit from a comprehensive approach that includes consultation, system design, equipment supply, and after-sales support, ensuring seamless integration into existing infrastructure.
Conclusion
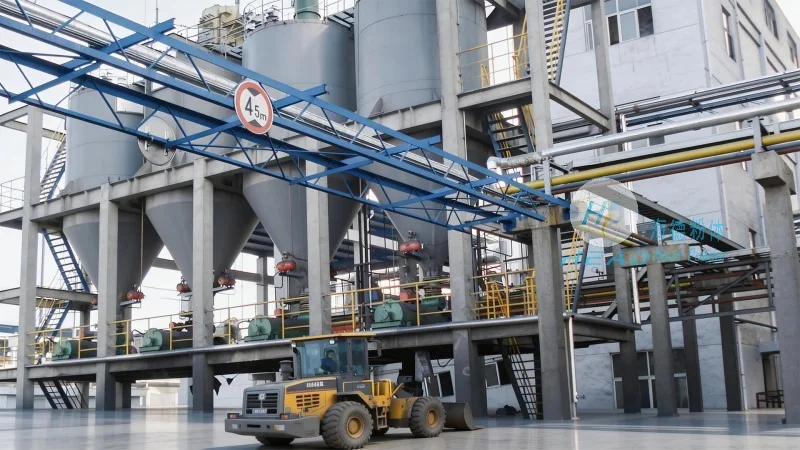
In summary, the working principle and characteristics of calcite material handling systems are critical to industrial efficiency. Specialized equipment, robust design, and advanced controls ensure high throughput, reliability, and adaptability. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing customized calcite handling solutions, leveraging its expertise to meet diverse client needs. By prioritizing quality, efficiency, and customer satisfaction, HeadPowder continues to optimize calcite handling processes globally.