

Working Principle and Features of Soda Ash (Sodium Sulphate) Pneumatic Conveying System Equipment
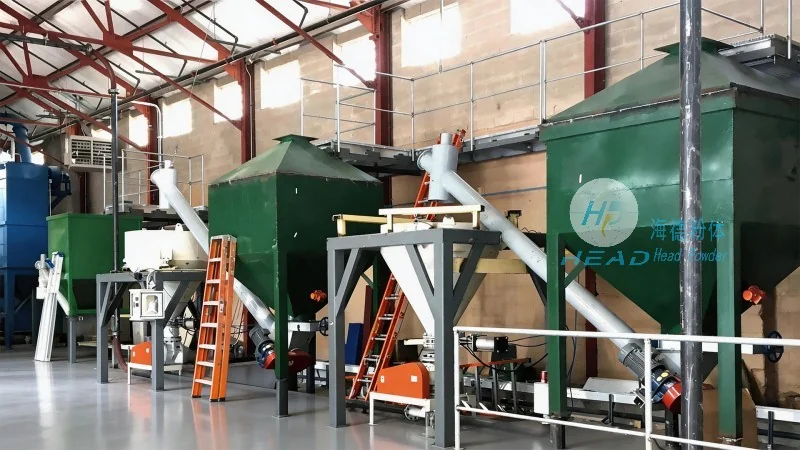
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for handling soda ash (sodium sulphate). This article provides an in-depth exploration of the working principles and key features of such systems, highlighting their efficiency and reliability in industrial applications.
Company Overview
HeadPowder, a leading enterprise based in Shandong, China, has established itself as a trusted provider of engineering solutions for material handling. With a strong commitment to quality and innovation, the company focuses on delivering customized pneumatic conveying systems that meet the specific needs of clients in various industries. The company's expertise lies in integrating advanced technology with practical engineering to ensure optimal performance and durability of the equipment.
Working Principle of Soda Ash Pneumatic Conveying Systems
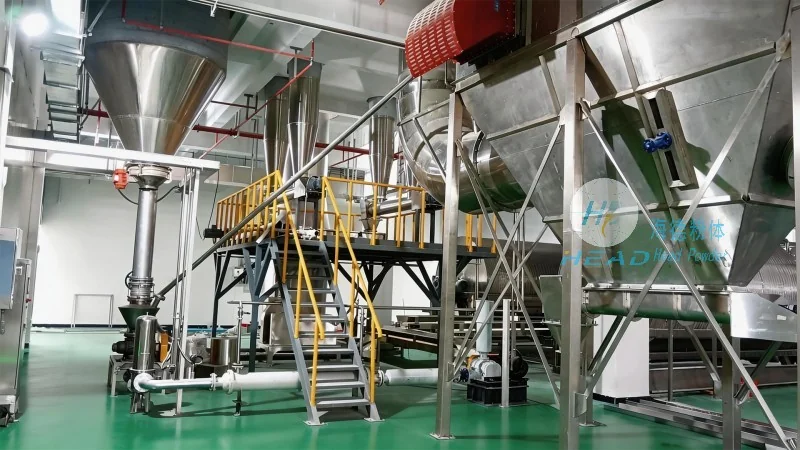
The core working principle of a soda ash pneumatic conveying system involves the use of air or gas to transport bulk materials through a pipeline network. In this system, the soda ash powder is introduced into a hopper or feeder, where it is then fed into the conveying line under controlled conditions. A blower or compressor generates the necessary airflow, which propels the material particles through the pipeline. The system typically operates under positive pressure, ensuring that the material is transported efficiently without the need for mechanical components like belts or buckets. The air velocity is carefully managed to maintain a stable flow of the powder, preventing blockages and ensuring consistent delivery to the destination point. The entire process is automated, with sensors and control systems monitoring the flow rate, pressure, and other critical parameters to maintain optimal performance.
Key Features of the Pneumatic Conveying System
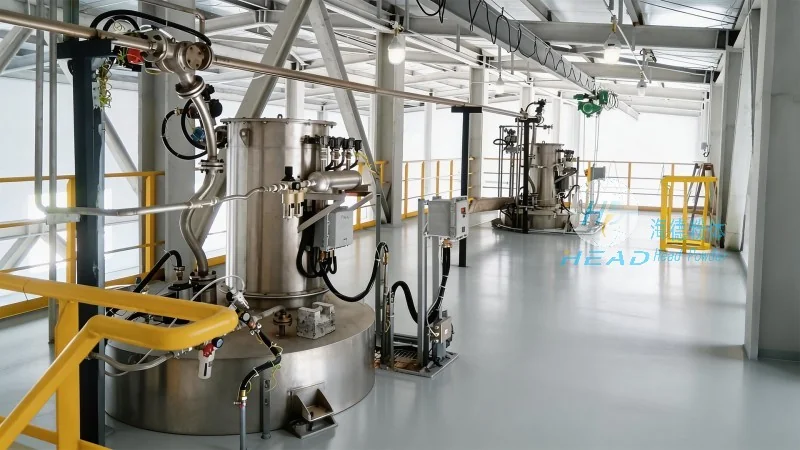
HeadPowder's soda ash pneumatic conveying systems are characterized by several key features that enhance their performance and reliability. Firstly, the system is designed for high efficiency, with minimal energy consumption compared to traditional mechanical conveying methods. The use of air as the conveying medium reduces wear and tear on the equipment, leading to lower maintenance costs and longer service life. Secondly, the system offers flexibility in terms of layout and installation, as the pipeline can be configured to follow the existing plant layout or be customized to suit new construction projects. This adaptability allows for seamless integration into existing production lines or new facilities. Thirdly, the system provides excellent control over the material flow, with adjustable air pressure and flow rates enabling precise delivery of the soda ash to the required destination. This level of control is crucial for maintaining product quality and preventing contamination. Additionally, the system is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms, ensuring safe operation in industrial environments. The materials used in the construction of the conveying lines and components are selected for their resistance to corrosion and abrasion, making the system suitable for long-term use with soda ash, which can be abrasive and corrosive in nature.
Advantages in Industrial Applications
The implementation of a soda ash pneumatic conveying system offers numerous advantages in industrial settings. By eliminating the need for manual handling or mechanical conveyors, the system reduces labor costs and improves workplace safety. The automated operation also minimizes the risk of material spillage and contamination, which is critical for maintaining product quality in the soda ash industry. Furthermore, the system's ability to transport materials over long distances without the need for intermediate storage or handling points enhances overall operational efficiency. This leads to streamlined production processes and reduced downtime, contributing to increased productivity and profitability for the end-user. The reliability of the system, with its low maintenance requirements and long service life, provides a stable and cost-effective solution for material handling needs.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s soda ash pneumatic conveying systems represent a sophisticated and efficient solution for the transportation of bulk materials in industrial applications. By understanding the working principles and leveraging the key features of these systems, industries can achieve improved operational efficiency, reduced costs, and enhanced product quality. The company's commitment to quality and innovation ensures that clients receive tailored solutions that meet their specific requirements, making HeadPowder a preferred choice for pneumatic conveying systems in the soda ash sector.